





最新发布第11页
排序
Bypassing a FANUC Linear Scale: Full to Semi Closed-Loop Conversion with 1815#1, 2024, 2084/2085 and 2185
How to temporarily bypass a FANUC linear scale and switch from full to semi closed-loop: 1815#1/#5, 2024, 2084/2085, 2185, 1821, 1850, 1851/1852, 2003#5 and 2019#7. Marks the dispu...

 前天
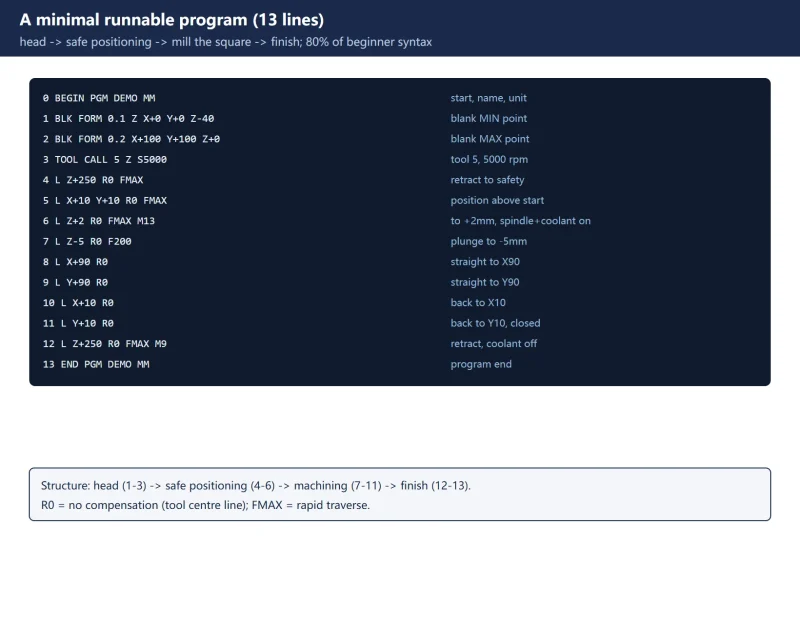
HEIDENHAIN TNC Conversational Programming for Beginners: One Minimal Program
HEIDENHAIN Klartext is conversational programming - the screen asks, you answer, no G-code memorising. Using a 13-line minimal program, this explains BEGIN PGM, BLK FORM blank, TOO...
前天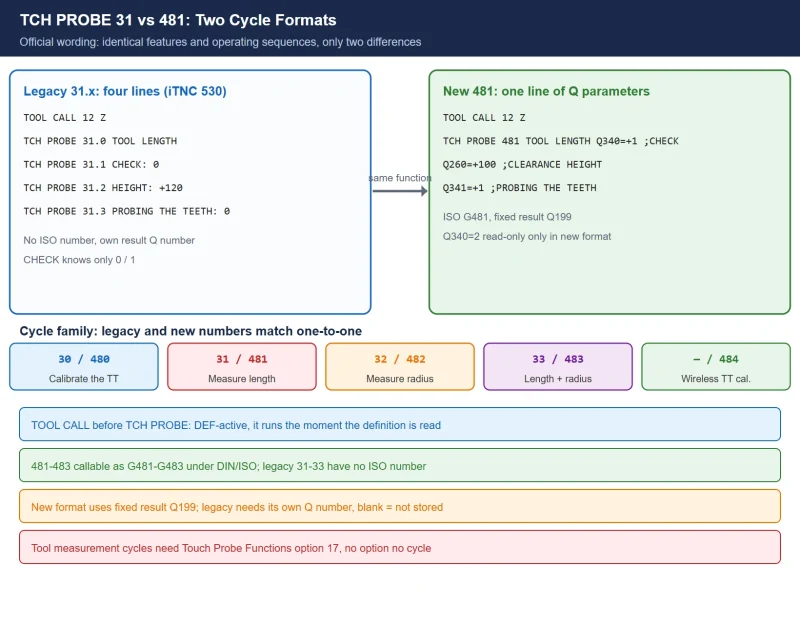
Heidenhain TCH PROBE 31 / 481 Tool Length Measurement: Parameters, TOOL.T Fields and MP vs Cfg Differences
Tool measurement with a Heidenhain TT goes wrong for three recurring reasons: the cycle format does not match the control generation, the safety-zone parameter is looked for in the...
前天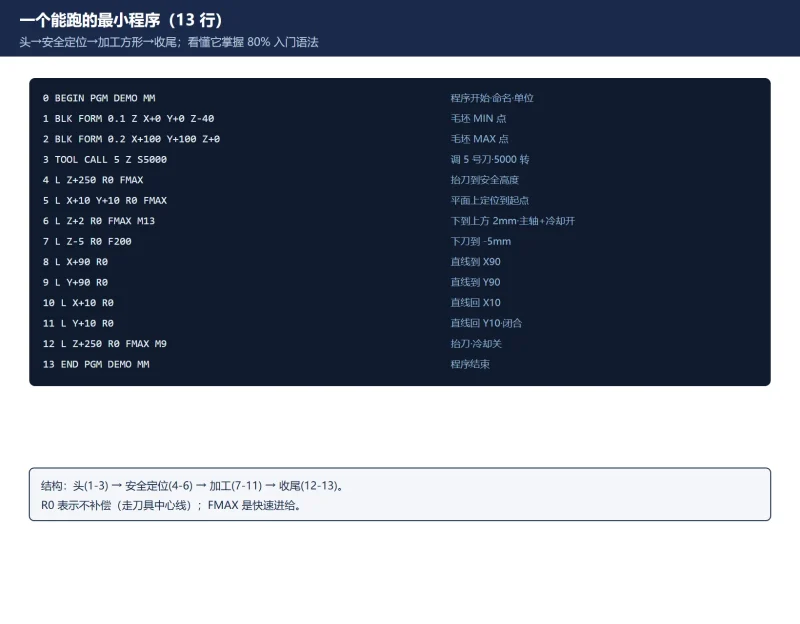
海德汉 TNC 对话式编程入门:一个最小程序看懂 BEGIN/BLK FORM/TOOL CALL/L/C/CR/APPR/循环
海德汉 Klartext 对话式编程,屏幕问一句你答一句,不用背 G 代码。本文用一个 13 行能跑的最小程序,逐行讲清 BEGIN PGM、BLK FORM 毛坯、TOOL CALL 刀具、L 直线、C/CR 圆弧、R0/RL/RR 补偿、...
前天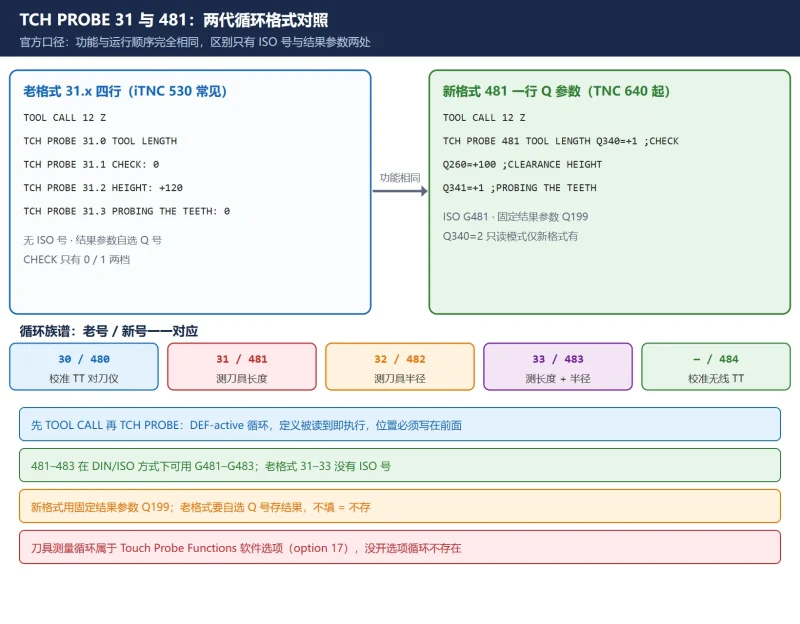
海德汉 TCH PROBE 31/481 测刀循环参数对照:iTNC530 走 MP、TNC640 走 Cfg,逐齿上限 99 与 20 的分界
对刀仪测刀测不准,根子多在循环格式选错代、安全区参数找错地方、TOOL.T 该预填的字段空着。本文按官方手册口径讲透 TCH PROBE 31 与 481 的两代格式差异、Q340 覆写/比较/只读三模式、Q260 安...
前天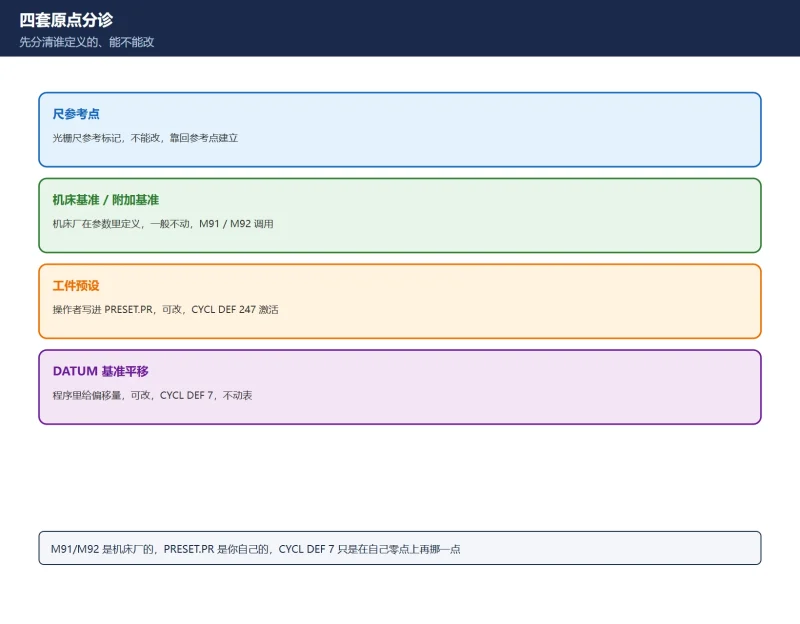
海德汉 TNC 预设(PRESET.PR)与工件零点怎么用?CYCL DEF 247 / 7 / DATUM SET 三种机制边界 + M91 / M92 + 手动与测头找正
海德汉 TNC 的预预设与工件零点怎么设?讲清 PRESET.PR 表结构、第 0 行含义、CYCL DEF 247 与 CYCL DEF 7 DATUM SHIFT 的边界、M91/M92 逐段生效与跨代定义差异,以及手动找正和 3D 测头找正的...
前天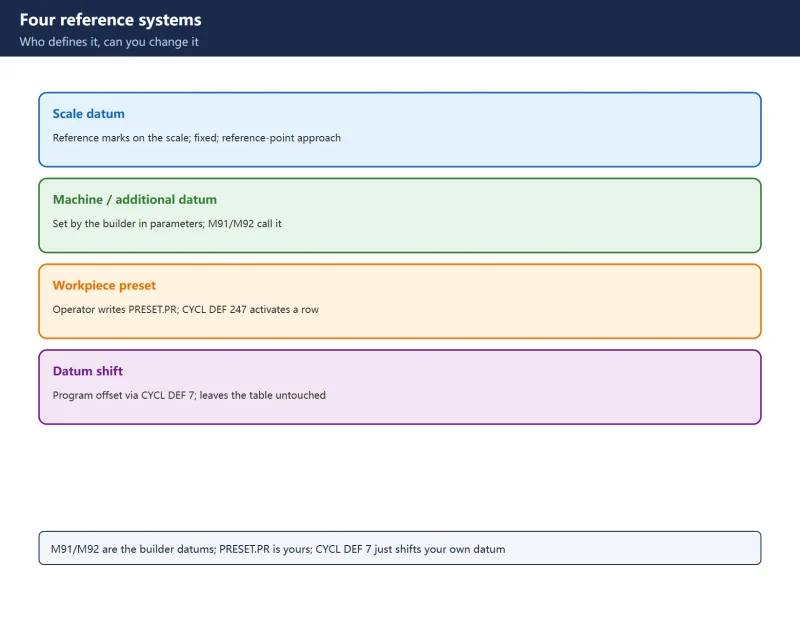
HEIDENHAIN Presets and Work Zero: PRESET.PR, CYCL DEF 247 vs CYCL DEF 7, M91/M92 and How to Set the Work Zero
How to set the work zero on a HEIDENHAIN TNC: PRESET.PR table structure, row 0, CYCL DEF 247 versus CYCL DEF 7 DATUM SHIFT, why activating a preset wipes a datum shift, M91/M92 blo...
前天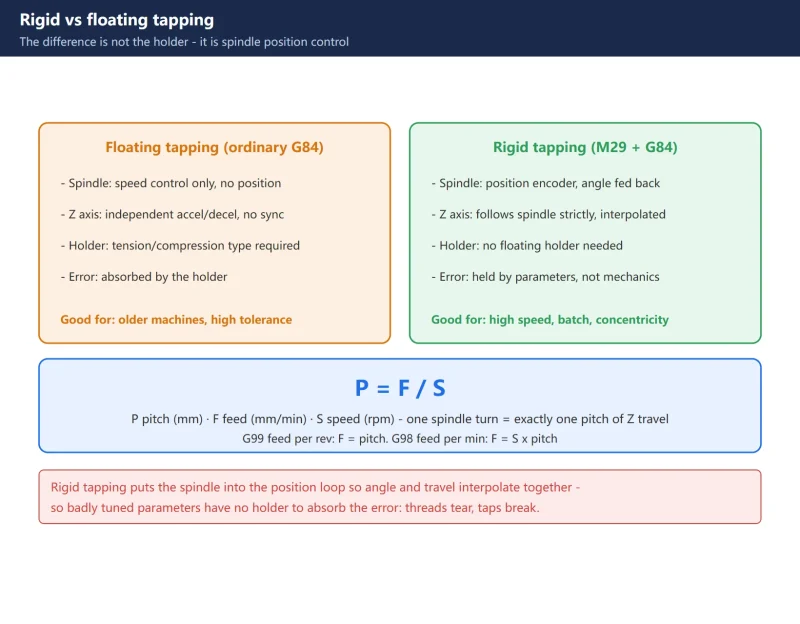
Fanuc Rigid Tapping Parameters Explained: M29/G84 Sync, the 5200–5294 Chain and SP0741 Alarm Troubleshooting (with DGN 452/453)
Bad rigid tapping is usually not the program - it is the parameters nobody explained. This guide splits the 5200-5294 group into five blocks: enable bits that decide whether you ta...
前天
FANUC M代码常见使用方法汇总
2025年新版《FANUC M代码常见使用方法汇总》高清 PDF 免费下载:13 节图解 M代码译码、结束信号、调用子程序/宏程序、缓冲类型及在线增加 M代码功能实例,适合调试/改造/维修工程师 30 分钟上手...
前天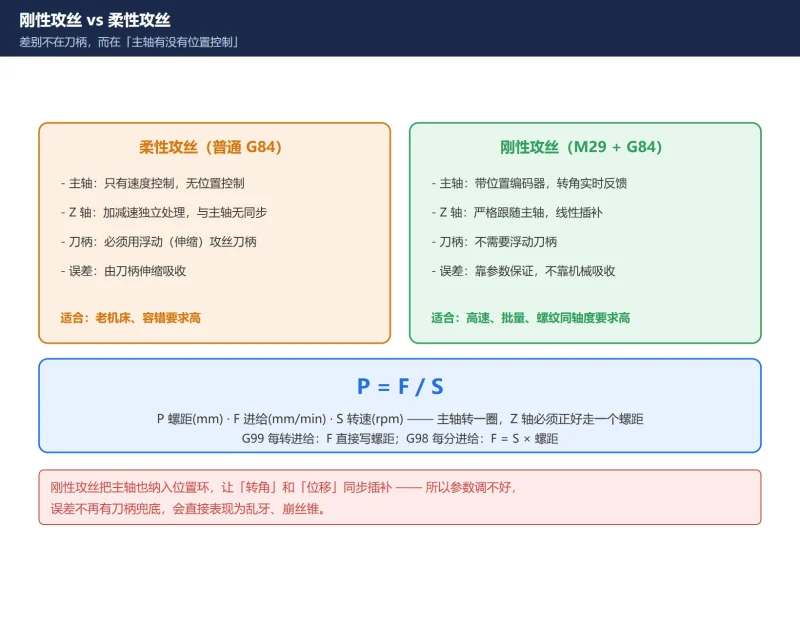
FANUC 刚性攻丝参数全解:M29/G84 同步原理 + 5200–5294 参数链 + SP0741 报警怎么排(附诊断号 452/453 读法)
刚性攻丝调不好的根子,多半不是编程而是参数。本文把 5200–5294 按五类拆开讲:开关位决定走不走刚性攻丝、齿轮比 5221–5224/5231–5234 决定比例、转速上限是 5241–5244(不是 5200)、增...
前天






扫一扫,添加我的微信










