


Declaration (read first): the meaning, units and activation conditions of every parameter are subject to the official manual for the corresponding machine model; the same function can differ across control versions and machine-builder defaults. This table is a function cross-reference and lookup entry only — it is not a parameter manual and must not be copied as a setting-value table. The parameter numbers are just the entry points for the same function; units, signs and dimensions differ, so never transfer a value from one control to another directly.
Sister article: 828D vs FANUC vs Mitsubishi Parameter Cross-Reference (Chinese); three single-brand sources: 828D Common Machine Data Quick Reference, FANUC Parameter Number Map by Range, Mitsubishi M80/M70 Servo Parameters.
29.1 Why align by function, not by number range
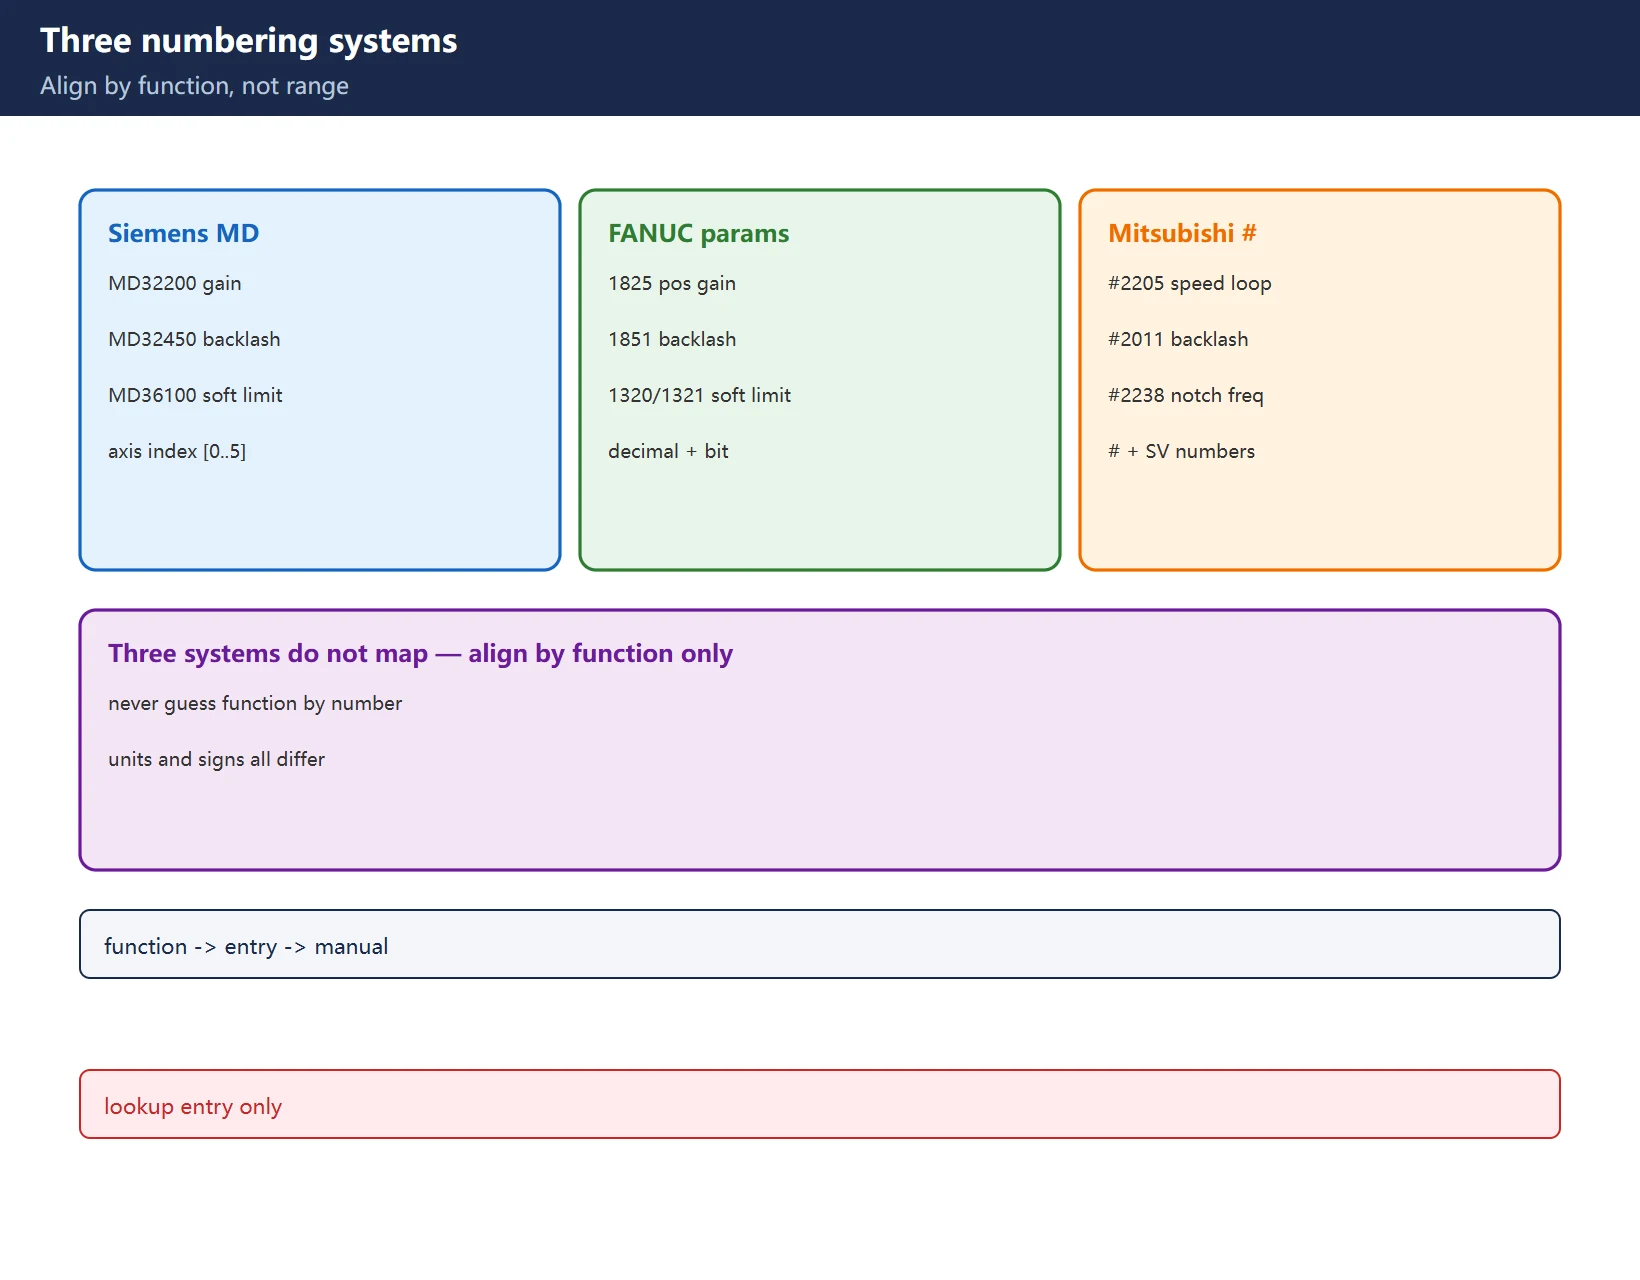
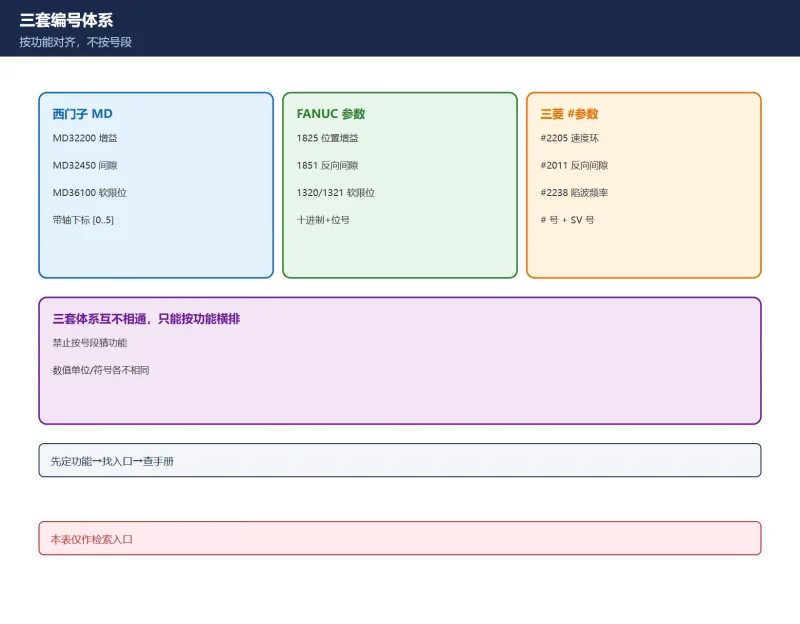
Table 1 Three numbering systems (different systems, no number-to-number mapping)
| Control | Parameter naming | Example | Unit/dimension trait |
|---|---|---|---|
| SINUMERIK 828D / 840D sl | MDxxxxx machine data, SDxxxxx setting data | MD32200 position loop gain | axis index [0..5], per channel/axis |
| FANUC 0i/3x series | decimal parameter + bit # | 1825 position loop gain, 2021 inertia ratio | units vary, often in 0.01 steps |
| Mitsubishi M80 / M800S | #xxxx parameter + SV number | #2205 speed loop gain, #2238 notch frequency | hex/decimal mixed, SV and NC numbers coexist |
The only correct workflow: decide what function you are adjusting (e.g. backlash), find that control’s entry in the matching column, then confirm meaning and units in that machine’s manual. Never guess a function from a number range — the three systems partition numbers on completely different logic.
29.2 Axis and motion: soft limits / backlash / acceleration / rapid speed
Axis parameters are the most-used group in a cross-reference. This table lines up the four common entries (including 840D sl).
Table 2 Axis and motion parameter cross-reference
| Function | SINUMERIK 828D/840D sl | FANUC | Mitsubishi M80 | Notes |
|---|---|---|---|---|
| Backlash compensation | MD32450 BACKLASH | 1851 (rapid: 1852) | #2011 (G00) / #2012 (G01, unit 0.5 um) | Units differ: Siemens mm, Mitsubishi 0.5 um — do not copy the number |
| Positive soft limit | MD36110 POS_LIMIT_PLUS | 1320 stored-travel positive boundary | soft limit per M80 manual | FANUC 1320/1321 are per-axis stored travel boundaries |
| Negative soft limit | MD36100 POS_LIMIT_MINUS | 1321 negative boundary | per M80 manual | leave travel margin inside the hard limit |
| Max axis acceleration | MD32300 MAX_AX_ACCEL | 1620 / 1622 accel/decel time constants | accel/decel time constants per M80 manual | Siemens is an acceleration value, FANUC mostly time constants — different dimensions |
| Rapid speed | MD32000 MAX_AX_VELO | 1420 per-axis rapid speed | rapid speed per M80 manual | units/ranges per each manual |
| Max cutting feed | SD43200 etc. (mode dependent) | 1422 max cutting feed | per M80 manual | – |
Reading note: backlash is the easiest item to “copy the wrong number” — Siemens MD32450 is usually in mm while Mitsubishi #2011/#2012 are in 0.5 um units, so the same 0.05 mm backlash is written completely differently. All soft limits must leave a safety margin inside the hard limit; verify against measurement and your manual.
29.3 Spindle: speed limits / gear shift / orientation / constant surface speed
Table 3 Spindle parameter cross-reference
| Function | SINUMERIK 828D/840D sl | FANUC | Mitsubishi M80 | Notes |
|---|---|---|---|---|
| Gear-step max/min speed | MD35140 GEAR_STEP_MAX/MIN_VELO_LIMIT | per-gear speed params per 0i/3x manual | per M80 manual | multi-gear spindles indexed by step |
| Spindle orientation angle | orientation MD/SD per manual | 4077 orientation stop position (common) | per M80 manual | angle works with PLC/PMC logic |
| Constant surface speed | G96 related setting data | G96 related params per manual | G96 related per manual | a G-code function; parameter items differ |
| Spindle sync | spindle-sync MD (MD35xxx series) | sync/rigid-tap params per manual | per M80 manual | varies by model/option — entry only, no value |
Discipline: spindle parameters are tightly coupled to the machine builder’s PLC/PMC logic (gear shift, orientation, sync all read the ladder) — during a conversion you cannot move parameter numbers alone; you must evaluate the PLC/PMC side together. Items not directly verifiable in a manual are listed as “per manual” with no guessed value.
29.4 Zero points and coordinate systems: G54-G59 / additional zero / offset write
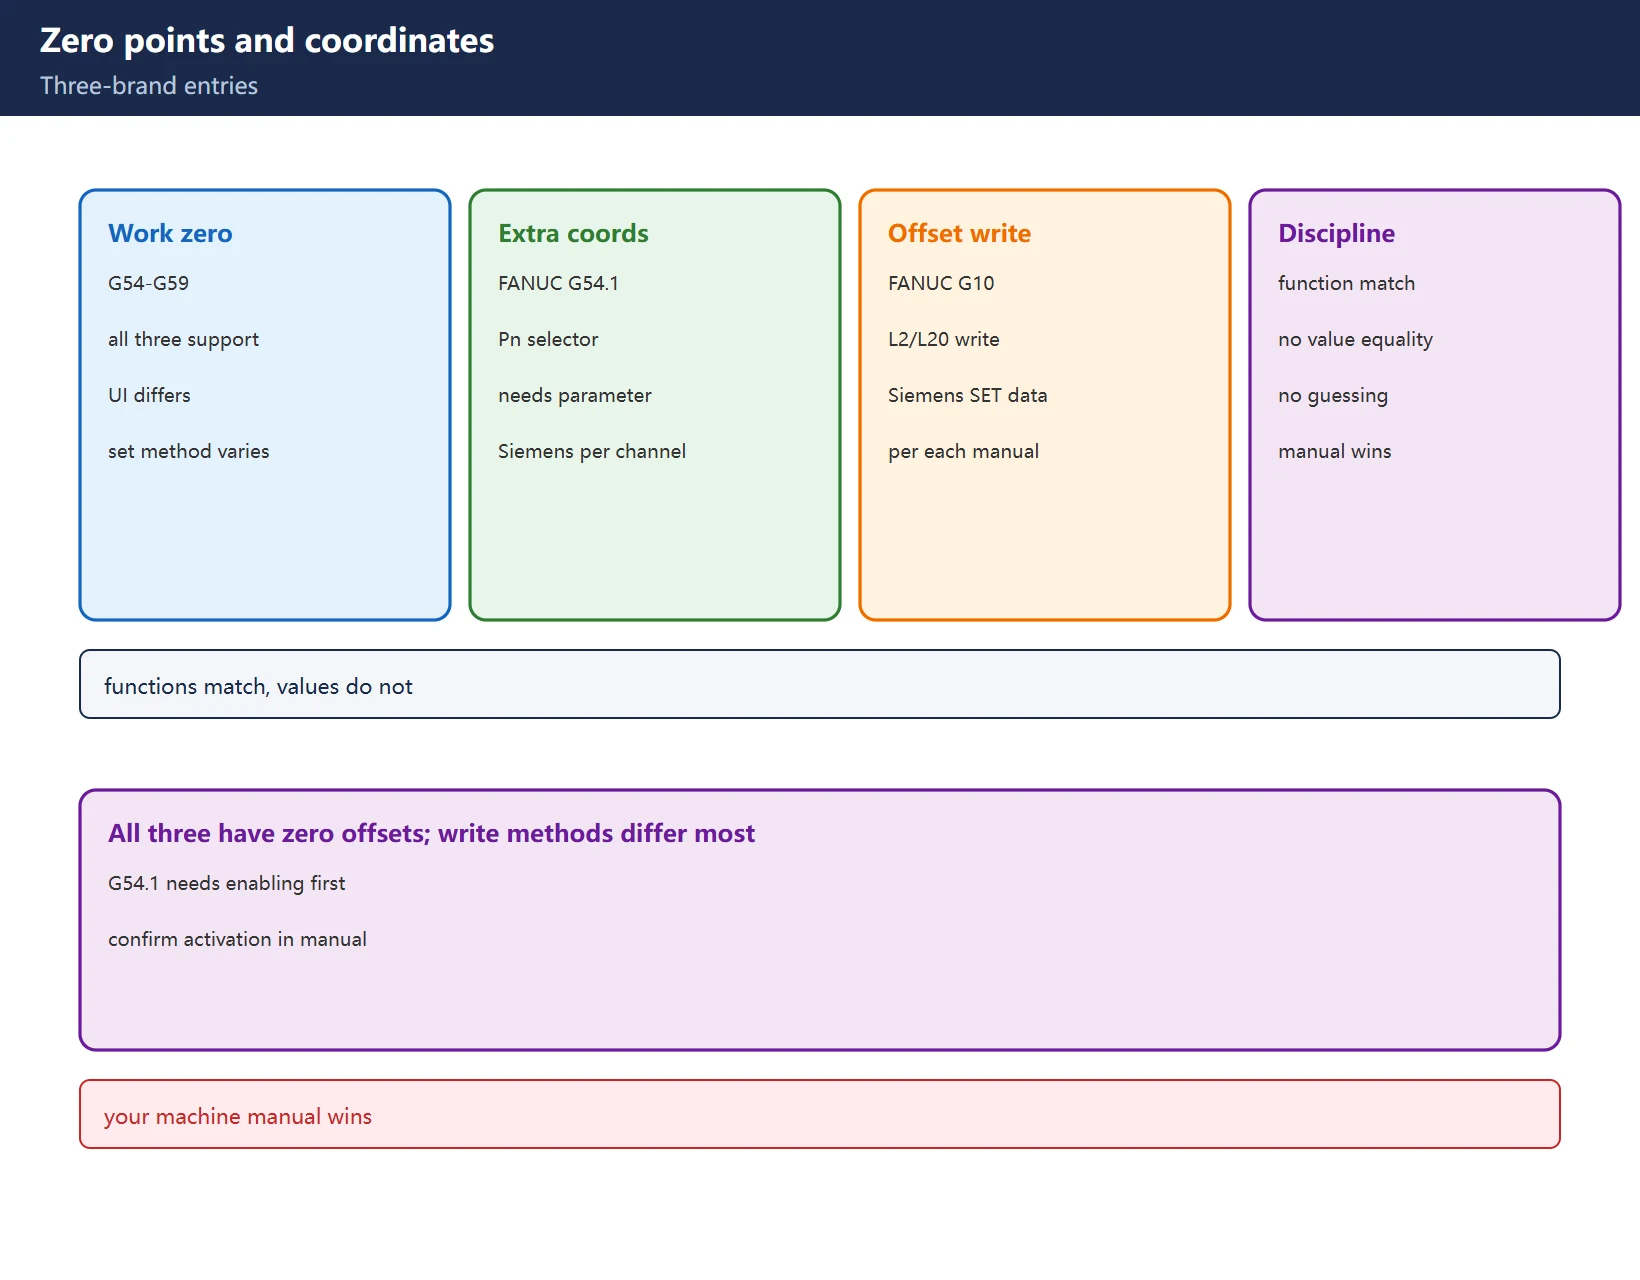
Table 4 Zero point and coordinate entry cross-reference
| Function | SINUMERIK 828D/840D sl | FANUC | Mitsubishi M80 | Notes |
|---|---|---|---|---|
| Workpiece zero offset | G54-G59 settable zero offsets | G54-G59 work coordinates | G54-G59 work coordinates | all three support it; UI/write method differs |
| Additional work coordinate | additional zero offsets per channel | G54.1 Pn additional work coordinates | additional coords per M80 manual | FANUC G54.1 needs a parameter enabled |
| Offset write | via SET/setting data or program | G10 L2/L20 write offsets | write command per M80 manual | write methods differ greatly |
29.5 Alarm / watchdog and battery related parameters
Table 5 Alarm and monitoring entry cross-reference
| Function | SINUMERIK 828D/840D sl | FANUC | Mitsubishi M80 | Notes |
|---|---|---|---|---|
| Contour monitoring threshold | MD32210 POSCTRL_MONITOR etc. | 1828 moving error limit / 1829 stopping error limit | per M80 manual | threshold meanings differ, per manual |
| In-position width | positioning window MD | 1826 per-axis in-position width | per M80 manual | – |
| Battery voltage / data retention | battery alarm MD/PLC bit | battery alarm and absolute-position params | per M80 manual | system level, see brand battery articles |
29.6 Lubrication / coolant / air pressure (pulse period / pressure-switch delay)
Table 6 Lubrication / coolant / air entry cross-reference
| Function | SINUMERIK 828D/840D sl | FANUC | Mitsubishi M80 | Notes |
|---|---|---|---|---|
| Lubrication pulse period | set by PLC program plus MD | set by PMC ladder plus timers/data table | set by PLC program | none has a single cross-brand parameter |
| Pressure-switch delay | PLC timer | PMC timer / D data table | PLC timer | field delay per process and manual |
| Coolant control | PLC / M function | PMC / M function | PLC / M function | no unified parameter number |
Key insight: auxiliary actions such as lubrication, coolant and air pressure are implemented in the PLC/PMC on all three controls — there is no “same-number cross-brand parameter”. Any claim of “parameter X is the lubrication period” must first identify which brand and which machine-builder PLC version.
29.7 Compression and filtering: MD32400 series vs FANUC notch vs Mitsubishi #2233/#2238
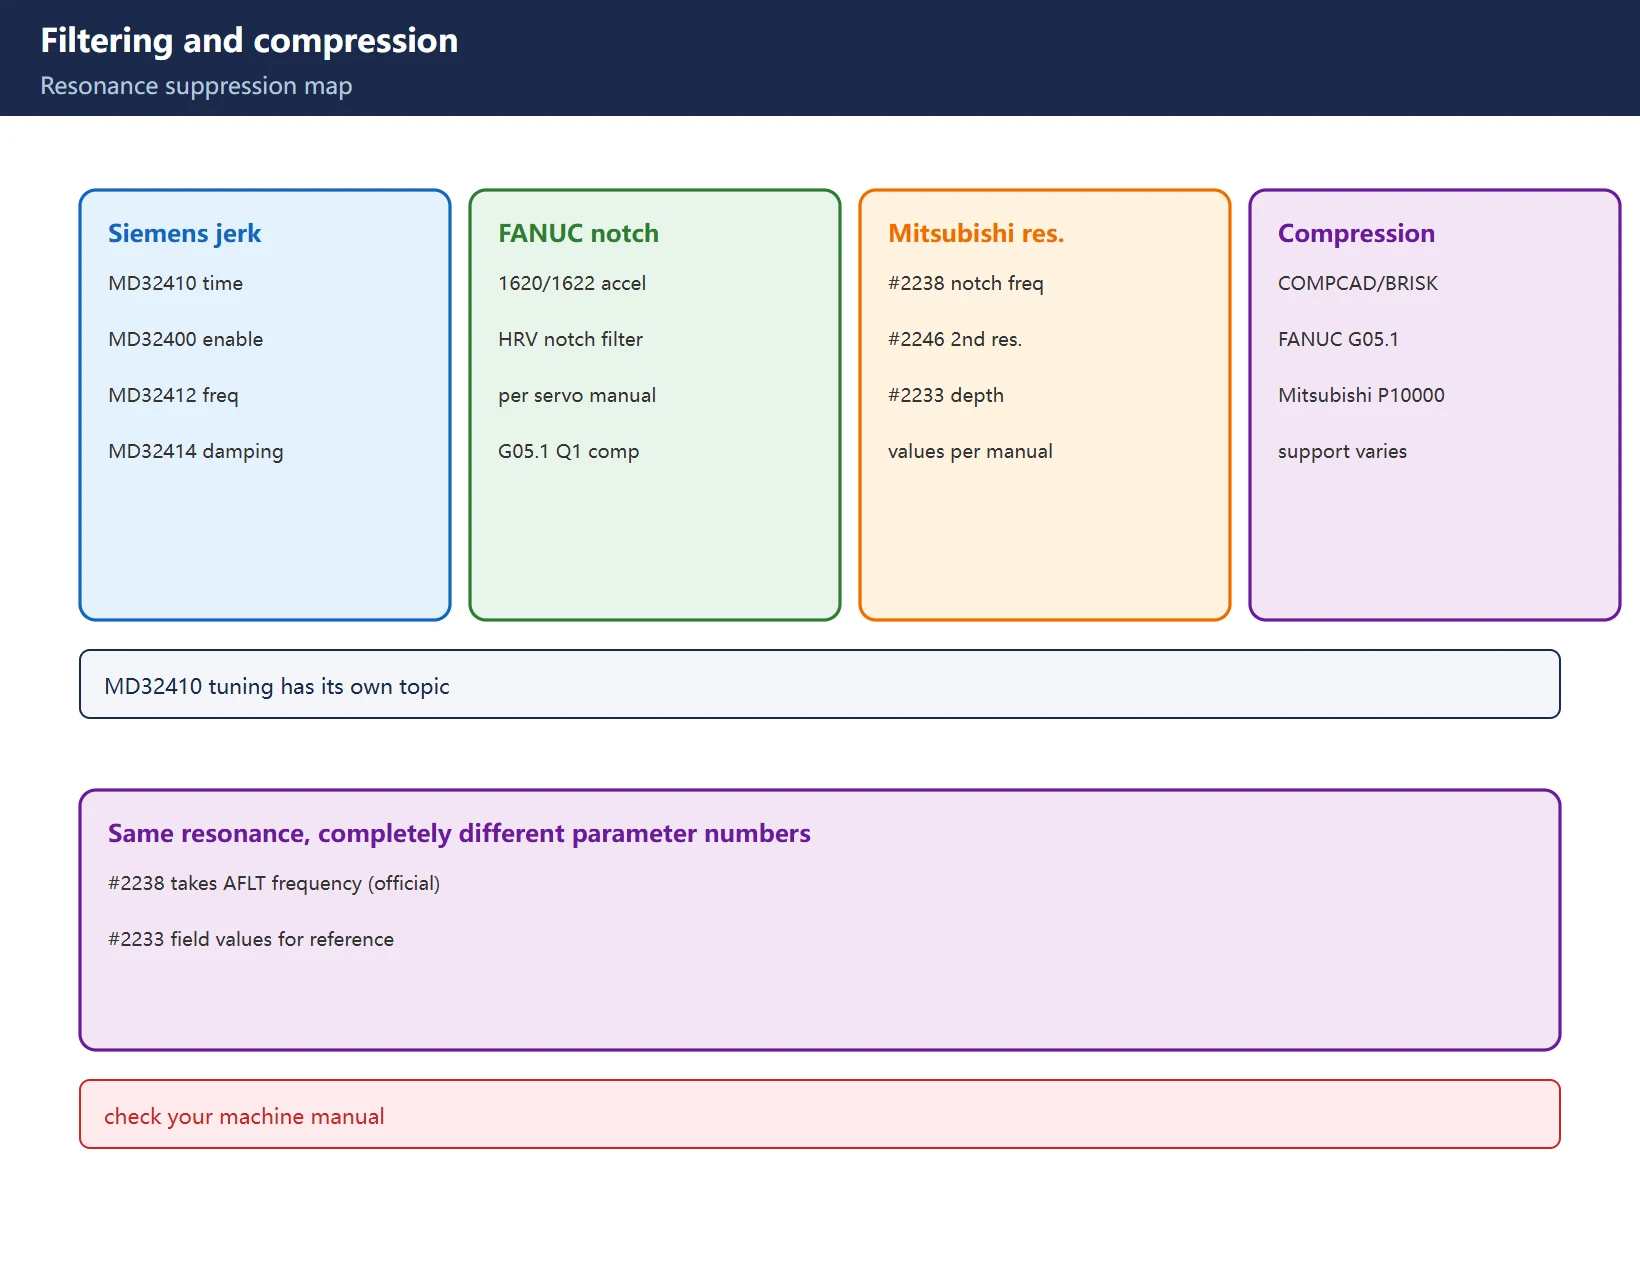
Table 7 Filter / compression / resonance-suppression cross-reference
| Function | SINUMERIK 828D/840D sl | FANUC | Mitsubishi M80 | Notes |
|---|---|---|---|---|
| Jerk filter time | MD32410 AX_JERK_TIME, MD32400 AX_JERK_ENABLE | accel/decel time constants 1620/1622, FAD related | accel/decel time constants per manual | Siemens jerk is a separate mechanism |
| Vibration filter frequency | MD32412 suppression frequency, MD32414 damping | notch filter params per HRV/servo manual | #2238 SV038 FHz1 notch freq 1, #2246 2nd resonance freq | Mitsubishi manual explicitly: #2238 takes the AFLT frequency |
| Notch depth / resonance depth | per MD damping terms | per servo manual | #2233 resonance depth (field values 0090/00A0/00B0, per manual) | #2233 values subject to official manual |
| Program compression | COMPCAD, BRISK (support differs 840D sl vs 828D) | AI contour control G05.1 Q1 related | high-precision mode G05 P10000 related | command names differ; support varies by model/option |
The dedicated MD32410 jerk-time tuning (including the 1/f rule) belongs to a separate SINUMERIK contour-error diagnosis topic on this site; this table gives the entry only.
29.8 Servo tuning family: Kv / position loop gain / inertia identification
Table 8 Core servo tuning parameter cross-reference
| Function | SINUMERIK 828D/840D sl | FANUC | Mitsubishi M80 | Notes |
|---|---|---|---|---|
| Position loop gain (Kv) | MD32200 POSCTRL_GAIN (axis index) | 1825 position loop gain (unit 0.01/s) | #2203/#2204 position-loop related (per manual) | units differ, values are not interchangeable |
| Speed loop gain | MD32810 speed-loop equivalent time etc. | 2021 inertia ratio (speed gain multiplier) | #2205 speed loop gain (field ~200, per manual) | FANUC 2021 is inertia ratio, not speed-gain body |
| Inertia ratio / identification | servo optimization incl. load-inertia ID | 2021 load inertia ratio | #2235 inertia identification related (per manual) | field values from measured identification |
| Feedforward | MD32620 FFW_MODE, MD32610 | 2005#1 feedforward enable, 2069 velocity FF gain | 2010 feedforward gain (field ~40, per manual) | bit/parameter numbers differ |
Correction reminder: online sources often call FANUC 2021 “speed loop gain” or 2083/2085 “position loop gain” — per official and multi-source data, 2021 is the load inertia ratio, 1825 is the position loop gain, and 2023 is the velocity feedback pulse count. Getting this wrong in a cross-reference breaks every downstream tuning decision.
29.9 Usage discipline and declaration repeated
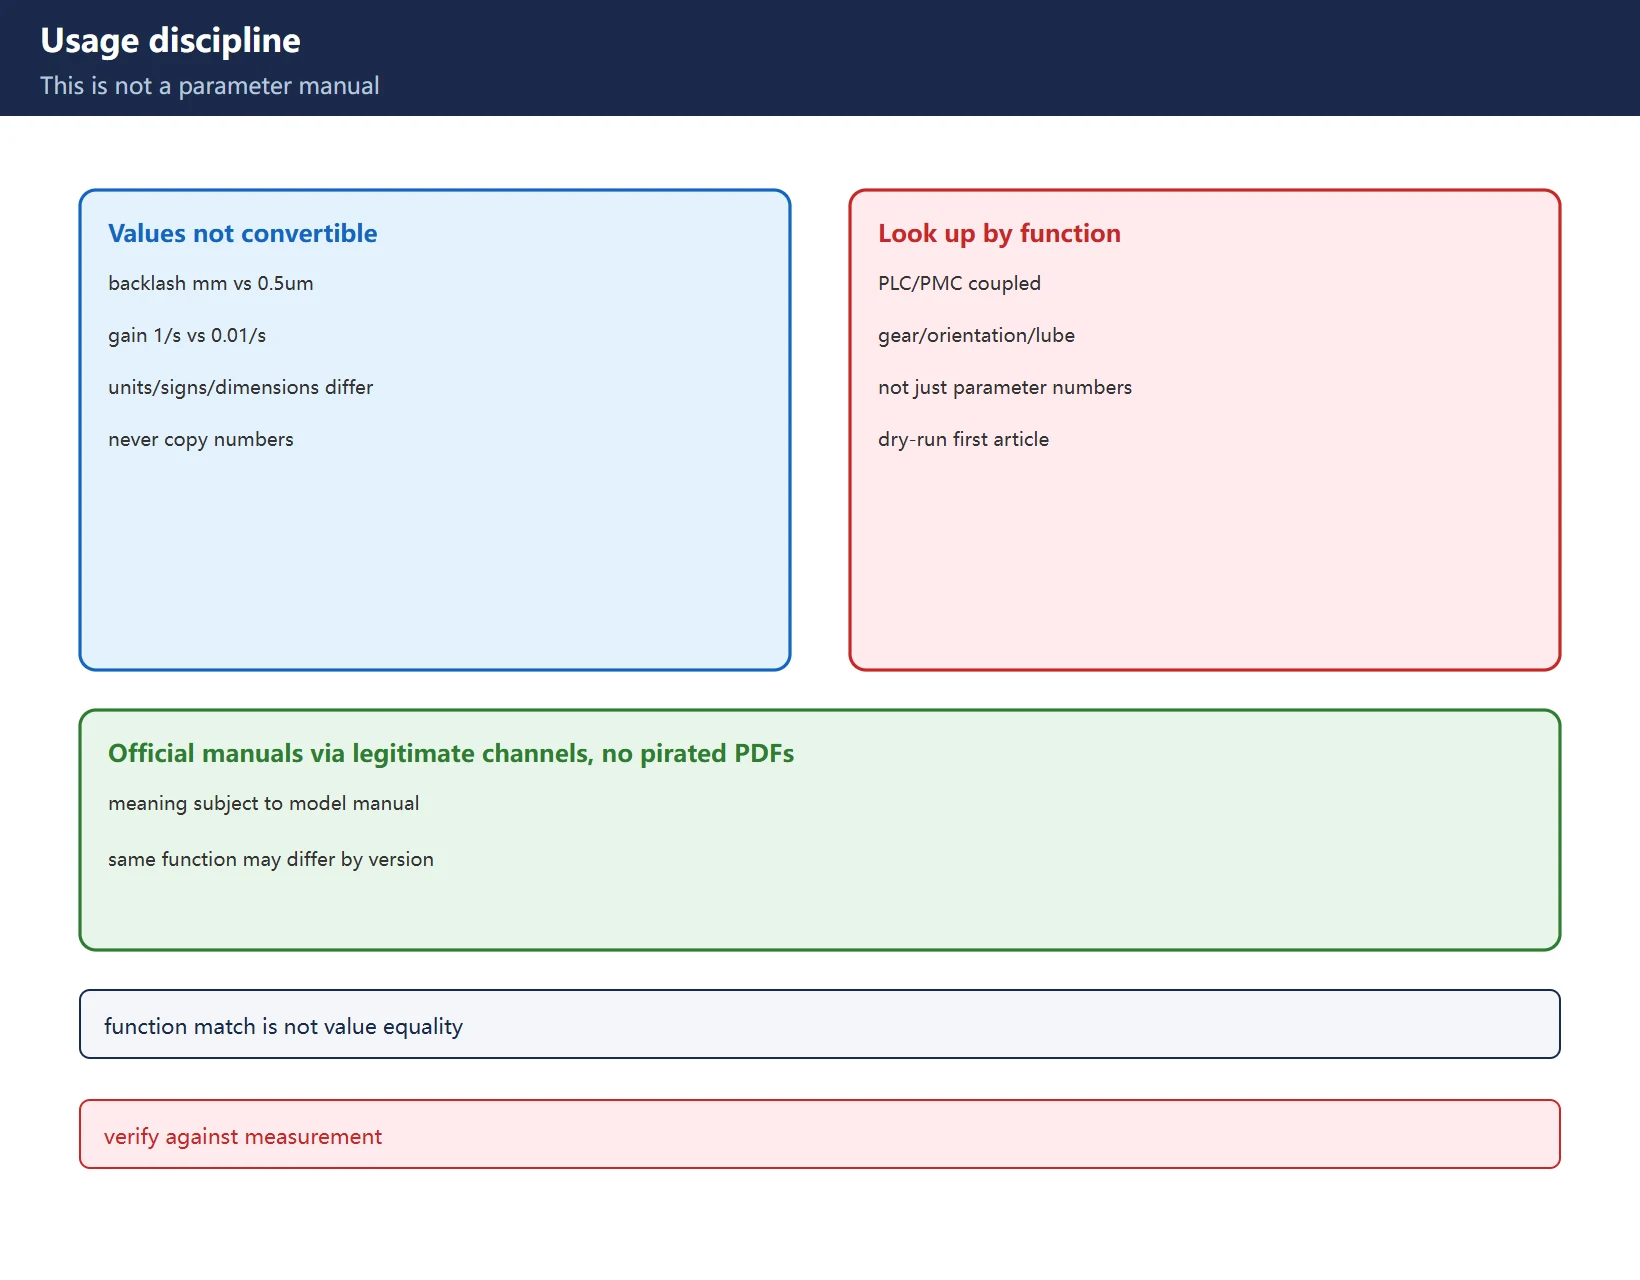
- This table is a function cross-reference and lookup entry only; meaning, units and activation conditions are subject to the official manual for the corresponding model.
- Values are not directly convertible: units, signs and dimensions differ (backlash mm vs 0.5 um, position gain 1/s vs 0.01/s).
- Look up by function, never guess by number: identify the function, find the entry, confirm in the manual.
- PLC/PMC-coupled items (gear shift, orientation, lubrication, air pressure) cannot be moved by parameter number alone — evaluate the ladder together.
- Official manuals via legitimate channels: this site does not host, reproduce or link pirated manual PDFs.
- Further reading: 828D MD Quick Reference, FANUC Parameter Number Map, Mitsubishi M80 Servo Parameters.
Frequently Asked Questions
Which FANUC parameter corresponds to the 828D soft-limit parameter?
By function: 828D/840D sl first soft limit negative is MD36100 POS_LIMIT_MINUS, positive is MD36110 POS_LIMIT_PLUS; FANUC’s counterparts are stored-travel boundary 1320 (positive) and 1321 (negative). But the units and setting methods differ, and both need a safety margin inside the hard limit — you can say “functionally corresponding”, never “numerically equal”, subject to each manual.
How do Siemens MD and FANUC parameters map one-to-one during a conversion?
There is no number-to-number mapping, only function-to-function. Correct workflow: (1) list the functions to migrate (backlash, gain, soft limit, accel/decel…); (2) find both controls’ entries by function in this table; (3) confirm each unit/sign/activation condition in the two official manuals; (4) re-tune from measurement, never copy values. The three numbering systems partition on completely different logic, so never guess by number range.
Can this table be used as a parameter manual, and what is authoritative?
No. This table is a function cross-reference and lookup entry, not a parameter manual, and it does not give a single “correct setting value”. Each parameter’s meaning, unit, range and activation condition are subject to the official manual for the corresponding model; the same function can differ across versions and machine-builder defaults. Verify against your machine’s manual and measurement before any field change, and dry-run the first article.
Last updated: 2026-11-20
Where to go next
- FANUC Troubleshooting — the full guide library: alarms, diagnosis numbers, servo, spindle, PMC and electrical faults, organised by symptom.
- CNC Repair Tools — which instrument measures what: multimeters, clamp meters, insulation testers and oscilloscopes, with the specification that actually matters.
- Remote Technical Support — have the readings reviewed with you: alarm reverse lookup, PMC ladder analysis and servo tuning advice by call. Repair companies and integrators welcome.
- Buying & Ownership Decisions — refurbished vs new, used-machine checks, software licensing and manuals: spend with the field facts in hand.
Read the guide, get the right instrument, or walk the diagnosis through with someone — pick whichever you need.




































暂无评论内容