



Sister article: 828D / 840D sl Servo Alarms 25000 / 25010 / 25201: Layered Troubleshooting (Chinese); related: SINUMERIK Drive Faults: F30020, F30021, F30011, F07011, Sinumerik F-Code Cross-Reference, SINUMERIK 840D sl Alarm Code Quick Reference, FANUC Alarm History and Operation History.
22.1 Three codes, three layers: one-glance triage
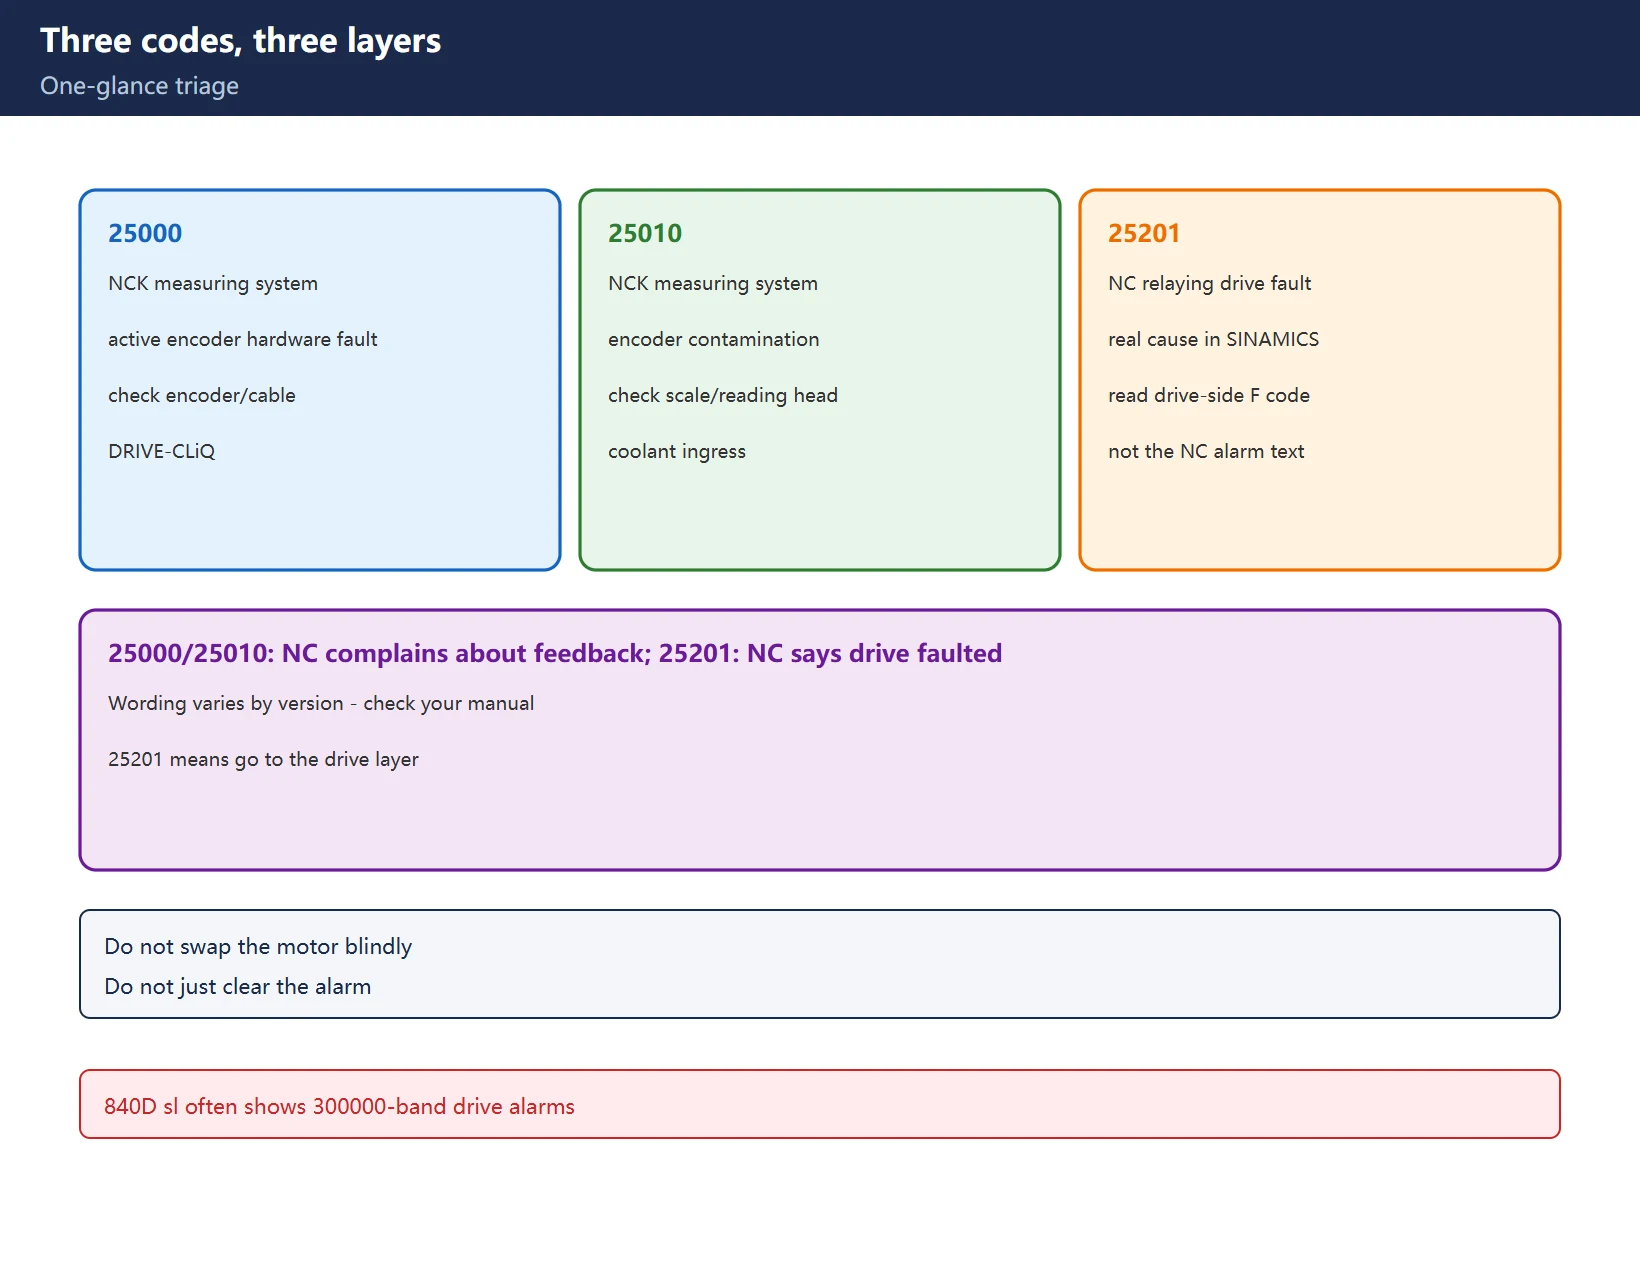
Table 1 25000 / 25010 / 25201 at a glance (plain text per your manual)
| Alarm | Layer | Typical wording (official/manual sources) | First place to look |
|---|---|---|---|
| 25000 | NCK – measuring system | “Axis %1 hardware fault of active encoder” | Encoder / cable / DRIVE-CLiQ of the selected measuring system |
| 25010 | NCK – measuring system | “contamination of encoder” / measuring-system signal quality | Scale, reading head, wipers, coolant ingress |
| 25201 | NC relaying a drive fault | “measuring circuit error” / “drive fault reported by the drive” | SINAMICS drive-side F code and fault object |
Key sentence: 25000 and 25010 are the NC complaining about its feedback; 25201 is the NC saying “the drive reported a fault” – go read the drive, not the NC alarm list.
22.2 ★ The correct entry point for 25201
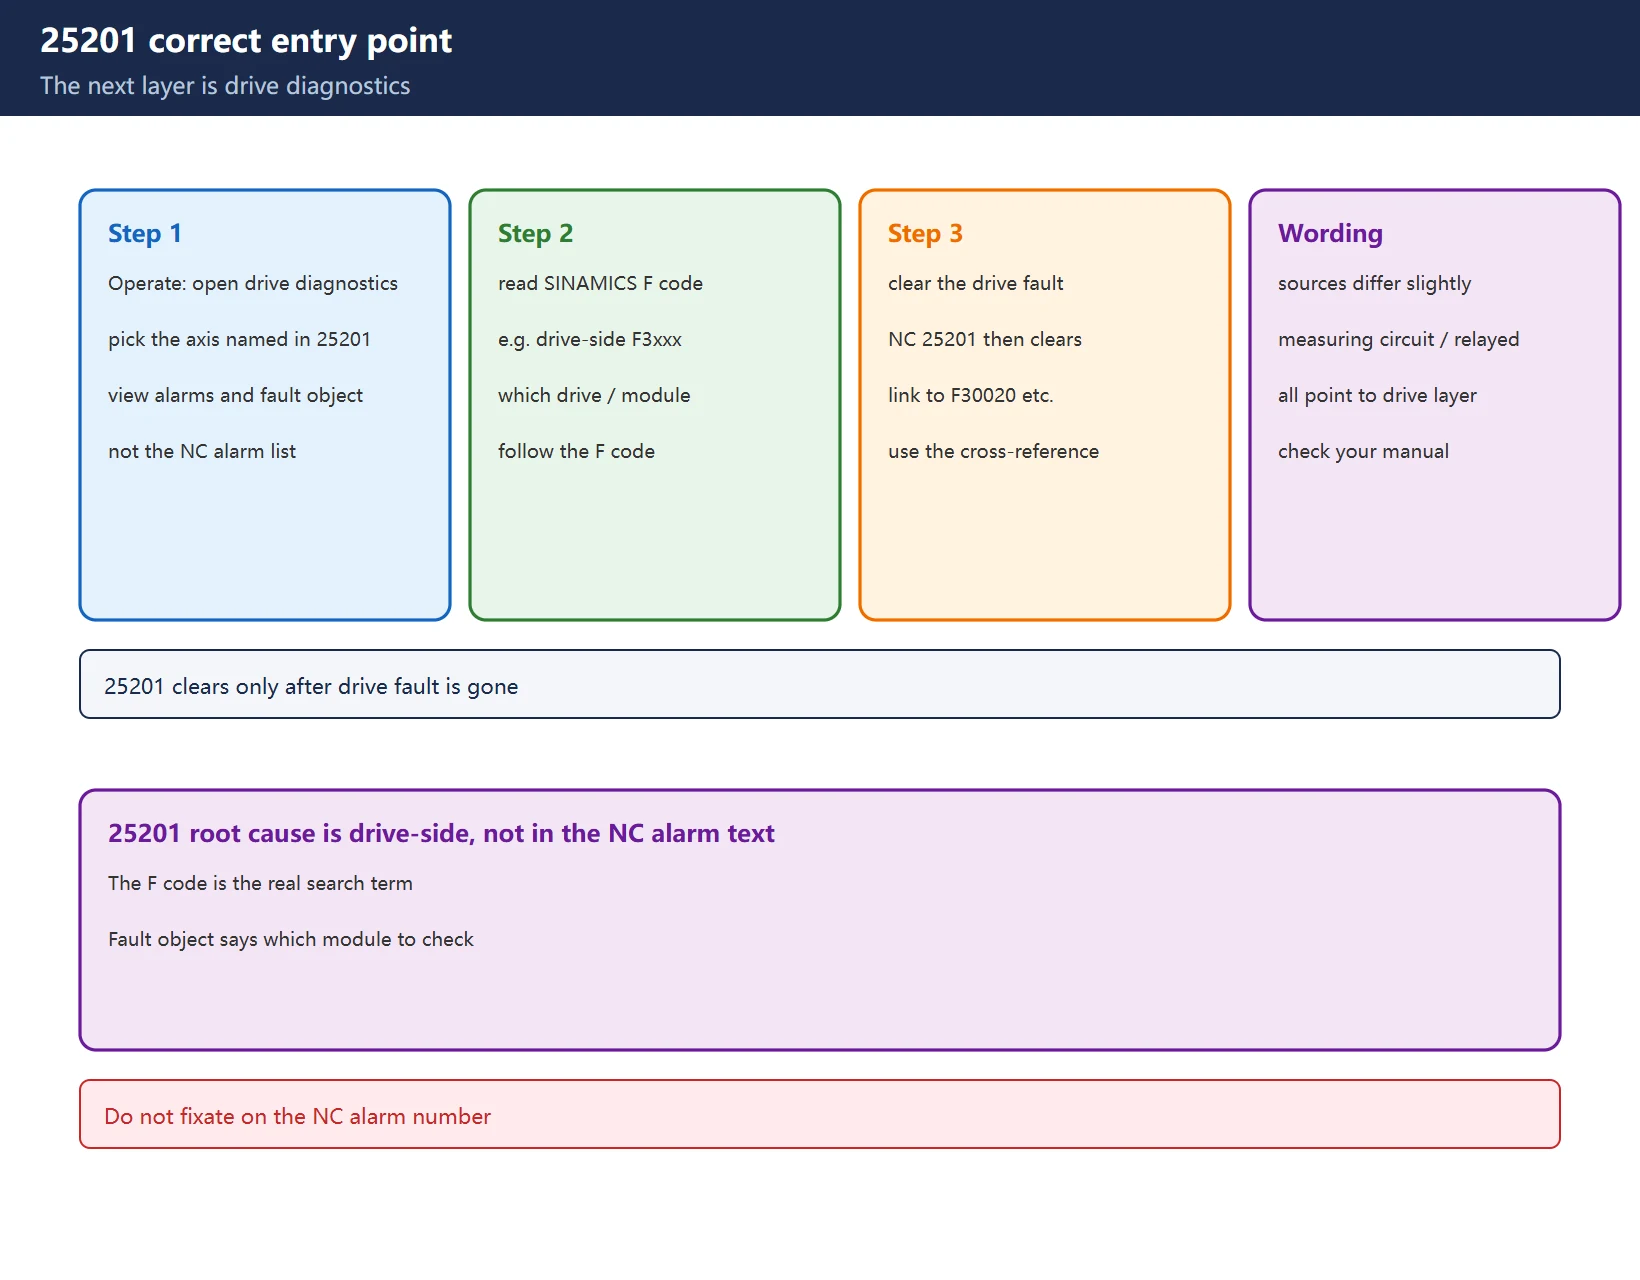
This is the core value of the article: do not hunt for the root cause in the NC alarm text of 25201. The useful information is one layer down:
- In SINUMERIK Operate, open the drive diagnostics / alarms for the axis named in 25201;
- Read the SINAMICS-side F code (e.g. an F3xxx on the drive) and the fault object (which drive, which sensor module);
- Follow that F code – see drive fault codes F30020 / F30021 / F30011 and the F-code cross-reference;
- Only after the drive fault is cleared does 25201 disappear on the NC side.
Reports differ slightly on 25201’s plain text (“encoder measuring circuit error” in one source, “drive fault relayed to NC” in another), but both point to the drive layer – that is the robust takeaway. 300000-band drive alarms often accompany it on 840D sl.
22.3 The three checks for 25000
25000 = a hardware fault of the currently active encoder (measuring system 1 or 2, chosen by machine data). Check in this order:
- Encoder cable and connector at the motor and at the cabinet entry – pushed pins, moisture, coolant, loose latch; flex the cable in the drag chain while watching the position display;
- DRIVE-CLiQ connection on the drive side – seating and topology;
- Encoder / reading head itself – only after wiring is proven good. Note the alarm may name the active vs passive encoder differently (25000 active, 25001 passive on some systems).
Table 2 25000 three-check order (per your diagnostics manual)
22.4 Three field root causes for 25010
25010 = contamination of the measuring system / degraded signal quality. Typical physical causes:
- Scale contamination or damaged reading head – dirt or oil on the scale, worn encoder disc;
- Coolant ingress – along the scale body and cable path, the most common cause on machine tools;
- Failed wiper / guard – the seal that should keep swarf and coolant off the scale.
This is the SINAMICS-side equivalent of the scale fault family covered for HEIDENHAIN encoders on this site; the physical diagnosis (clean, reseal, then replace) is the same – cross-check against your own manual.
22.5 Triage by “when it happens” – often faster than by code
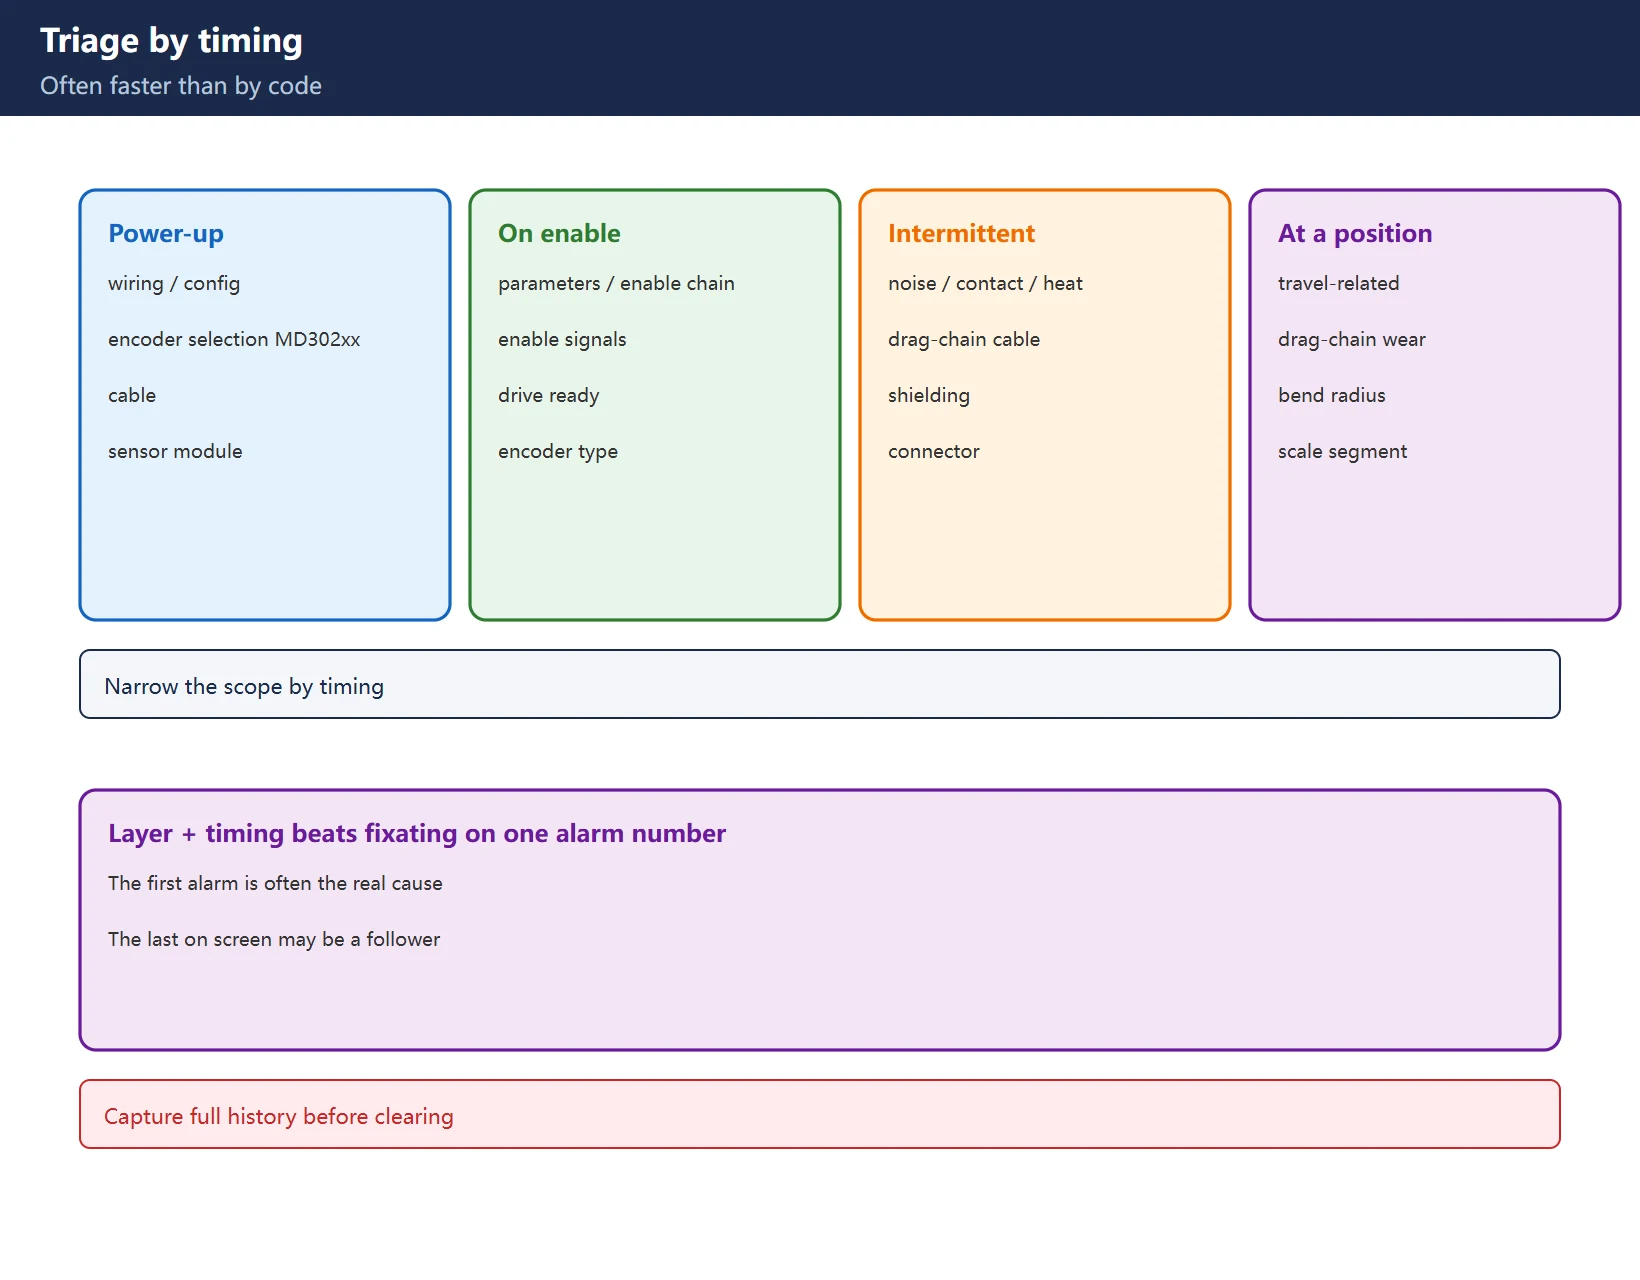
Table 3 Triage by alarm timing
| When it appears | Most likely family | First check |
|---|---|---|
| On power-up, axis never moves | Wiring / configuration | Encoder selection (MD302xx), cable, sensor module |
| As soon as the axis enables | Parameters / enable chain | Enable signals, drive ready, encoder type setting |
| Intermittently while running | Interference / poor contact / heat | Drag-chain cable, shielding, connectors |
| Only at a certain position | Travel-related | Drag-chain wear, cable bend radius, scale segment |
Combined with the code layer (22.1), timing narrows the fault far faster than chasing one alarm number.
22.6 Feed axis versus spindle
25201 on a feed axis usually points to that axis’s drive and its encoder. On a spindle, the path differs: the spindle encoder and orientation / tool-position signals are involved, so check the spindle sensor module and the tool-change position feedback path as well. Do not apply the feed-axis checklist verbatim to the spindle.
22.7 ⚠️ Do not “clear the alarm” as a repair
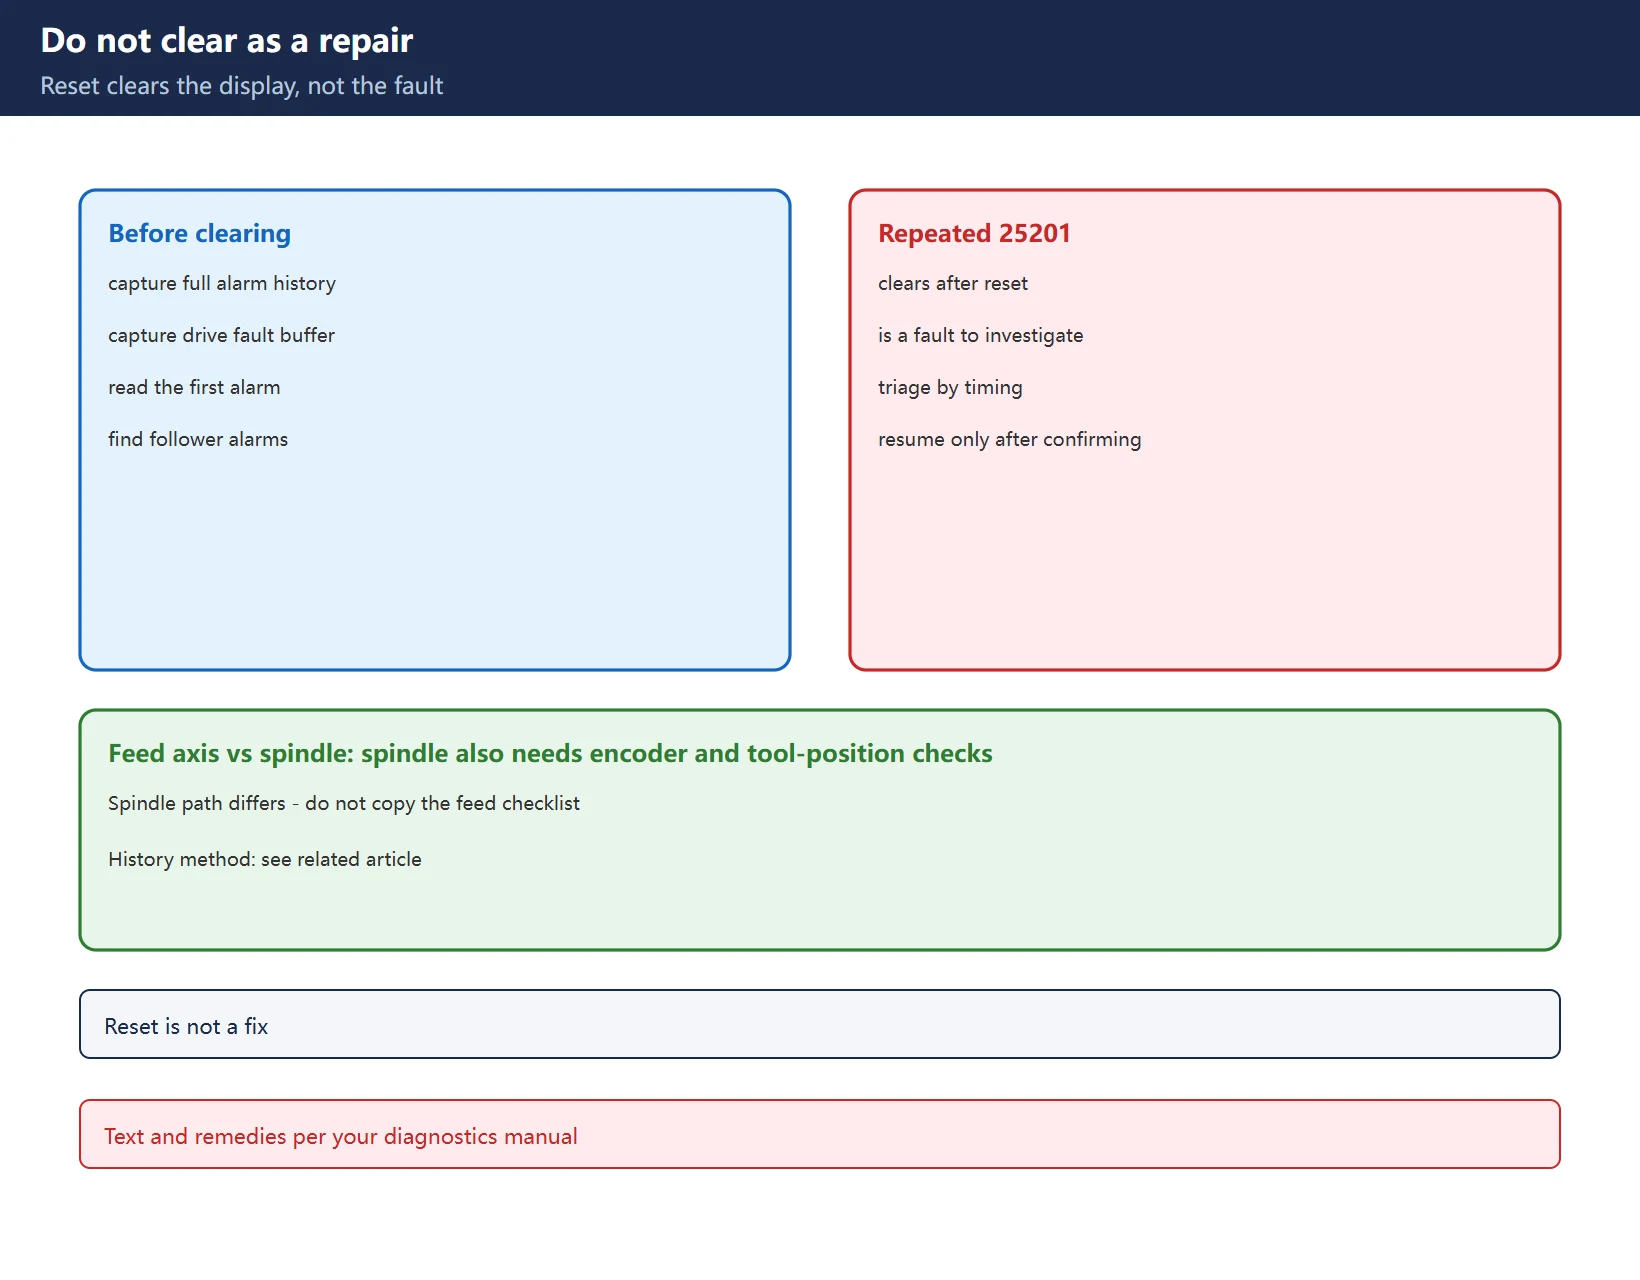
Resetting an alarm does not remove the fault. Before clearing, capture the full alarm history (and the drive fault buffer) – the first alarm in the chain is often the informative one, while the alarm you see on screen may be a downstream follower such as a limit-switch alarm. See alarm and operation history tracing for the method. Repeated 25201 that “goes away after reset” is a fault to investigate, not a nuisance to ignore.
Frequently Asked Questions
What does 25201 mean on an 828D, and where is the root cause found?
25201 is the NC relaying “this axis’s drive has a fault” – the real cause is on the SINAMICS side. The correct entry point is the drive diagnostics: read that axis’s F code and fault object, rather than hunting in the NC alarm text.
What is the difference between 25000 and 25010? Are both encoder-related?
25000 is a hardware fault of the currently active encoder (check encoder, cable, DRIVE-CLiQ); 25010 is measuring-system contamination or poor signal quality (check scale, reading head, coolant ingress). Both are NCK measuring-system alarms, but the root causes differ.
A servo alarm is intermittent and clears after reset – can production continue?
No. A reset clears the display, not the fault. Capture the full alarm history and drive fault buffer first (the first alarm in the chain is often the real cause), triage by when it happens, and only then resume.
Last updated: 2026-11-19
Where to go next
- FANUC Troubleshooting — the full guide library: alarms, diagnosis numbers, servo, spindle, PMC and electrical faults, organised by symptom.
- CNC Repair Tools — which instrument measures what: multimeters, clamp meters, insulation testers and oscilloscopes, with the specification that actually matters.
- Remote Technical Support — have the readings reviewed with you: alarm reverse lookup, PMC ladder analysis and servo tuning advice by call. Repair companies and integrators welcome.
- Buying & Ownership Decisions — refurbished vs new, used-machine checks, software licensing and manuals: spend with the field facts in hand.
Read the guide, get the right instrument, or walk the diagnosis through with someone — pick whichever you need.




































暂无评论内容