





最新发布第26页
排序
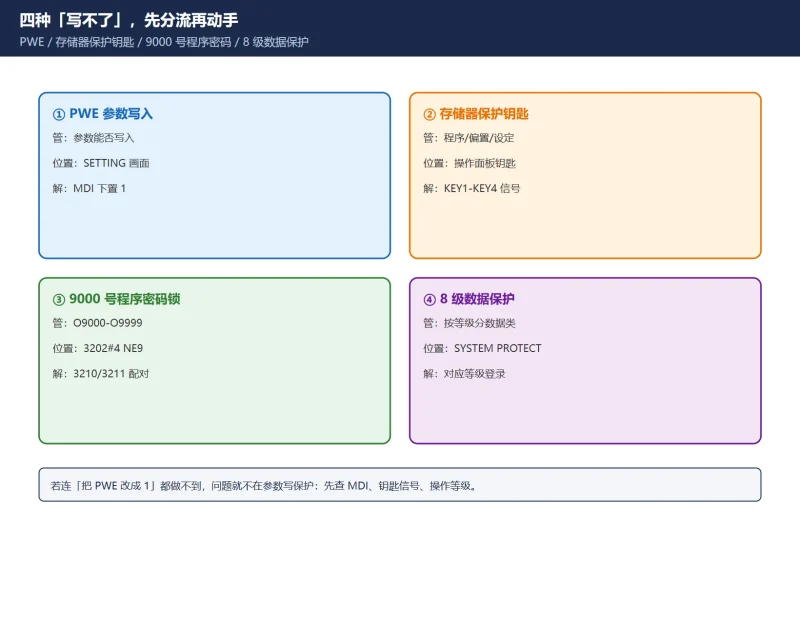
FANUC 参数改不了/写不进去怎么解除?PWE 参数写入开关 + SW0100 + 3210/3211 与 3202#4 NE9 混淆纠正
参数写不进去,先分清是 PWE 没开、程序编辑被保护、9000 号程序密码锁,还是新机的 8 级保护。本文给 MDI 到 SETTING 开 PWE 的完整路径,说明 SW0100 只是状态提示,并纠正把 3210/3211、3202...

 6天前
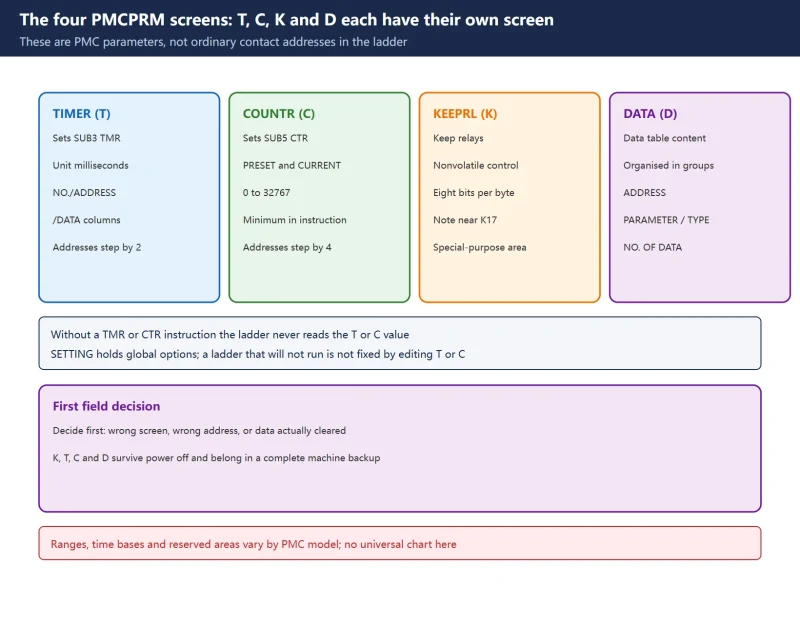
FANUC PMC Data Table, Counter, Timer and Keep Relay Quick Reference: The Four PMCPRM Screens
T, C, K and D are PMC parameters maintained on the TIMER, COUNTR, KEEPRL and DATA screens under PMCPRM. Verifiable screen roles, byte structure evidence for T and C, reserved areas...
6天前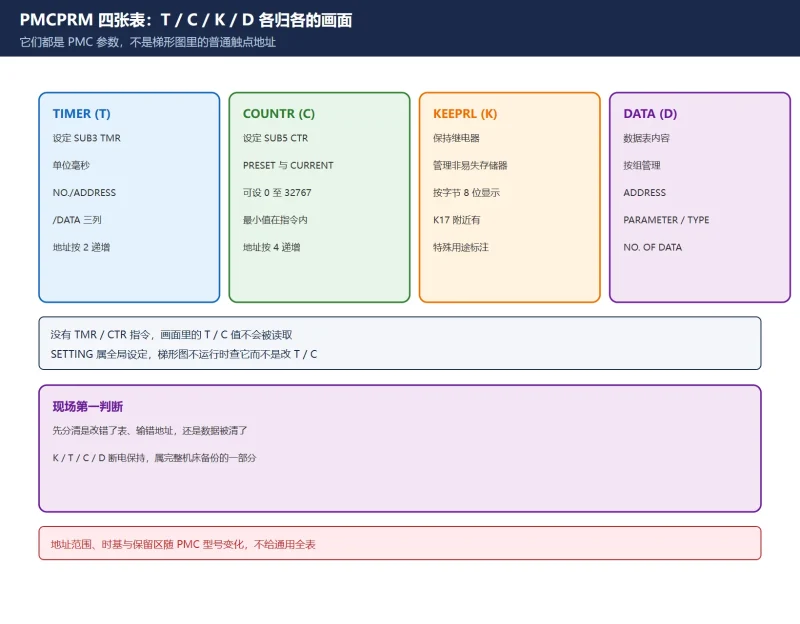
FANUC PMC 数据表 / 计数器 / 定时器 / K 继电器速查:PMCPRM 四张表与地址字节结构
T / C / K / D 都是 PMC 参数,统一在 PMCPRM 的 TIMER、COUNTR、KEEPRL、DATA 四张表维护。本页给出官方可核实的画面职责、T 占 2 字节与 C 占 4 字节的证据、保留区与 MDI 写入六步。
6天前
一文读懂 FANUC 0i-D 系列 CNC 系统:型号、功能与应用全解析
本文全面介绍 FANUC 0i-D 系列 CNC 系统的型号分类(0i-MD/0i Mate-MD、0i-TD/0i Mate-TD)、核心功能、硬件配置及应用场景,通俗易懂,助力机械行业从业者快速了解选型要点。
6天前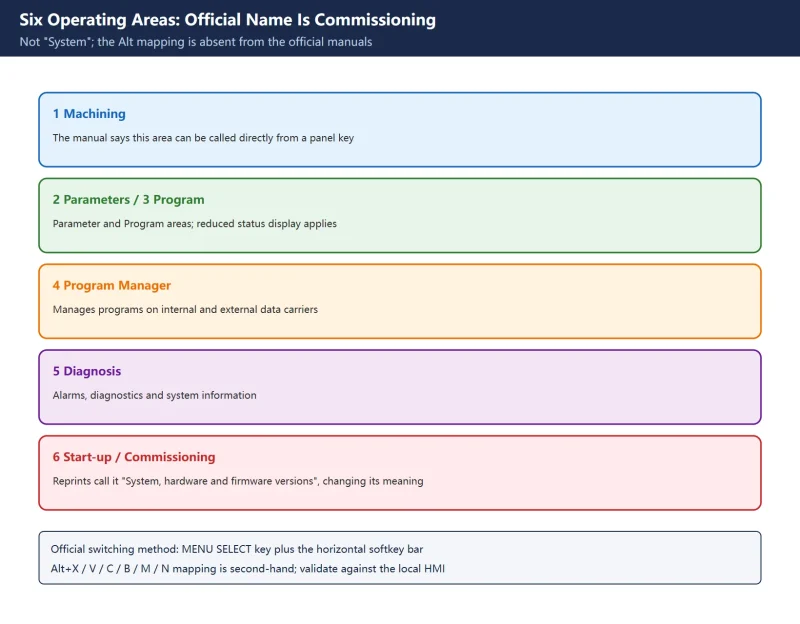
SINUMERIK 828D / 840D sl Shortcut Keys Verified Against the Official Manuals: Six Operating Areas, Ctrl / Alt Keys and the ARC / ARD Split
Circulating 'complete Sinumerik shortcut lists' are same-source reprints that get 840D sl Ctrl+Alt+S wrong, rename the sixth operating area and drop two official notes. Every key c...
6天前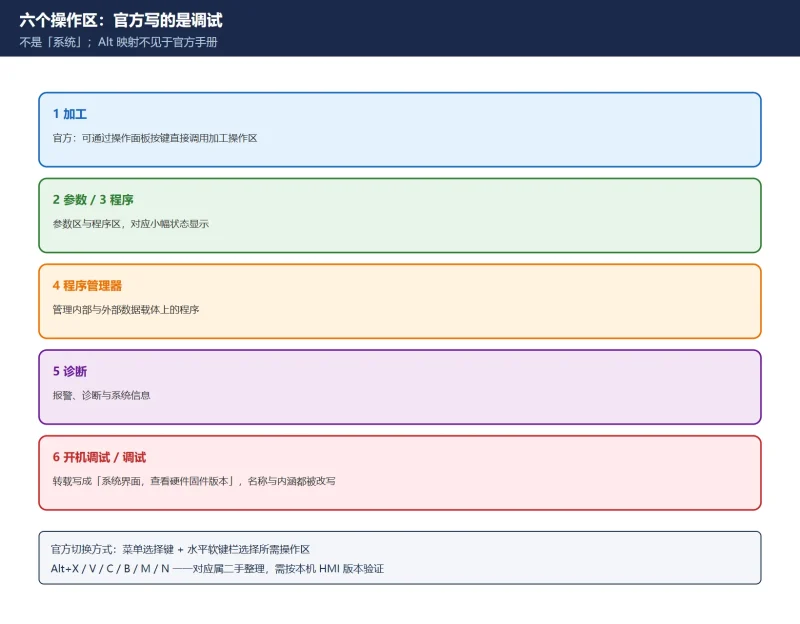
SINUMERIK 828D / 840D sl 快捷键速查(官方手册核实版):六个操作区 + Ctrl / Alt 组合键 + .ARC / .ARD 版本差异
中文转载的「西门子快捷键大全」是同源稿件,把 840D sl 的 Ctrl+Alt+S 也写成 .ARD,把第六个操作区写成「系统」,还漏掉官方两条注意事项。本页按官方操作手册逐条核实,并点破官方中文版 PDF...
6天前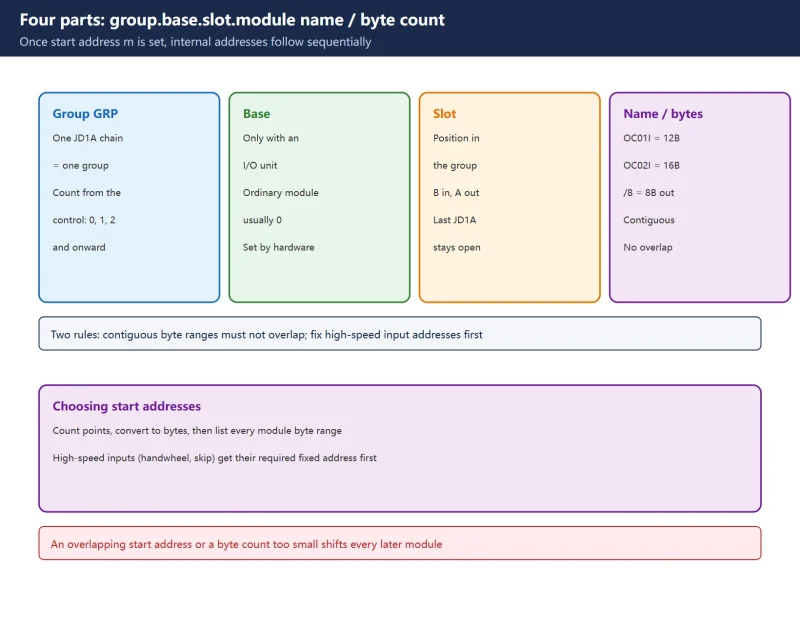
FANUC I/O Link Address Assignment: Group.Base.Slot, OC01I / OC02I and the 16-Byte Handwheel Rule
I/O Link address assignment is a four-part expression of group, base, slot and module byte count. Module byte counts, why a handwheel needs 16 bytes, I/O Link vs I/O Link i, and a ...
6天前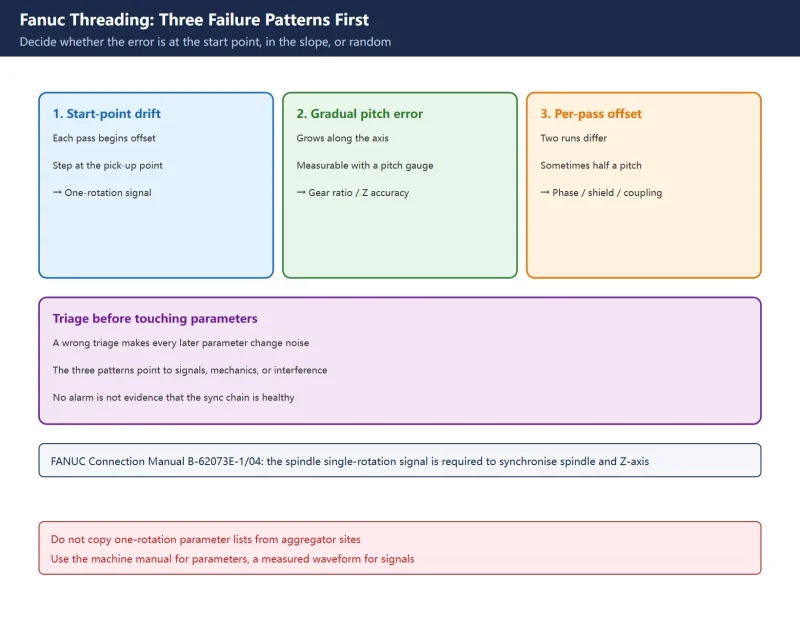
Fanuc Threading G32 / G92 / G76: Fixing Pitch Errors and Spindle Sync Problems
Thread pitch errors are rarely fixed by tweaking a tool offset. The real cause is a broken sync chain between the spindle one-rotation signal and Z-axis feed per revolution. Covers...
6天前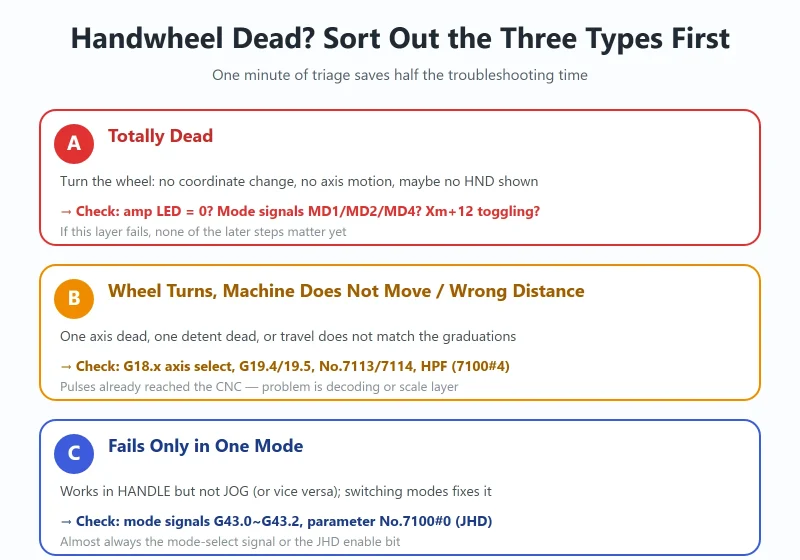
FANUC MPG Handwheel Not Working? Signal-Chain Troubleshooting: Servo Ready, I/O Link Assignment, Parameter Priority
FANUC handwheel (MPG) not working? Check in a fixed order: αi amplifier LED showing 0 = servo ready, HA/HB waveform and 5 V, I/O Link 16-byte OC02I assignment and the JA3 either/o...
6天前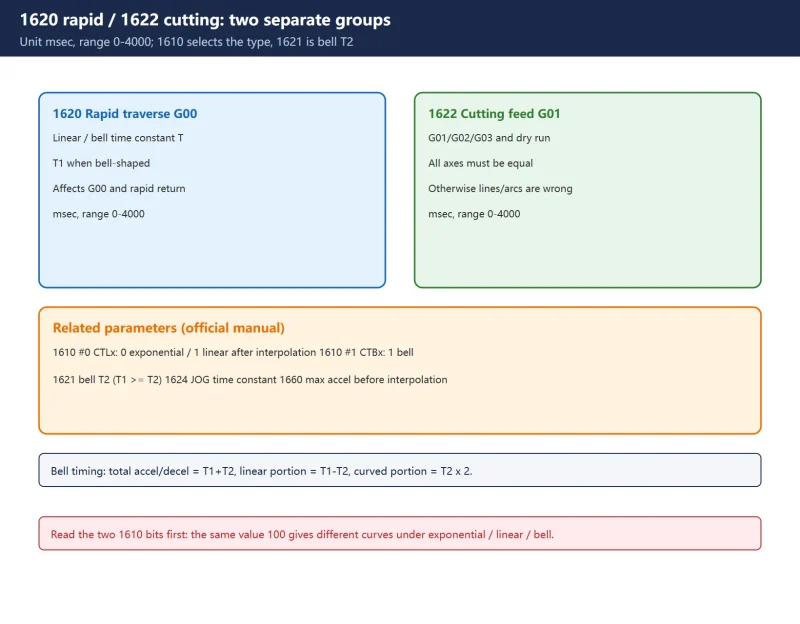
FANUC Acceleration/Deceleration and Corner Slowdown: 1620 Rapid, 1622 Cutting, and the Trade-offs
Parameter 1620 governs rapid-traverse accel/decel and 1622 governs cutting-feed accel/decel, both in msec; 1610 selects exponential, linear or bell-shaped and 1621 sets bell T2. Th...
6天前






扫一扫,添加我的微信










