





最新发布第4页
排序
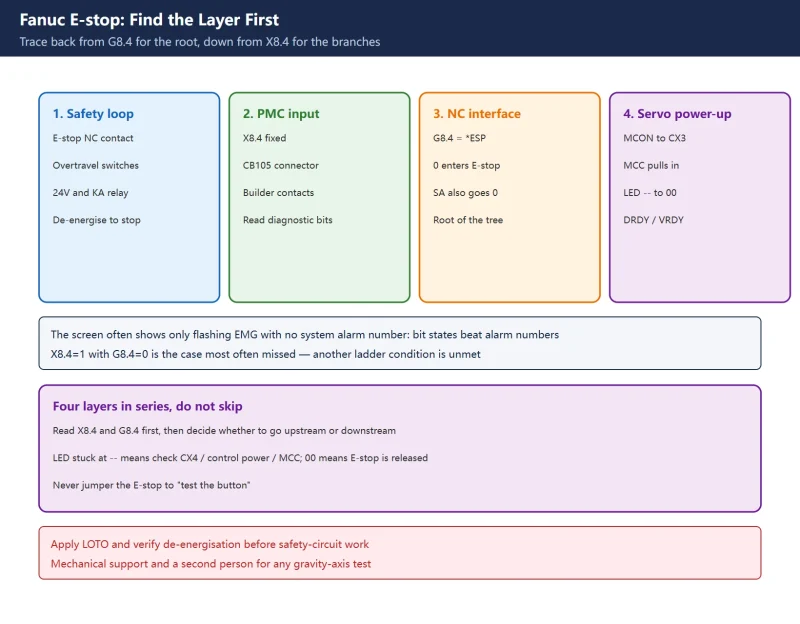
Fanuc E-Stop Circuit: G8.4, X8.4 Signals and Why the Servo Is Not Ready
Releasing the E-stop does not bring the servo back, and the control often gives no alarm number. Walks the four-layer chain: 24V safety loop, X8.4, G8.4, SA / MCC / CX4, with an X-...

 昨天
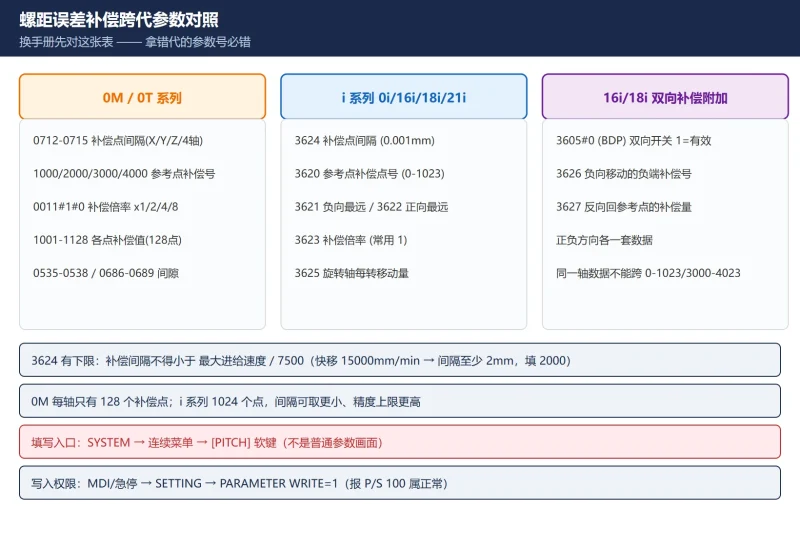
FANUC 螺距误差补偿 3620–3624 全流程:激光干涉仪测量 → 补偿点编号计算 → 参数填写 → 精度验证
FANUC 螺距误差补偿 3620-3624 全流程:跨代参数对照表(0M 0712-0715/1000-1128 ↔ i 系列 3620-3624 ↔ 16i/18i 双向 3605#0/3626/3627)、激光干涉仪测量与单向定位逼近、补偿点编号计算(负...
昨天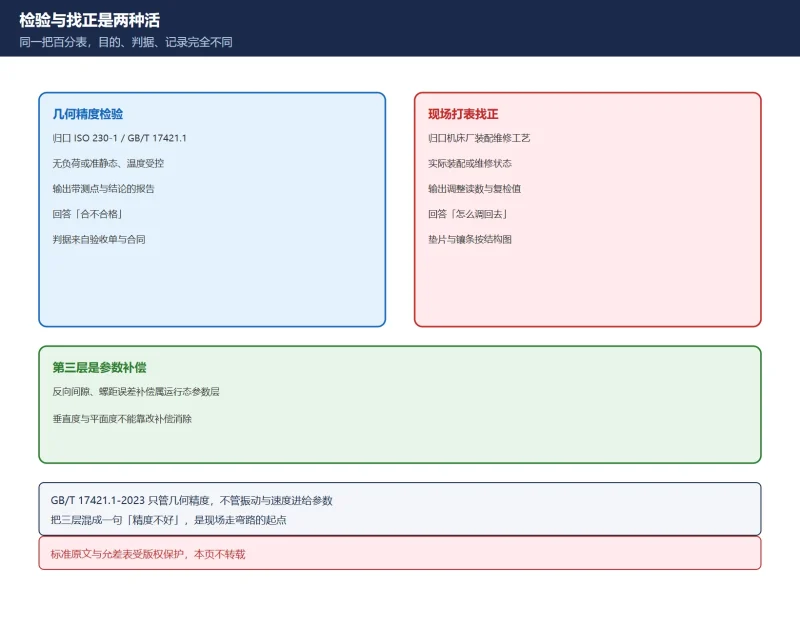
机床几何精度检测项 × 检具 × 判据 × 调整部位 对照框架:ISO 230-1 与 GB/T 17421.1 分册、五类几何误差族、判据来源纪律
网上流传的「几何精度判据表」大多把标准号挂错、把某一台带 B 轴机型的七项当成通用清单、再给一组互相打架的允差数字。本页按 ISO 230-1 / GB/T 17421.1 重新搭框架,只给方法族与检索导航,...
昨天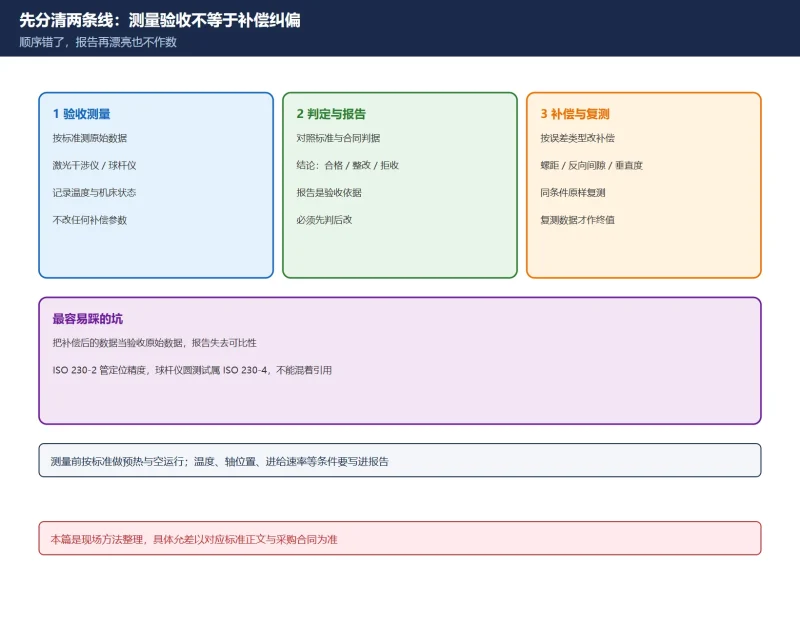
机床精度检验怎么做?球杆仪 ISO 230-4 与激光 ISO 230-2 判据对照
球杆仪做的是圆测试(ISO 230-4),激光干涉仪做的是定位精度与重复定位(ISO 230-2 / GB-T 17421.2),两者不是一套判据。本文给出标准分工、球杆仪六步作业、官方七类误差诊断项与验收结论三...
昨天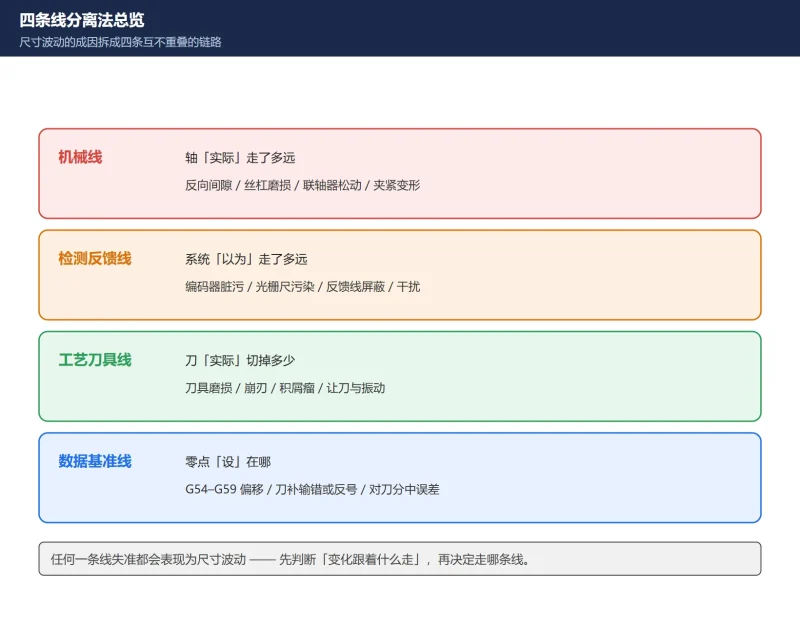
加工尺寸忽大忽小怎么查?四条线分离法:机械线 / 检测反馈线 / 工艺刀具线 / 数据基准线,一次把波动源分开
尺寸忽大忽小别再靠反复调刀补硬压 —— 刀补只修稳定的系统偏差,修不了随机漂移。用四条线分离法先判断「变化跟着什么走」:随件数走是刀具磨损,随时间走是热变形,随位置走是丝杠/螺距,随...
昨天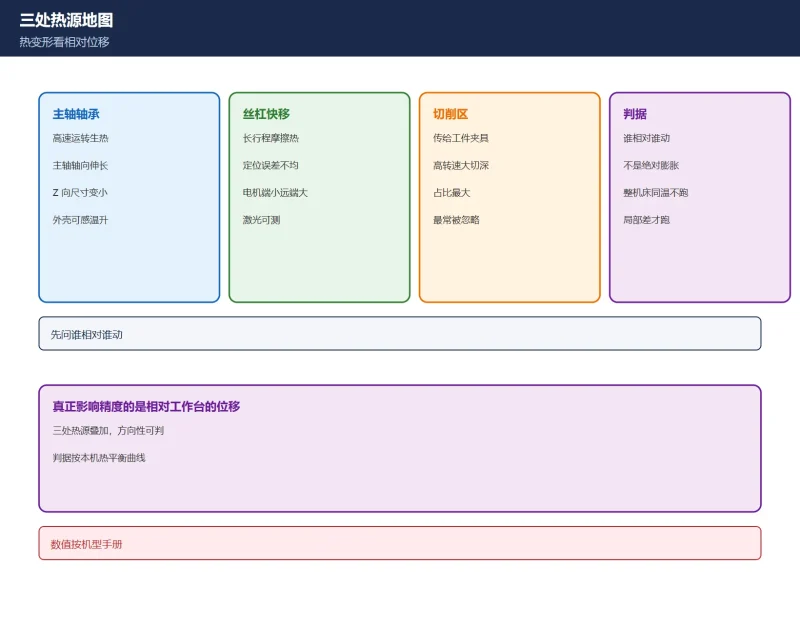
机床为什么要预热?热变形与首件精度漂移:三处热源 + 20 分钟预热协议 + 主轴油温与环境温度设定 + 热伸长诊断方法
机床预热与热变形全解:三处热源地图、两个方向性判据、20 分钟分档预热协议、千分表热平衡判定、主轴油冷机低 2–3℃ 设定、软件补偿不能替代预热的边界与设备台账化。数值按本机手册与实测热...
昨天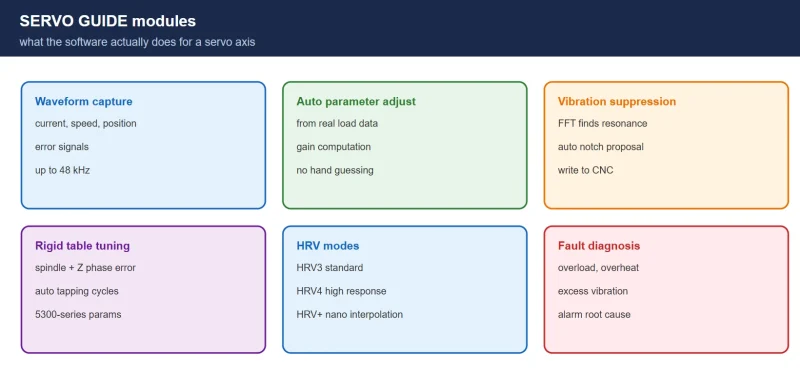
FANUC SERVO GUIDE: Waveform Analysis, Vibration Suppression and Rigid Tapping
A field guide to FANUC SERVO GUIDE: what it does, which controls it supports, how to install and connect over Ethernet, and the four workflows that solve most servo problems.
昨天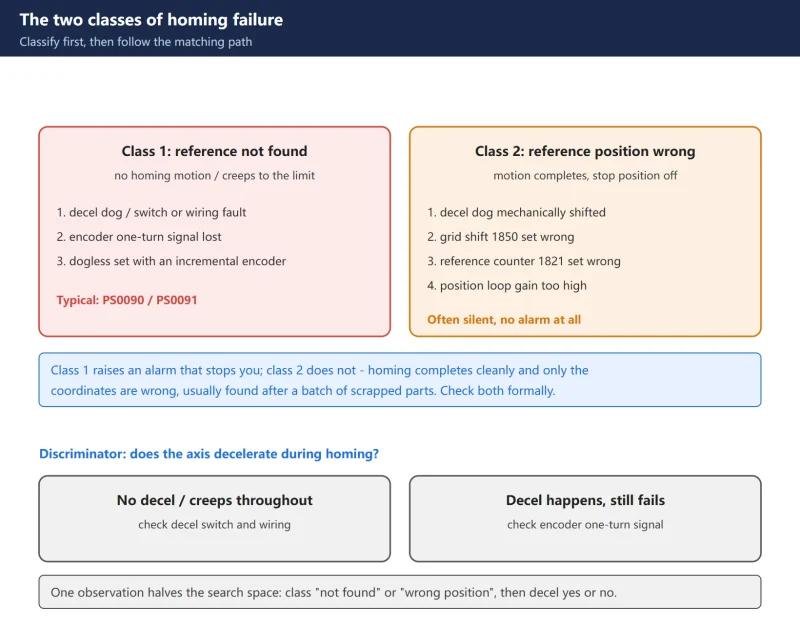
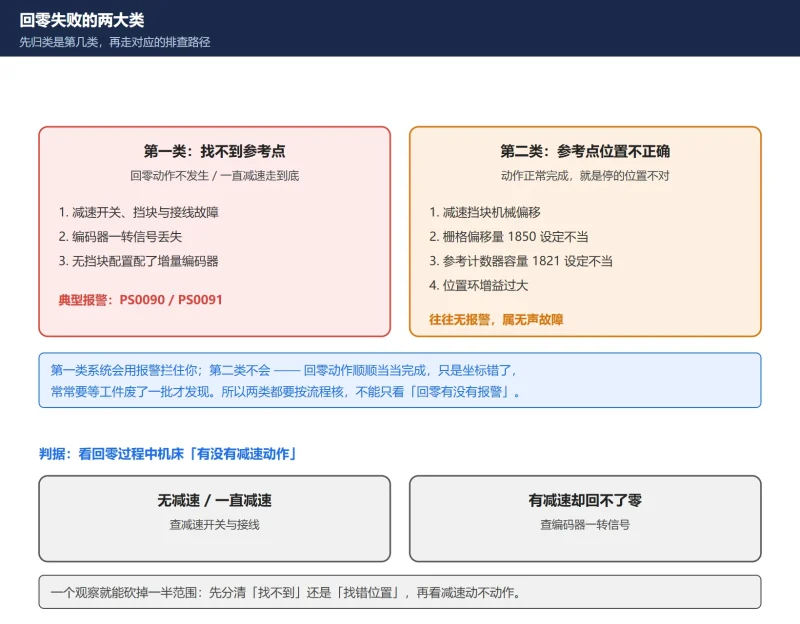
How to Classify and Troubleshoot CNC Homing Failures: Reference Not Found vs Wrong Reference Position + Decel Dog / One-Turn Signal + Grid Shift 1850 / Reference Counter 1821 + Absolute Encoder Battery
Stop swapping parts to see what sticks. Split homing failures into two classes: reference not found, and reference position wrong. In the first class, watch whether the axis decele...
昨天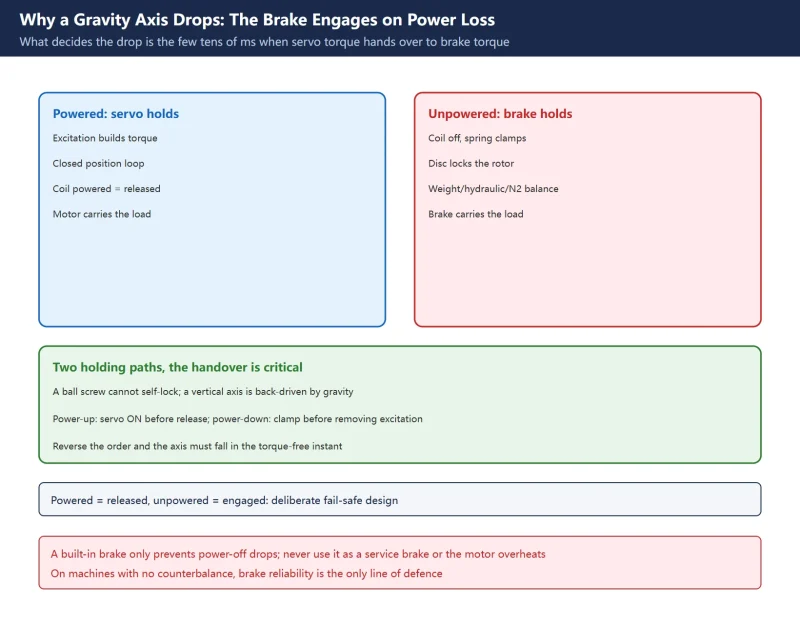
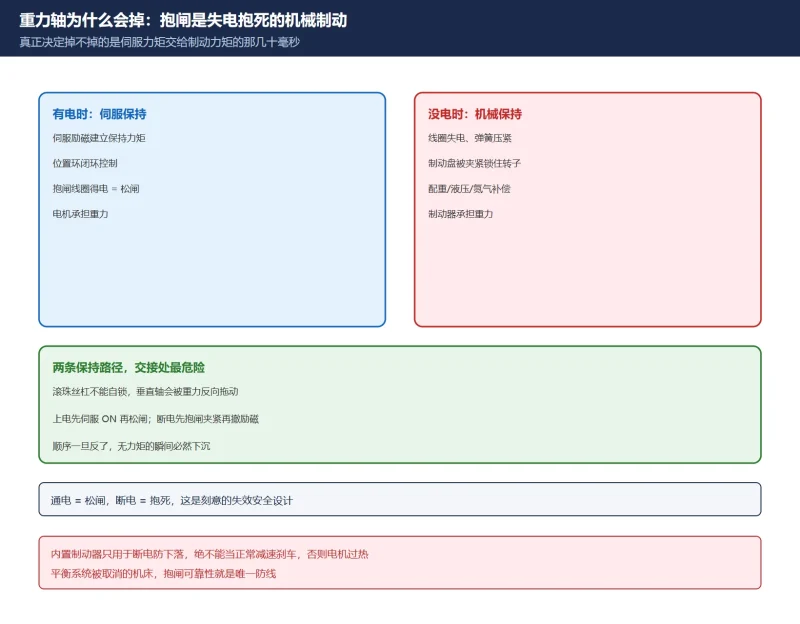
Fanuc Gravity-Axis Brake: Release Sequence, 24V Wiring and Diagnosing Z-Axis Drop
A Z axis that drops on E-stop or power loss is not simply a bad brake. Based on FANUC B-65162E/03-10: power-off engaged brake, power-up/down sequence, dedicated 24V circuit, BRKC, ...
昨天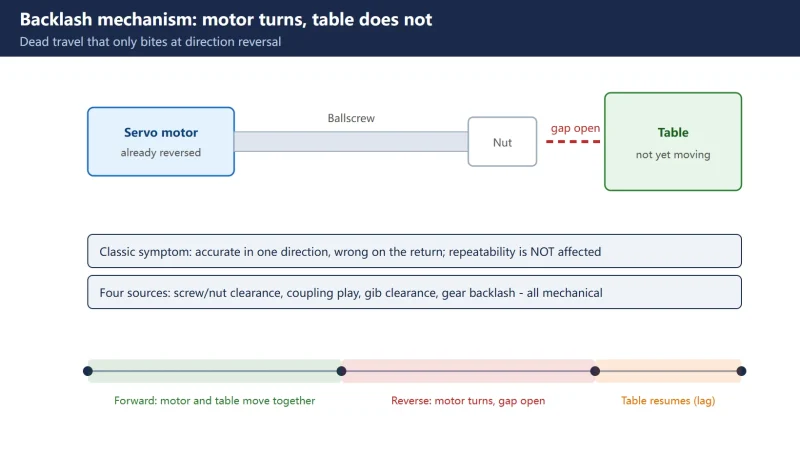
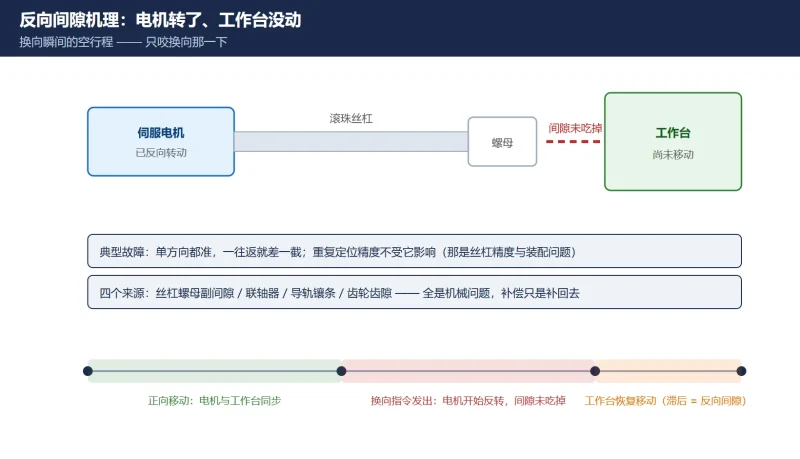
Fanuc Backlash Compensation 1851: Measure, Convert to Detection Units, Write and Verify
The complete FANUC backlash compensation procedure: measure with a dial indicator at cutting feed and rapid, convert to detection units (0.020 mm becomes 20; lathe X axis times 2),...
昨天






扫一扫,添加我的微信










