










最新发布第30页
排序
FANUC Alarm Code List: P/S Alarms 2032–5110 Explained (Part 5)
English reference for FANUC P/S alarm numbers 2032 to 5110: Ethernet and data server errors, P-CODE macros, peripheral axis control, sheet-metal and punch-press cycles, nibbling, a...

 21天前
FANUC 反向间隙补偿 1851 怎么设?千分表实测 → 检测单位换算 → 写入 → 双向验证的完整流程
FANUC 反向间隙补偿 1851 完整流程:千分表实测(切削 G01 与快速 G00 各一次)、检测单位换算表(0.020mm→20、车床 X 轴×2、英寸机床)、1851/1852 与 1800#4/1817#2 参数落位、PWE 写入与断...
昨天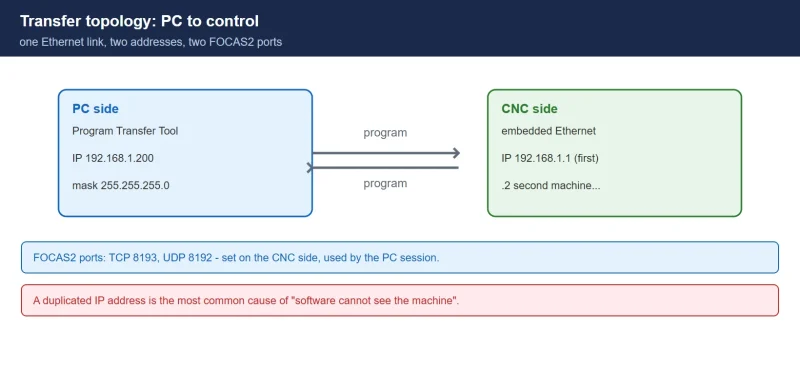
FANUC Program Transfer Tool V18: Ethernet Setup and Program Transfer
How to install FANUC Program Transfer Tool V18 and move part programs over Ethernet: supported controls, IP planning, CNC-side FOCAS2 settings, session setup and the drag-and-drop ...
21天前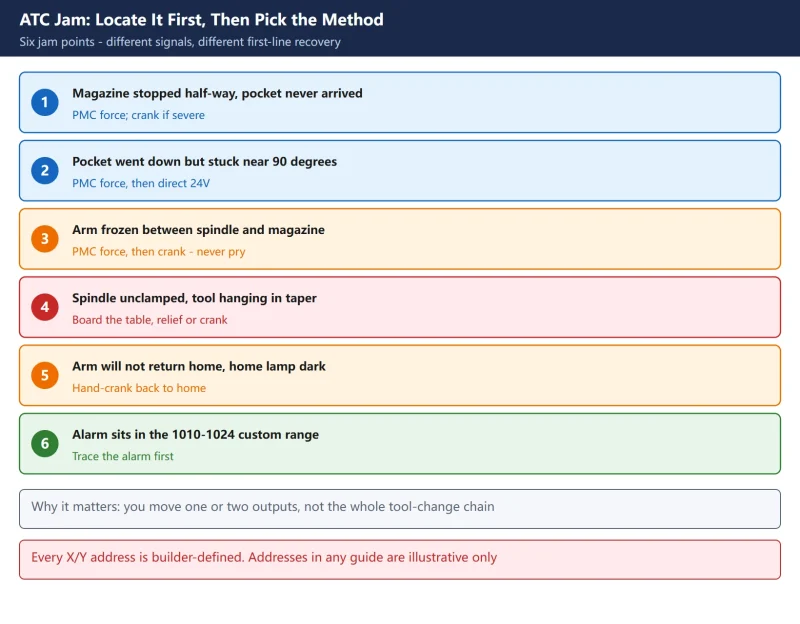
Fanuc Tool Change Stuck: 4 Manual Fixes for a Jammed ATC Arm
Recovery actions for an already-jammed tool change, not a diagnostic procedure. Locate the jam among six possible points, then escalate by intervention depth: PMC force output (sta...
昨天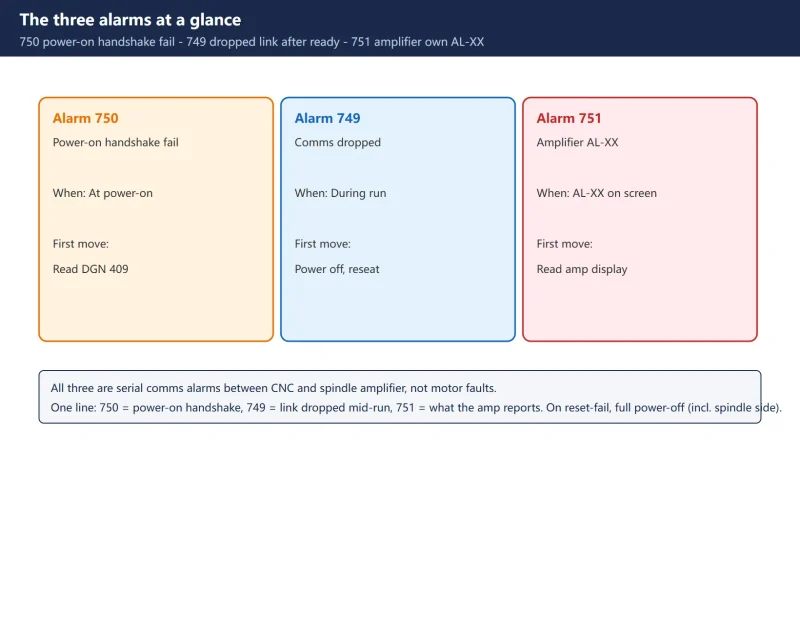
FANUC Serial Spindle Alarms 749/750/751: Split by Timing, then DGN 409 and Amp Display
749, 750 and 751 are all serial communication alarms between the CNC and the spindle amplifier - not motor faults. 750 is a failed power-on handshake, 749 a dropped link after read...
20天前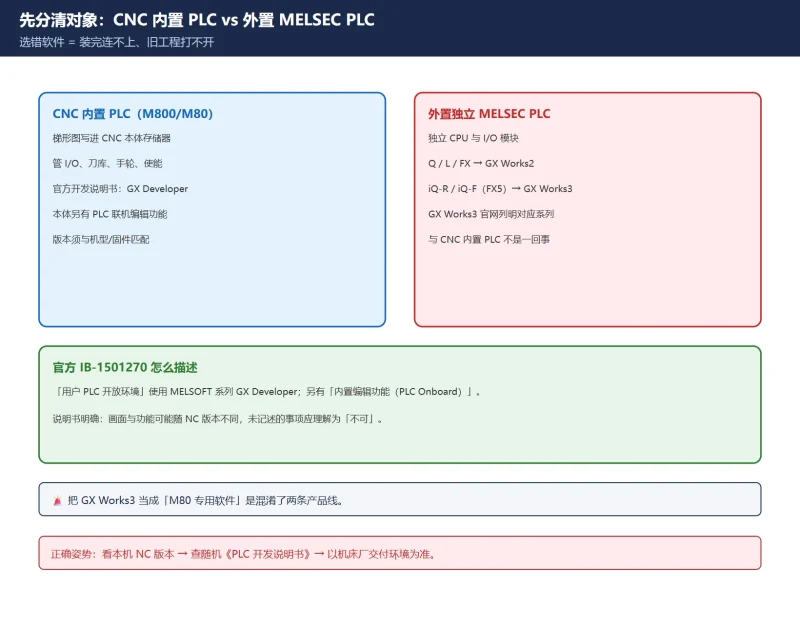
三菱 M80 PLC 编程软件用哪个?GX Works3 / GX Developer 官方下载路径 + 版本对应表 + 安装与连机常见坑
先分清「CNC 内置 PLC」和「外置 MELSEC PLC」,再选软件。三菱官方 M800/M80《PLC 开发说明书》(IB-1501270)写明的用户 PLC 开发环境是 MELSOFT 的 GX Developer;GX Works3 官网标明对应 ME...
前天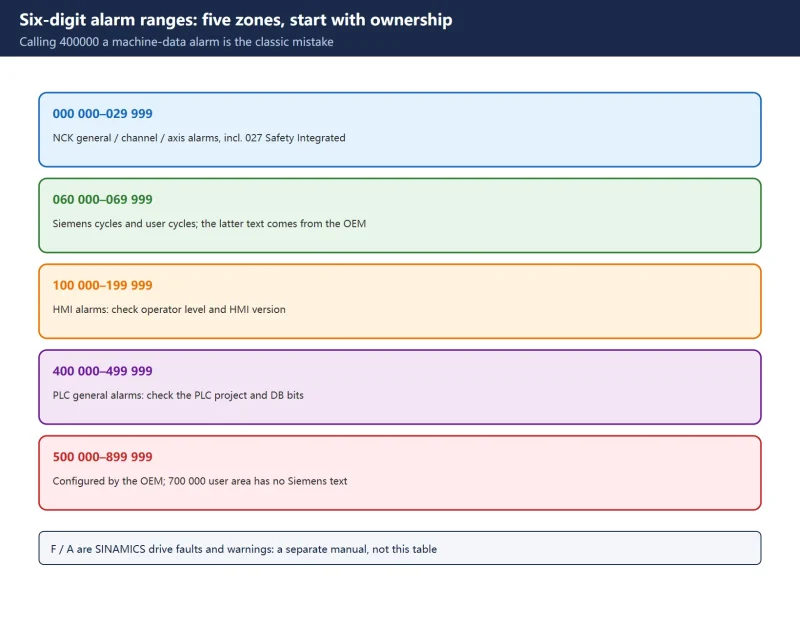
SINUMERIK 840D sl Alarm Code Quick Reference: Number Ranges, Reactions and Manual Index
840D sl alarms are six-digit numbers; the full per-number text lives only in the official Siemens diagnostics manual. This page gives the number ranges, CN/EN reaction terms, how t...
4天前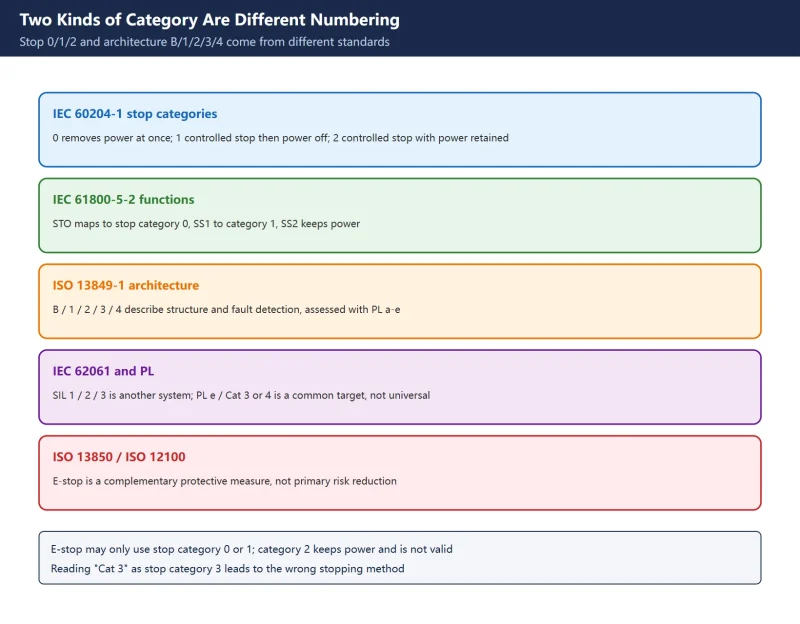
Machine Safety Circuits: STO vs SS1, Stop Categories, PL / SIL, Dual Channels and EDM
A circulating brief attributes Cat0 / Cat1 / Cat2 / Cat3 to ISO 13849. That merges two different meanings of category: stop categories 0/1/2 come from IEC 60204-1, architecture cat...
前天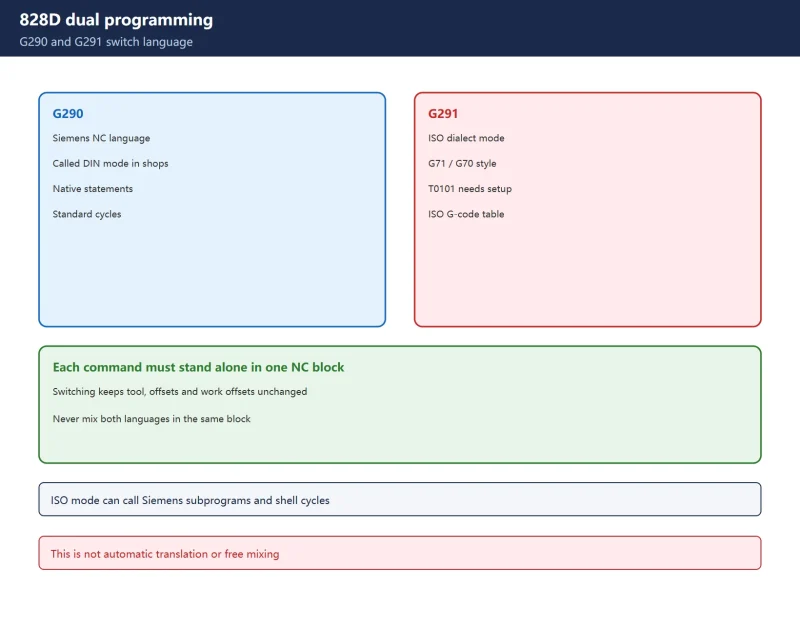
SINUMERIK 828D G290 vs G291: DIN and ISO Mode Side by Side
Siemens' own manual says G290 activates the Siemens NC programming language and G291 activates the ISO dialect. Each must stand alone in an NC block and the two languages cannot be...
4天前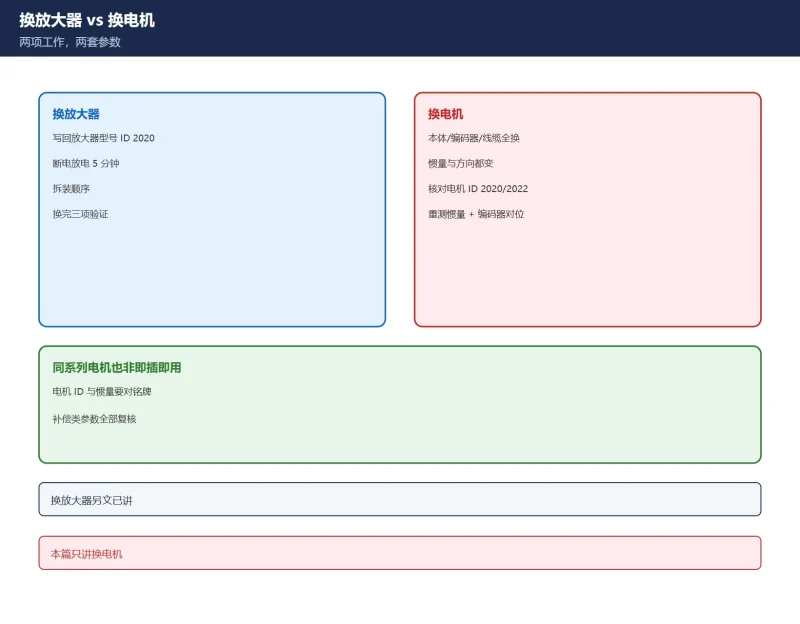
FANUC 换伺服电机后参数怎么回写?2020 / 2022 / 2021 + 惯量比重测 + 编码器方向与对位 + 三步验收
FANUC 换伺服电机全解:先分清换放大器与换电机,给出电机侧参数纠错(2021 惯量比、2023 速度脉冲数、1825 位置环增益,非网传的 2023/2083),惯量比重测三法、编码器对位、机械电气侧检查、...
昨天






扫一扫,添加我的微信










