最新发布第24页
排序
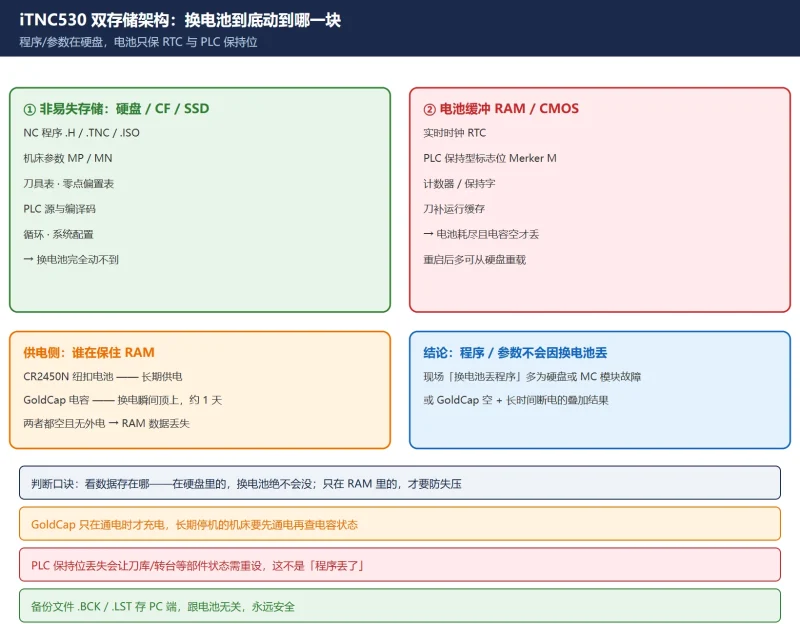
海德汉换电池会丢程序吗?iTNC530/TNC640/TNC7 到底丢什么、留什么,附 Renata CR2450N 型号与带电更换流程
换电池前最怕一句'程序会不会没'。对海德汉 iTNC530 这类控制,答案是否定的:NC 程序、机床参数、刀具表、零点偏置全在硬盘或 CF 卡里,跟那颗纽扣电池没关系。电池只保 RTC、PLC 保持位和刀补...

 昨天
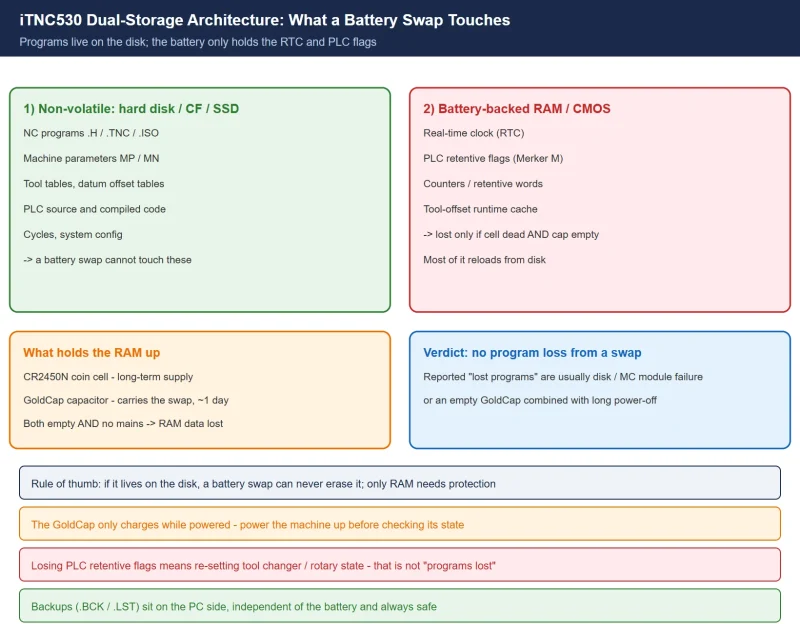
Will Changing the HEIDENHAIN Battery Erase Your Programs? iTNC530 / TNC640 / TNC7 — What Is Lost, What Is Kept, Renata CR2450N and the Live-Swap Steps
The fear before every battery swap: will the programs be gone? On HEIDENHAIN controls like the iTNC530 the answer is no — NC programs, machine parameters, tool tables and datum of...
昨天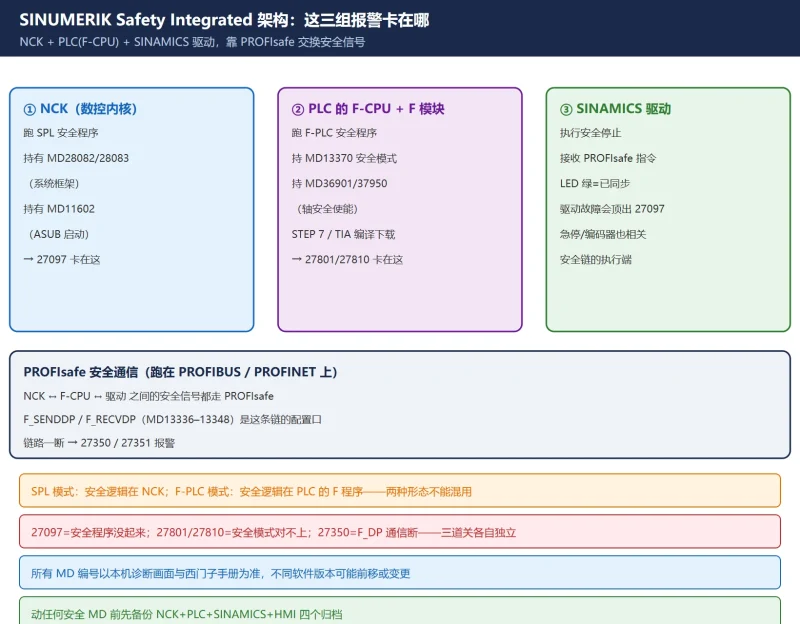
840D sl 安全集成报警 27097/27801/27810/27350 怎么查:SPL 启动、安全模式、F_DP 通信与对应机床数据
840D sl 的 SINUMERIK Safety Integrated 报警 27097(SPL 启动未执行)、27801/27810(安全模式与 PLC 配置不一致)、27350/27351(F_DP 通信错误)怎么查。逐一对应机床数据 MD28082/28083/11...
昨天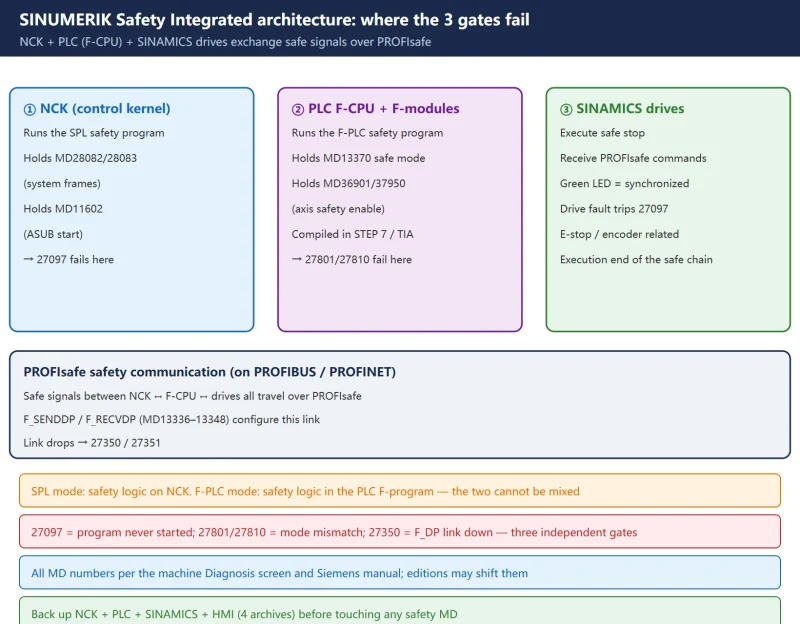
840D sl Safety Integrated Alarms 27097 / 27801 / 27810 / 27350 — SPL Start, Safe Mode Mismatch, F_DP Communication (with Machine Data)
How to diagnose SINUMERIK 840D sl Safety Integrated alarms 27097 (SPL not started), 27801/27810 (safe operating mode vs PLC config mismatch), and 27350/27351 (F_DP communication er...
昨天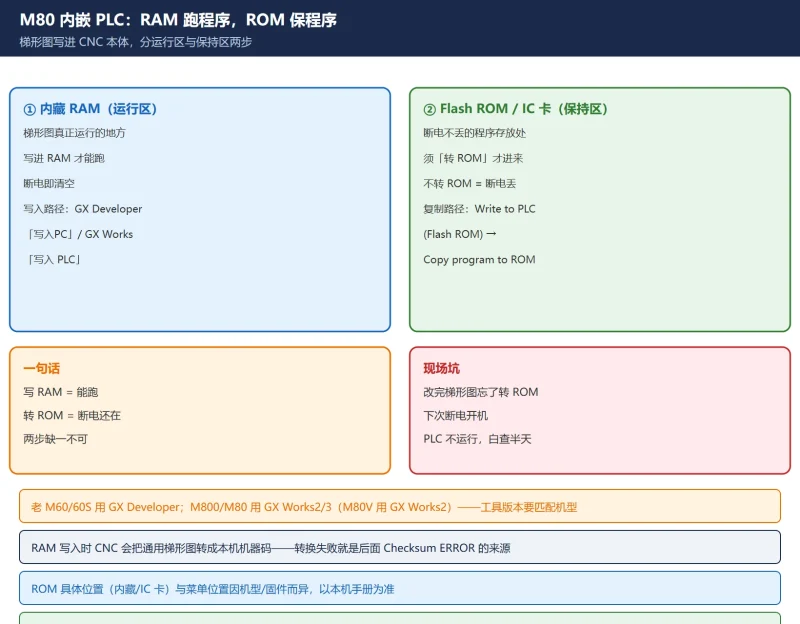
三菱 M80 梯形图怎么写进 CNC?GX Developer 写 RAM、转 ROM 与 Checksum ERROR 排查
三菱 M80 / M800 的梯形图(内嵌 PLC 序列程序)怎么写进 CNC:GX Developer / GX Works2·3 写入内藏 RAM 的流程、为什么必须'转 ROM'固化、以及 Checksum ERROR 的根因(转换错误把出错步变 N...
21小时前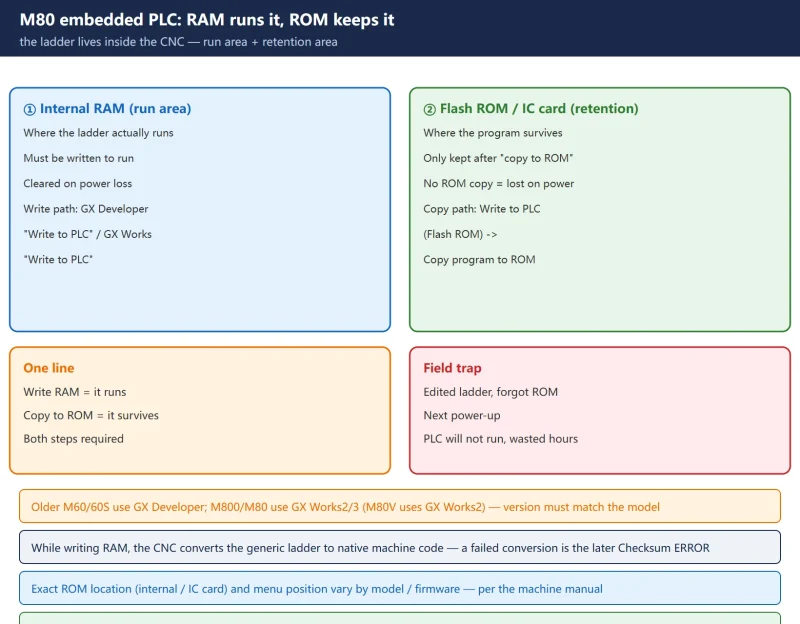
How to Write Mitsubishi M80 Ladder Logic into the CNC — RAM Write, ROM Copy and Checksum ERROR
How to write the Mitsubishi M80 / M800 ladder logic (the embedded PLC sequence program) into the CNC — the GX Developer / GX Works2·3 RAM write flow, why you must 'copy to ROM', ...
21小时前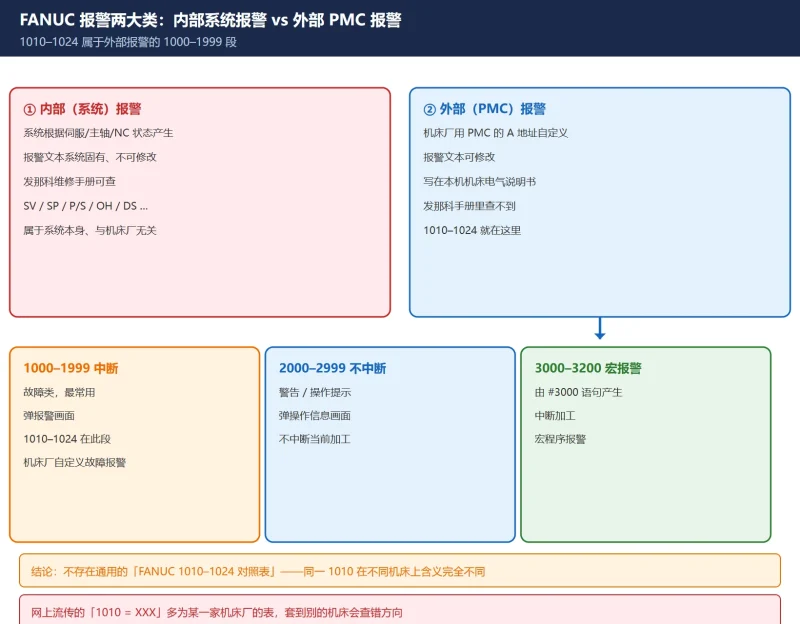
FANUC ATC 报警 1010–1024 速查:机床厂自定义报警的反查方法与真实对照
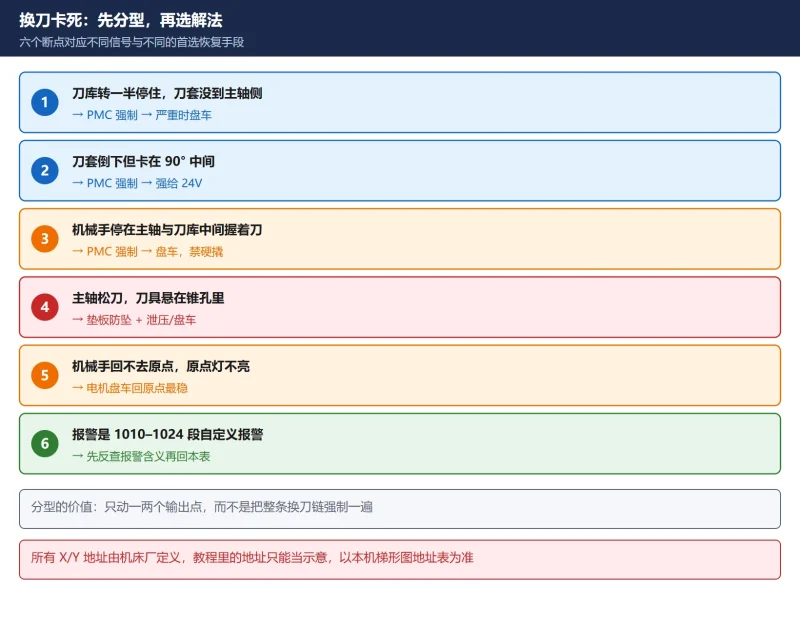
加工中心刀库/ATC 报警 1010–1024 为什么在发那科原厂手册里查不到?因为它们是机床厂用 PMC 的 A 地址自定义的外部报警。本文给出报警号段划分、A 地址映射、四步反查法,以及四个真实机床厂...
昨天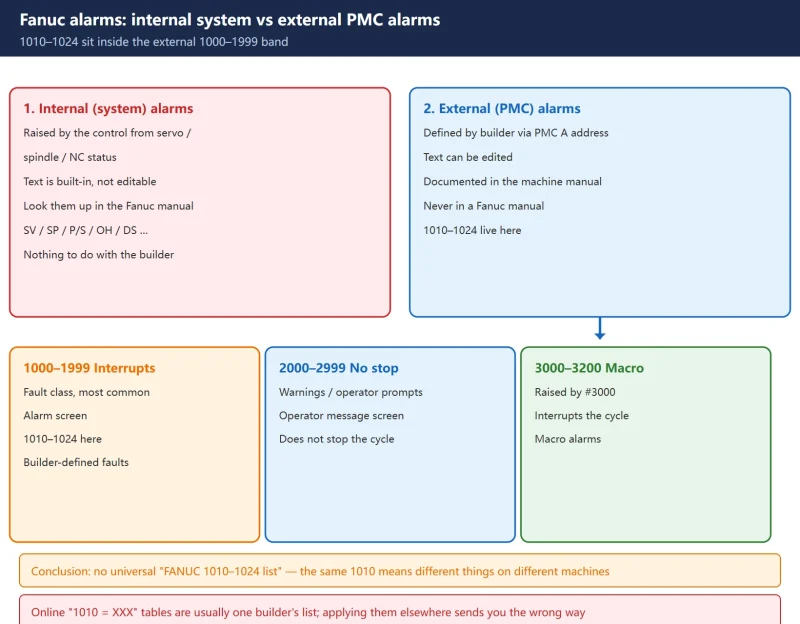
FANUC ATC Alarms 1010–1024 — Why They Are Not in the Fanuc Manual, and How to Trace Them
Why tool changer / ATC alarms 1010–1024 cannot be found in any Fanuc manual: they are machine-tool-builder external alarms driven by PMC A addresses. This guide covers the alarm n...
昨天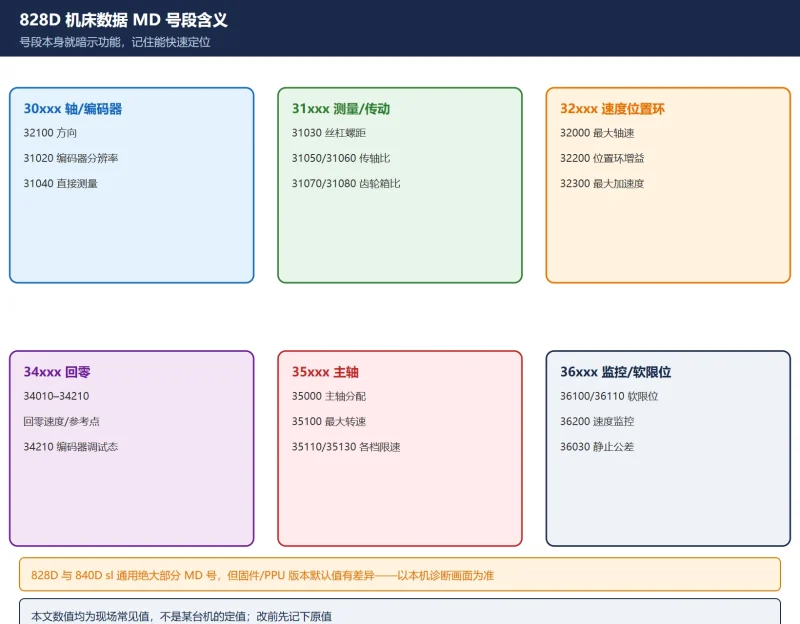
西门子 828D 常用机床数据 MD 速查:轴 / 主轴 / 回零 / 软限位分组对照
西门子 828D 调试现场最常改的机床数据(MD)按功能分组对照:轴基本配置 32100/31020/31030/31040/31050/31060、速度加速度与加加速度 32000/32010/32020/32200/32300/32431、主轴 35000/35010...
昨天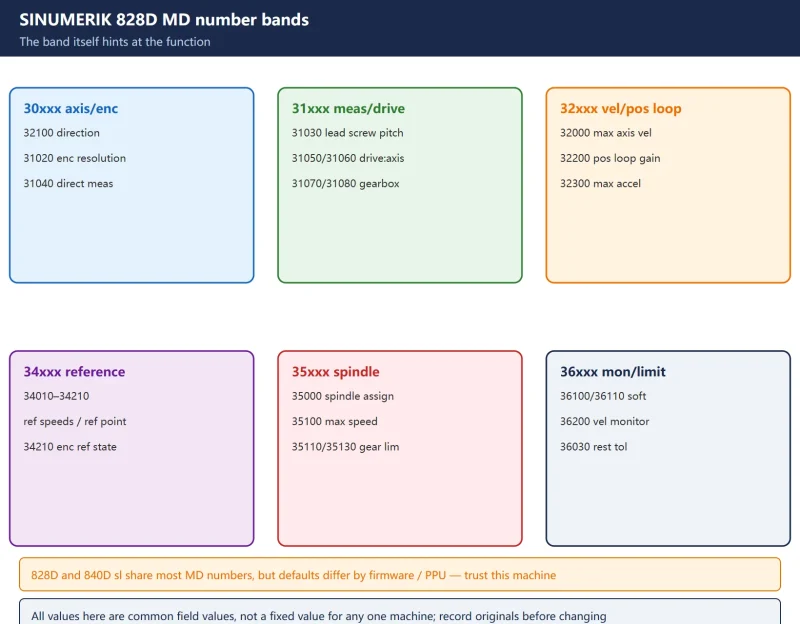
SINUMERIK 828D Common Machine Data (MD) Quick Reference — Axis / Spindle / Referencing / Soft Limits
The machine data (MD) most often changed when commissioning a SINUMERIK 828D, grouped by function: axis setup 32100/31020/31030/31040/31050/31060, velocity/acceleration/jerk 32000/...
昨天




扫一扫,添加我的微信