
最新发布第21页
排序
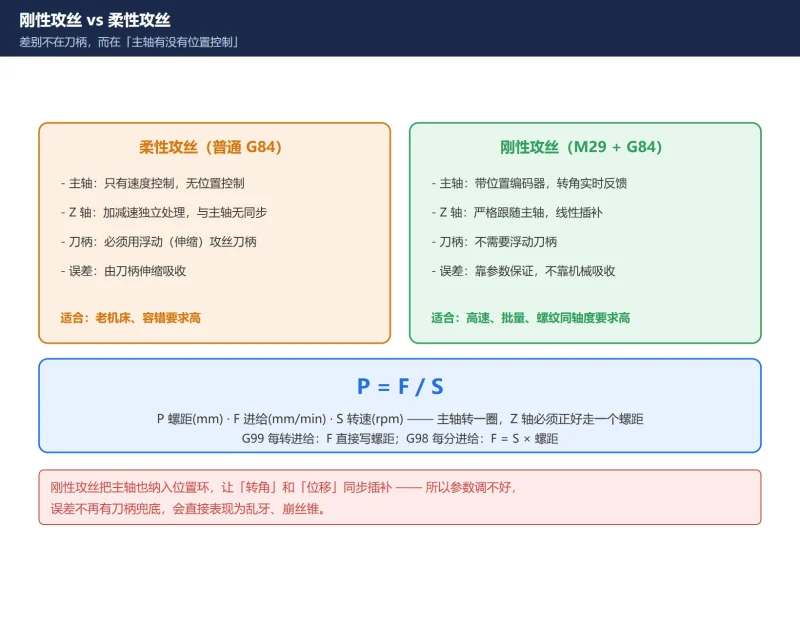
FANUC 刚性攻丝参数全解:M29/G84 同步原理 + 5200–5294 参数链 + SP0741 报警怎么排(附诊断号 452/453 读法)
刚性攻丝调不好的根子,多半不是编程而是参数。本文把 5200–5294 按五类拆开讲:开关位决定走不走刚性攻丝、齿轮比 5221–5224/5231–5234 决定比例、转速上限是 5241–5244(不是 5200)、增...

 昨天
“瞪眼法”解决FANUC机床故障分类以及解决方向
一文掌握“瞪眼法”排查FANUC数控机床故障的完整流程:从黑屏、PMC报警到硬件/软件根源,结合真实案例图解,教你3分钟判断故障类型并给出更换、维修、参数修改等解决方向,维修效率翻倍。
昨天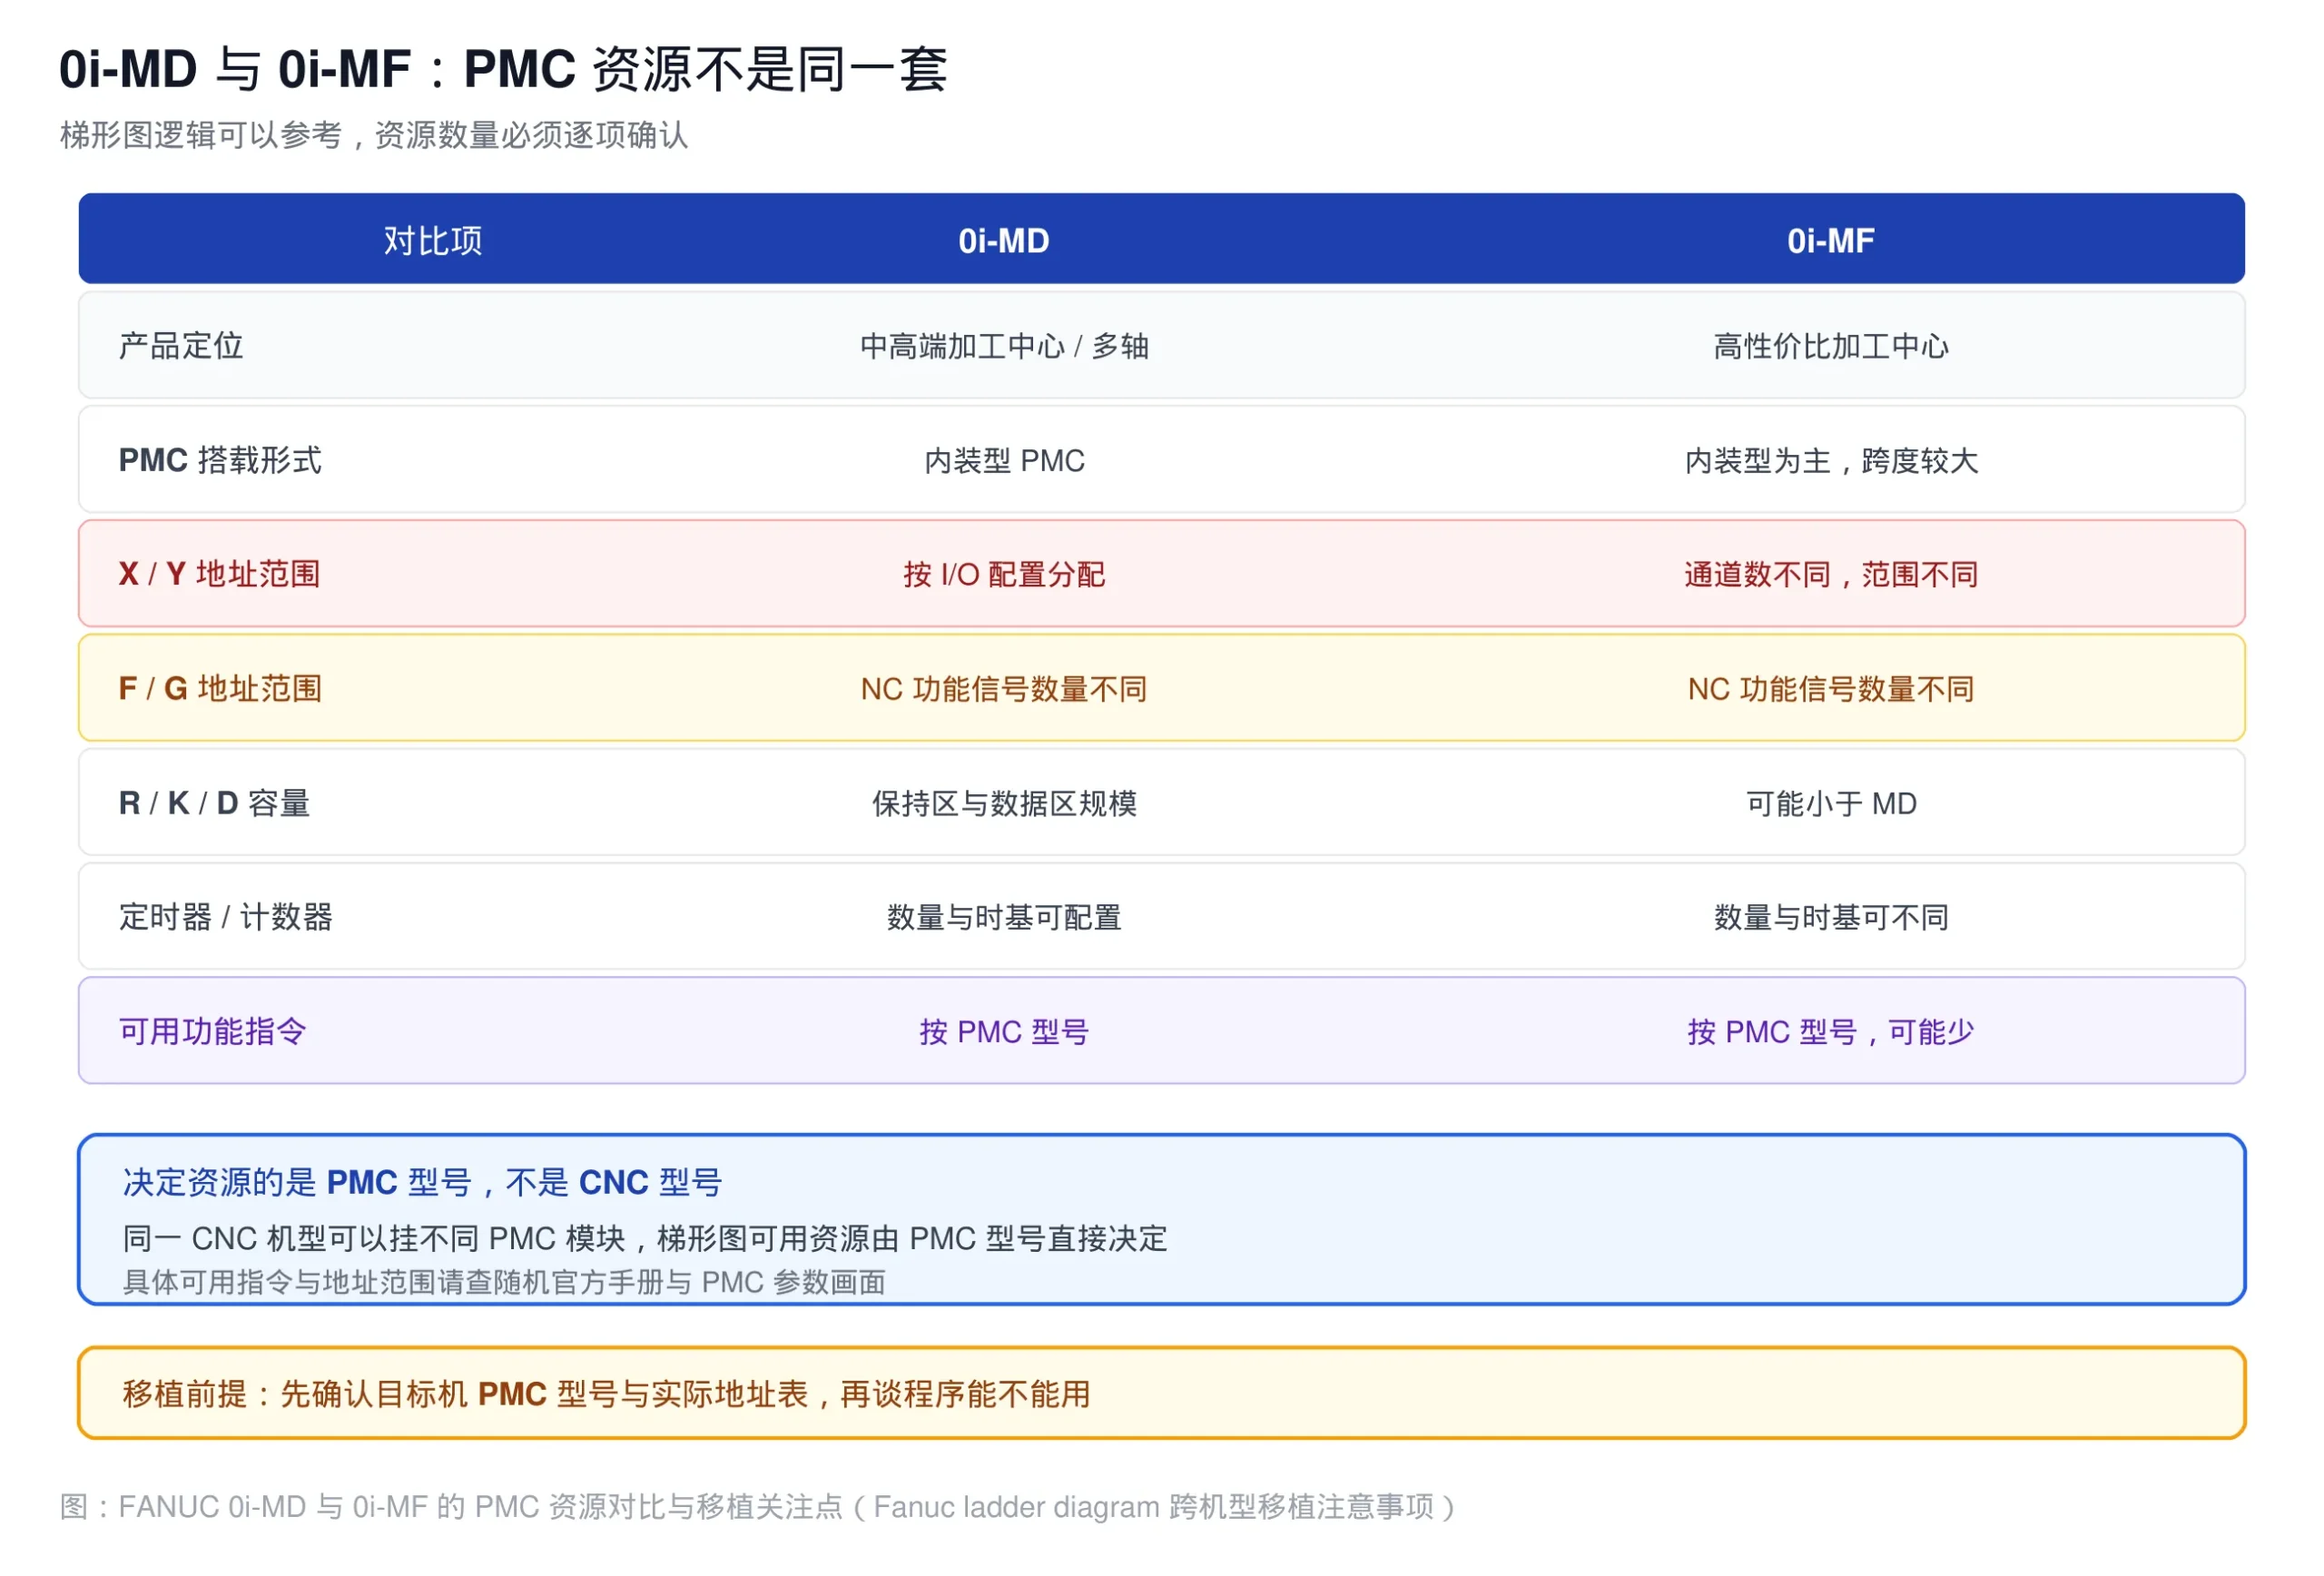
FANUC 0i-MD / 0i-MF PMC 差异对比:地址数量、机型限制与移植注意事项
一句话答案:FANUC 0i-MD 与 0i-MF 同属 0i 系列但 PMC 平台不同,搭载的 PMC 容量、指令集与 X/Y 等地址范围有差异,梯形图逻辑可参考但资源不能假定一致;跨机型移植要先做地址表核对、四步走...
昨天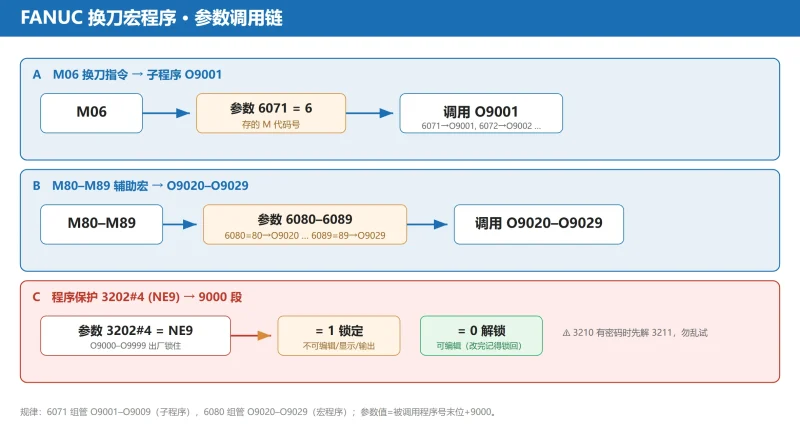
FANUC 换刀宏程序(O9001)编写与恢复:参数 6071/6080 调用关系、3202#4 NE9 解锁与 G54.x 接口信号
FANUC 加工中心换刀宏程序 O9001 编写与恢复:讲透参数 6071→子程序、6080–6089→宏程序、3202#4(NE9) 解锁 9000 段,G54.x 与 #1000 接口变量映射、模态保护与加装刀库避坑。
昨天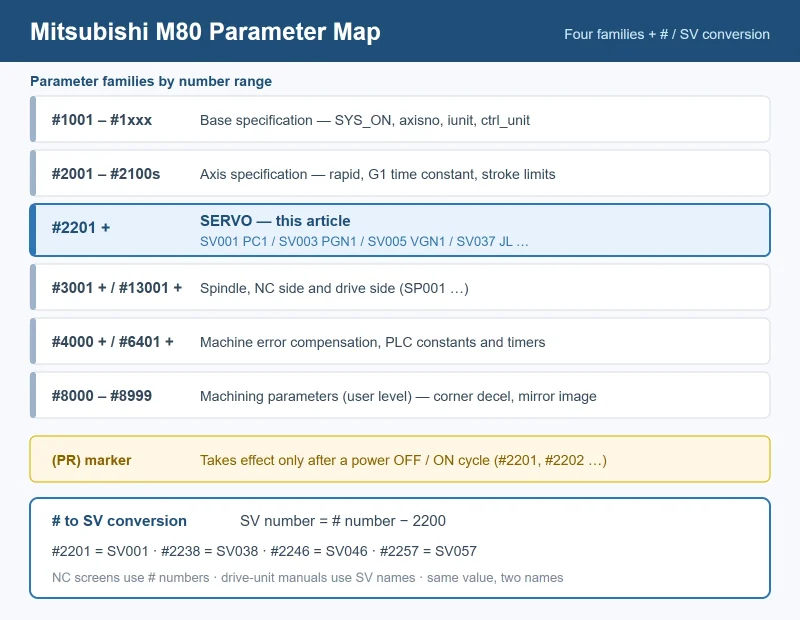
Mitsubishi M80/M70 Servo Parameters: #2201-#2210 Full Table, #2233/#2238/#2246 Resonance Filters, #2235/#2237 Load Inertia Setup
Mitsubishi M80/M70 servo parameter reference: the complete #2201-#2210 block (PC1/PC2 gear ratio, PGN1 position loop, VGN1 speed loop), #2233/#2238/#2246 notch filter setup, #2235 ...
昨天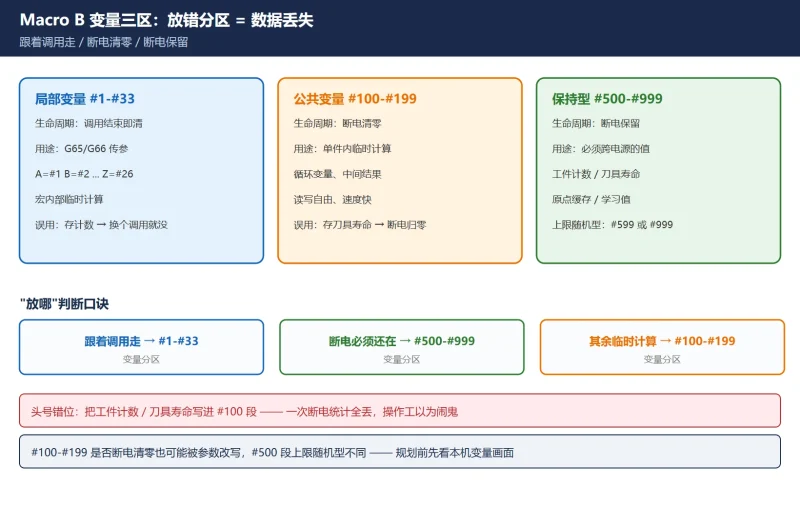
FANUC 宏程序(Macro B)教程:变量分区怎么选、G65/G66/G67 怎么用、嵌套上限与 PS 报警对照
FANUC 宏程序(Macro B)系统教程:变量三区怎么选(#1-#33 局部随调用清空、#100-#199 断电清零、#500-#999 保持型——工件计数与刀具寿命必须放 #500 段)、空值陷阱(没赋值的变量是 null 不...
昨天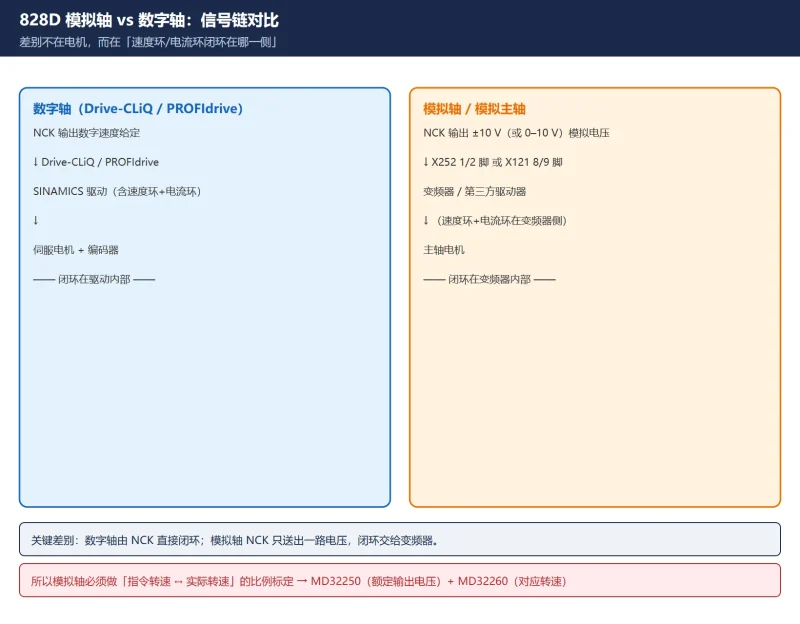
西门子 828D 模拟主轴 / 模拟轴怎么配置:MD30100–31050 参数组 + X252 接线 + MD32250/32260 量程标定
828D 接变频器 / 模拟驱动时,要把轴配成「模拟轴(模拟量给定输出)」而不是数字轴。本文给出 MD30100 / 30110 / 30120 / 30130 / 30134 与 MD30200 / 30220 / 30230 / 30240 的取值口径,X252...
昨天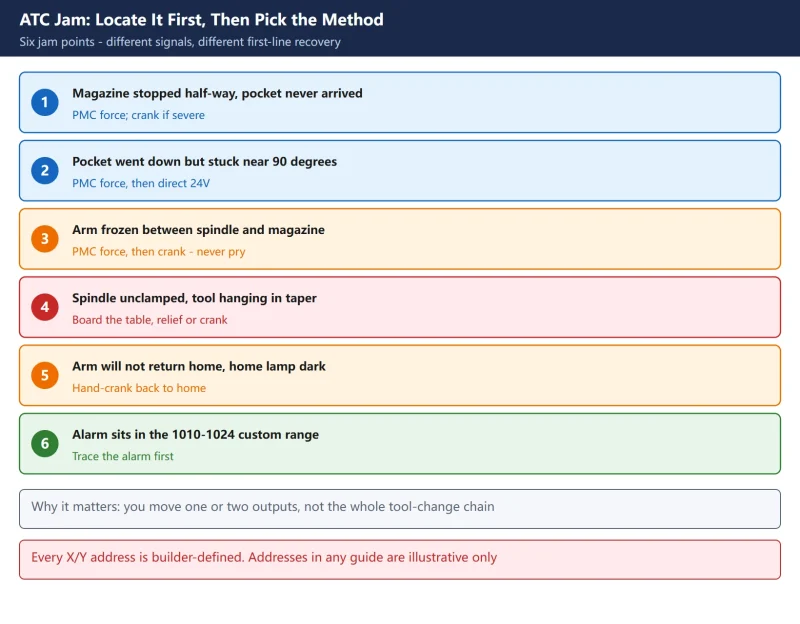
Fanuc Tool Change Stuck: Four Manual Recovery Methods for a Jammed ATC Arm (PMC Force Output, Direct 24V to the Solenoid, Pressure Relief, Motor Hand-Crank)
Recovery actions for an already-jammed tool change, not a diagnostic procedure. Locate the jam among six possible points, then escalate by intervention depth: PMC force output (sta...
昨天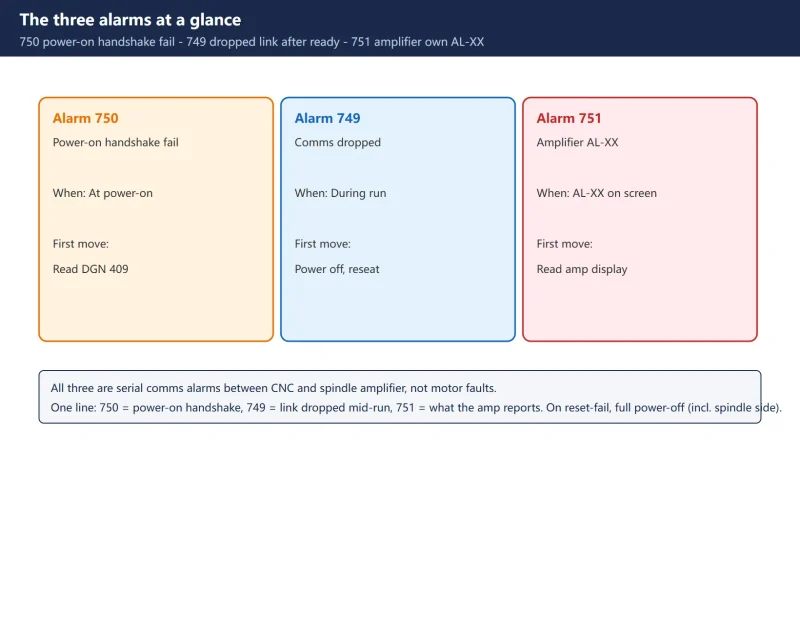
FANUC Serial Spindle Alarms 749/750/751: Split by Timing, then DGN 409 and Amp Display
749, 750 and 751 are all serial communication alarms between the CNC and the spindle amplifier - not motor faults. 750 is a failed power-on handshake, 749 a dropped link after read...
23小时前




扫一扫,添加我的微信