

最新发布第22页
排序
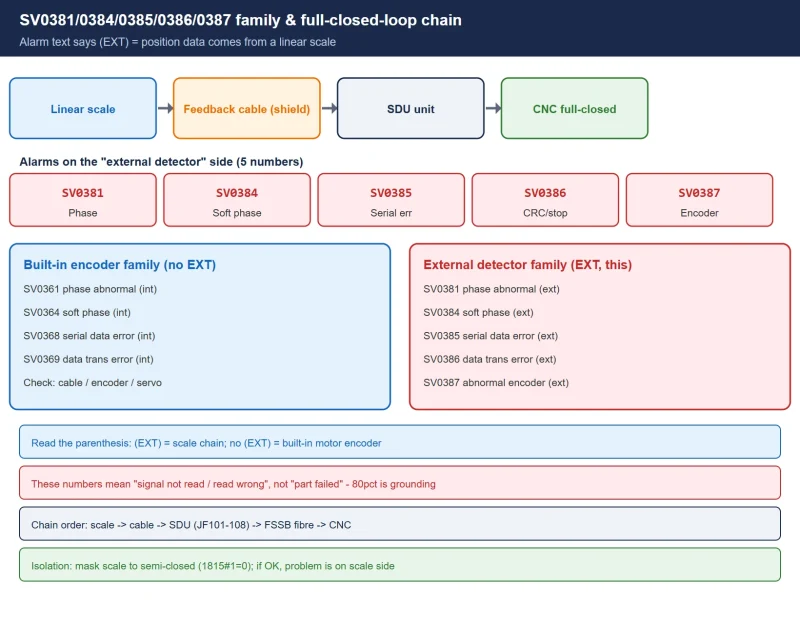
FANUC SV0381/0384/0385/0386/0387 Servo Alarms: Poor Grounding and the Linear Scale (EXT) Alarm Family
On a full-closed-loop machine SV0381/0384/0385/0386/0387 often trip alternately or keep repeating on one axis, easily misread as a broken scale or amplifier. These alarms all say '...

 昨天
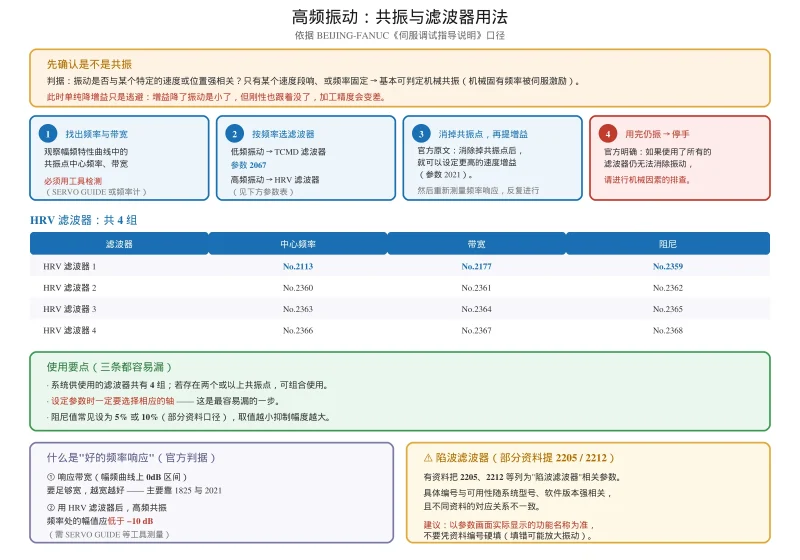
数控机床伺服振动、过冲、异响怎么调?现象分类排查表与波形判读
伺服振动现象分类排查教程:高频啸叫、低频颤振、起停过冲、加工振纹四类方向完全不同,含 HRV 滤波器四组参数表与共振消除流程、象限凸起的两面性判据、2048 反向间隙加速调整、HRV 控制作用与...
昨天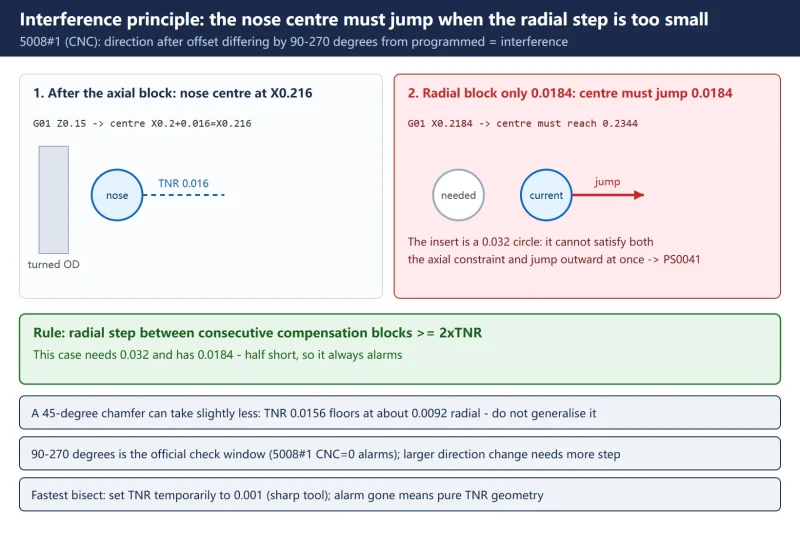
Fanuc G41/G42 Interference Alarm: The 2×TNR Minimum Radial Step Rule Explained
The complete FANUC G41/G42 interference alarm (PS0041 / PS0325) guide: the 2×TNR minimum radial step rule with the 0.0156 inch / 0.0092 inch worked case, the TNR matrix, five caus...
昨天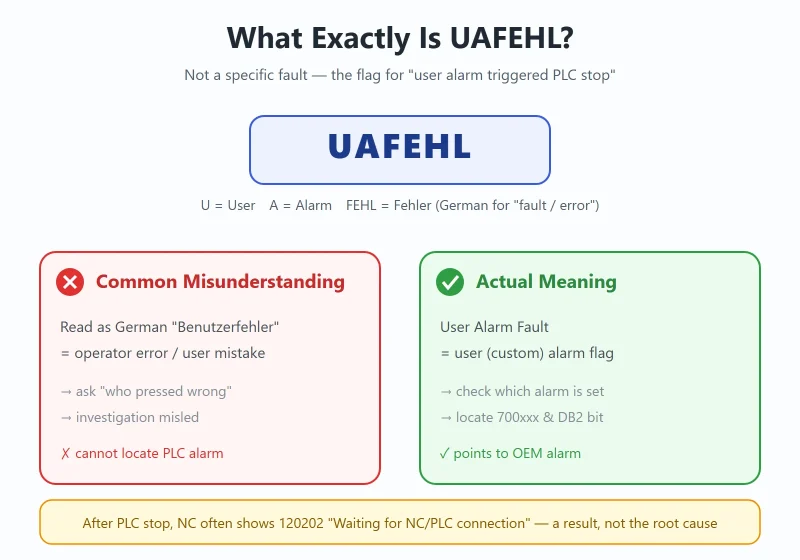
SINUMERIK 840D/828D UAFEHL Alarm: What It Means, Why the PLC Stops, and How to Localize It via DB2
UAFEHL is not a specific fault — it is the SINUMERIK flag for 'a user alarm triggered the PLC stop.' Six root-cause families, a 5-step localization procedure, SF/STOP/RUN LED mean...
昨天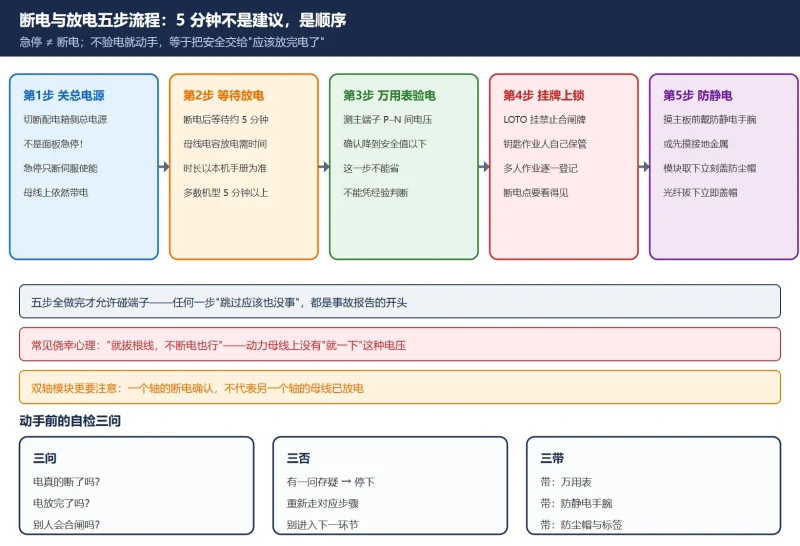
FANUC 伺服放大器更换实操:断电放电 5 分钟、拆装顺序、电机 ID 与参数写回、换完必做的三项验证
FANUC 伺服放大器更换实操:从该不该换的决策、断电放电 5 分钟与验电挂牌、拆装顺序(先标记再拔线后拆螺丝)、电机 ID No.2020 与初始化位 No.2000#1 参数写回、FSSB 自动设定,到换完必做的...
昨天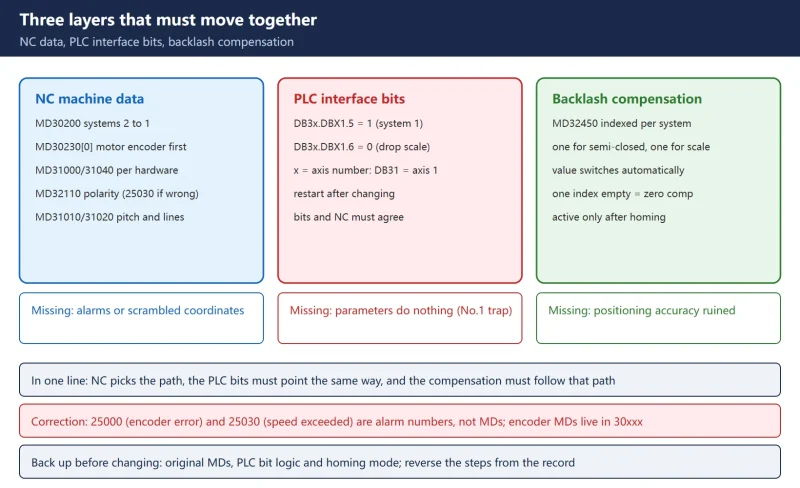
SINUMERIK 828D Semi-Closed Loop Conversion: MD Parameters, PLC Bits and Gap Compensation
A complete SINUMERIK 828D semi-closed loop conversion guide for masking a faulty linear scale: the three layers that must move together — NC machine data (MD30200 number of measur...
昨天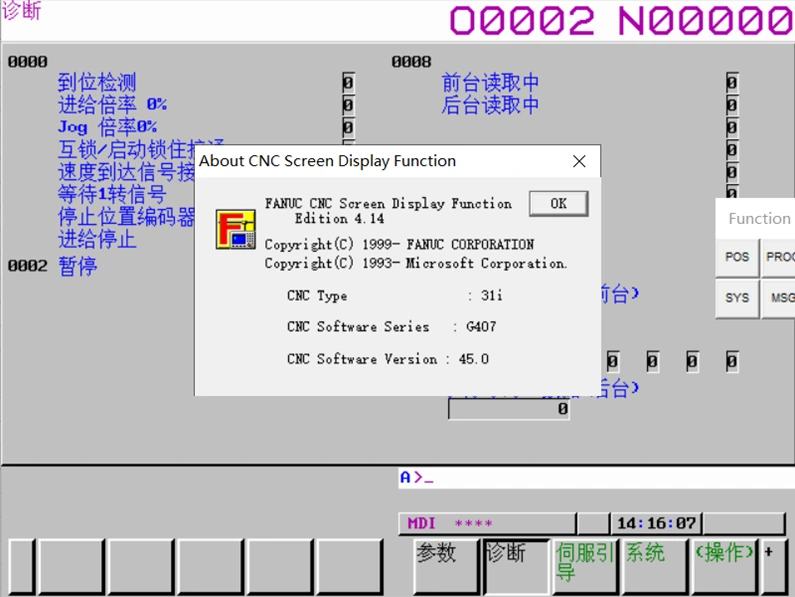
FANUC CNC Screen Display 连接31IB PLUS系统操作步骤
详解 FANUC CNC Screen Display 软件连接 31i-B PLUS 及 MF PLUS 系统的完整流程。包含电脑与系统IP网段设置、FOCAS端口配置及远程监控调试技巧。工程师必备的以太网连接实战手册,助您快速实现...
昨天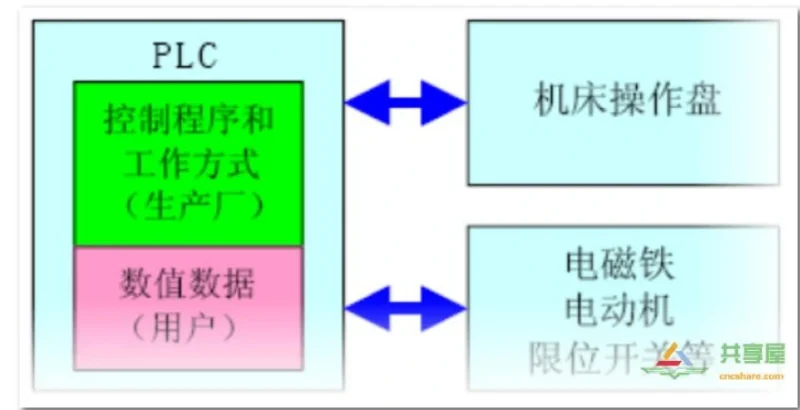
零基础学习发那科PMC视频教程全攻略 | 从看不懂梯形图到独立调试
本文面向零基础读者,系统介绍如何通过学习视频教程掌握发那科 PMC(可编程机床控制器)。文章说明 PMC 的定位与 X/Y/G/F/R/K 六类信号地址体系,梳理市面主流 PMC 视频教程的形态与挑选标准(...
昨天
FANUC Diagnosis Numbers (DGN) Quick Reference: 000–605 Partitioned Table with Alarm Cross-Reference
FANUC diagnosis numbers (DGN) quick reference: 100+ numbers grouped by function (000–039 execution, 200–299 servo, 300–399 position, 400–499 spindle, 500–605 overtravel/PMC), ...
昨天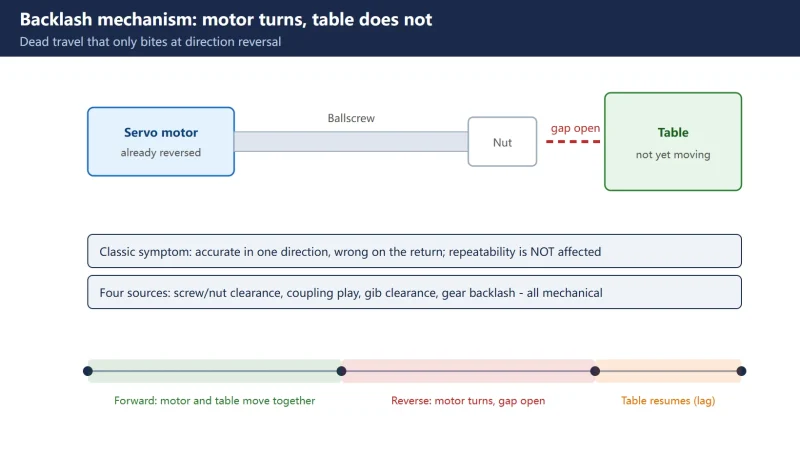
Fanuc Backlash Compensation 1851: Measure, Convert to Detection Units, Write and Verify
The complete FANUC backlash compensation procedure: measure with a dial indicator at cutting feed and rapid, convert to detection units (0.020 mm becomes 20; lathe X axis times 2),...
昨天




扫一扫,添加我的微信