


Sister article: FANUC canned-cycle quick table: address words, parameters and alarms. Related: Fanuc canned cycles explained, Fanuc rigid tapping 5200–5294, Fanuc rigid tapping parameter quick reference.
1.1 Nine-cycle master table
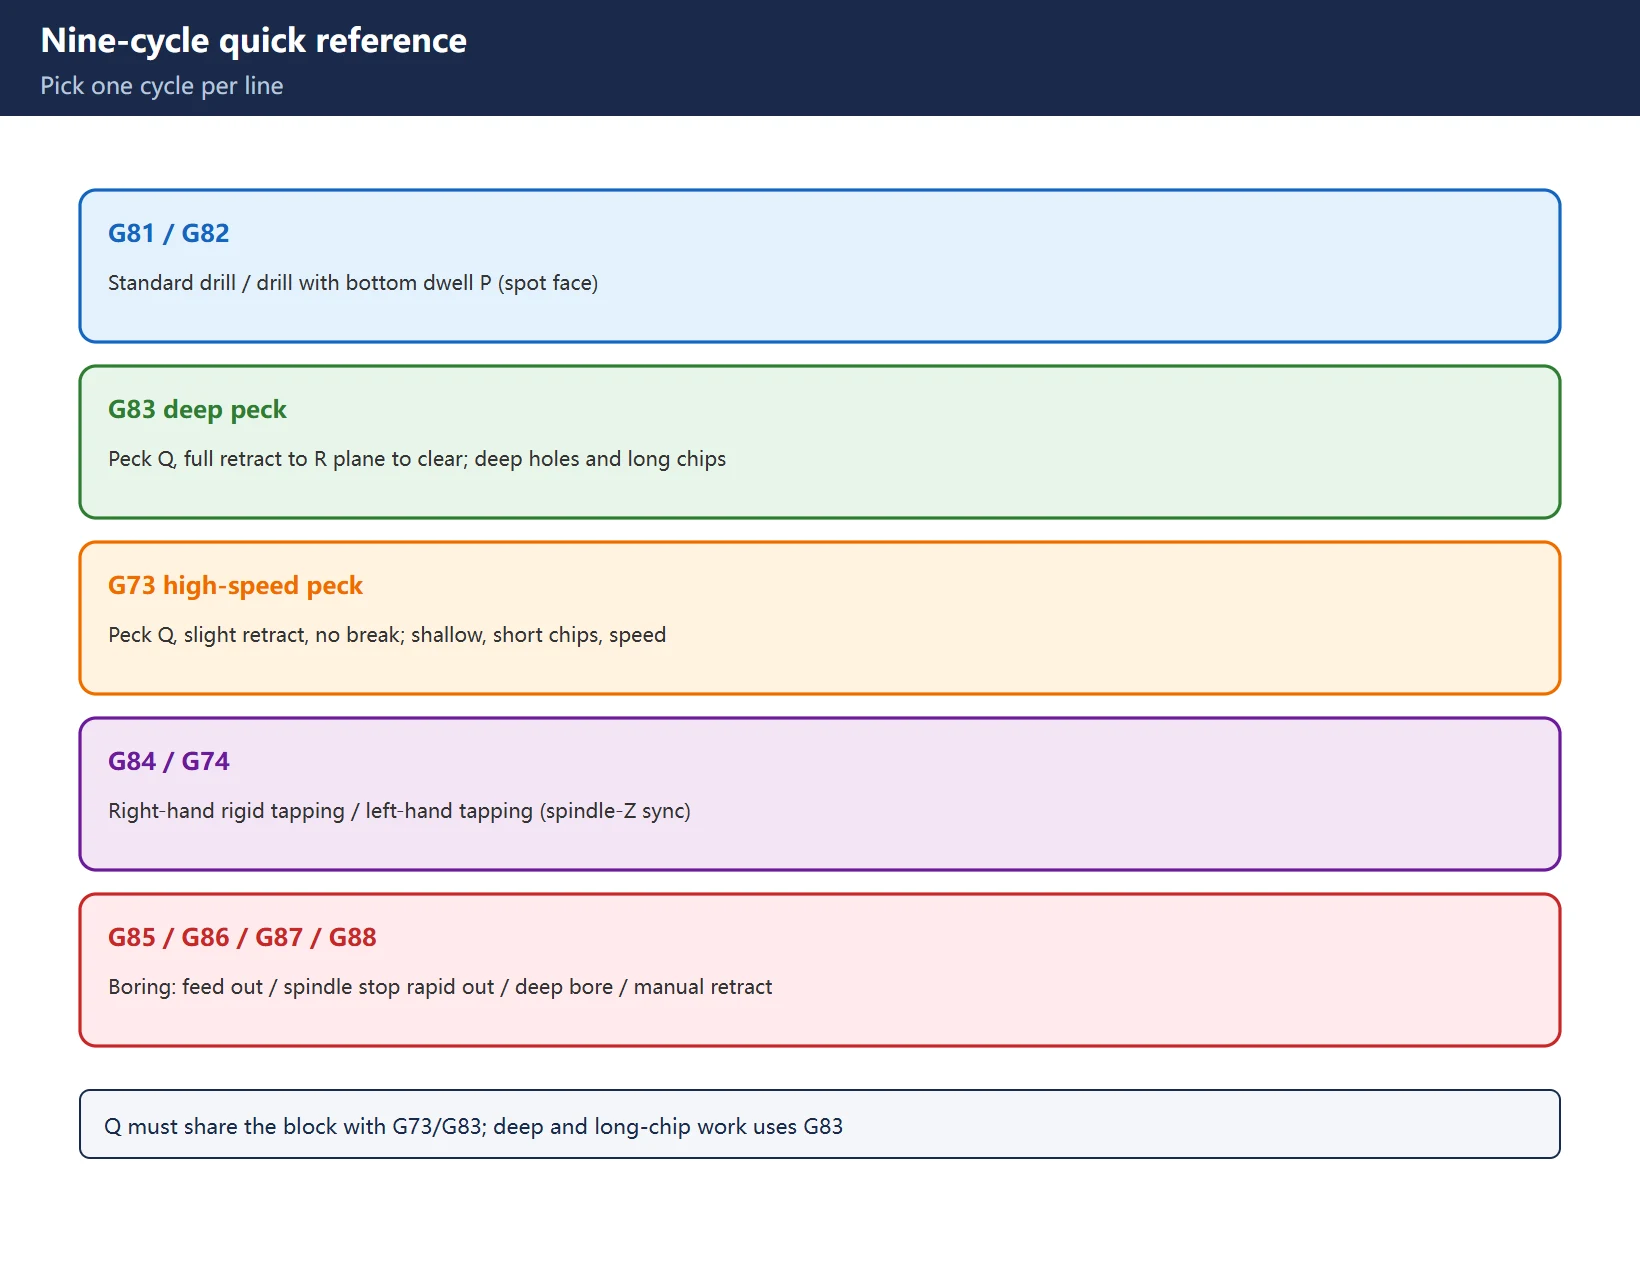
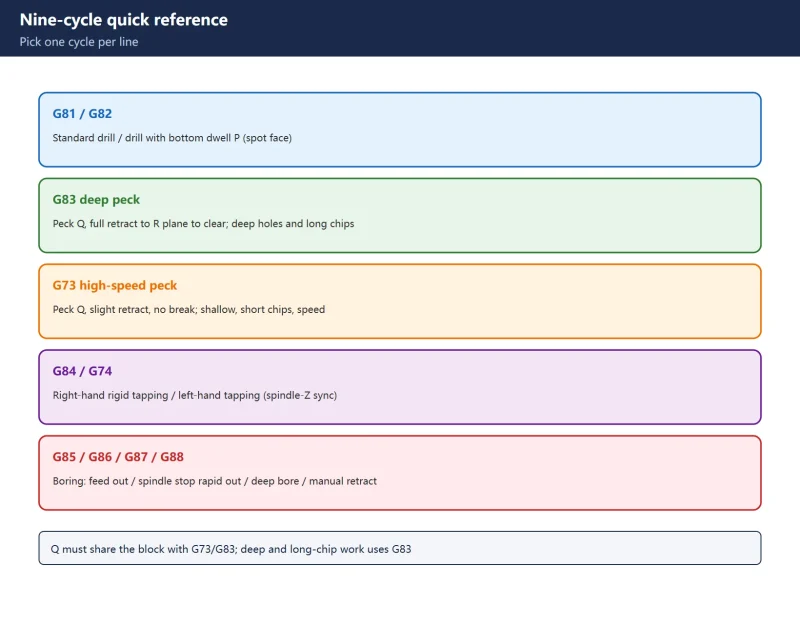
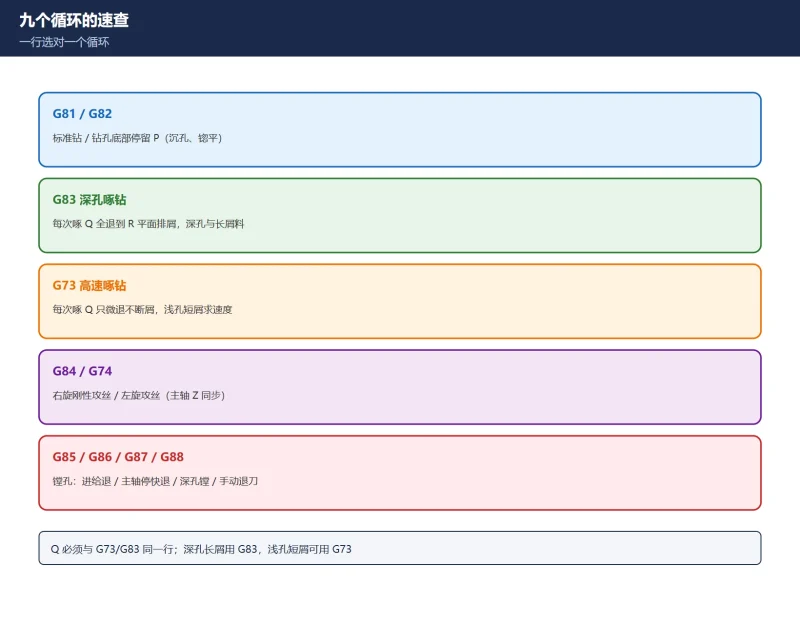
| Cycle | Purpose | Bottom behaviour | Retract plane | Required addresses | Parameters | Alarms |
|---|---|---|---|---|---|---|
| G81 | Standard drill | Feed to bottom | Rapid to R plane | X Y Z R F | 5200 range | 045 (no Q needed) |
| G82 | Drill with dwell | Dwell P at bottom | Rapid to R plane | X Y Z R P F | 5204 (P unit) | – |
| G83 | Deep-hole peck | Peck Q, full retract to clear | Retract to R plane | X Y Z R Q F | 5213 | 045 |
| G73 | High-speed peck | Peck Q, slight retract, no break | Slight retract | X Y Z R Q F | 5121 | 045 |
| G84 | Right-hand rigid tap | Spindle/Z sync, reverse out | Per tapping mode | X Y Z R F | 5200–5209 | 045 / SP0741 |
| G74 | Left-hand tap | Reverse tapping | Per tapping mode | X Y Z R F | 5200–5209 | 045 |
| G85 | Boring | Feed in, feed out | Feed out | X Y Z R F | 5200 range | – |
| G86 | Boring | Feed in, spindle stop, rapid out | Rapid out | X Y Z R F | 5200 range | – |
| G87 / G88 | Deep bore / manual retract bore | Needs orientation / manual retract | Special | X Y Z R F | Orientation params | – |
Table 1. Nine-cycle master table (exact motions follow the manual for your control)
1.2 Address word master table
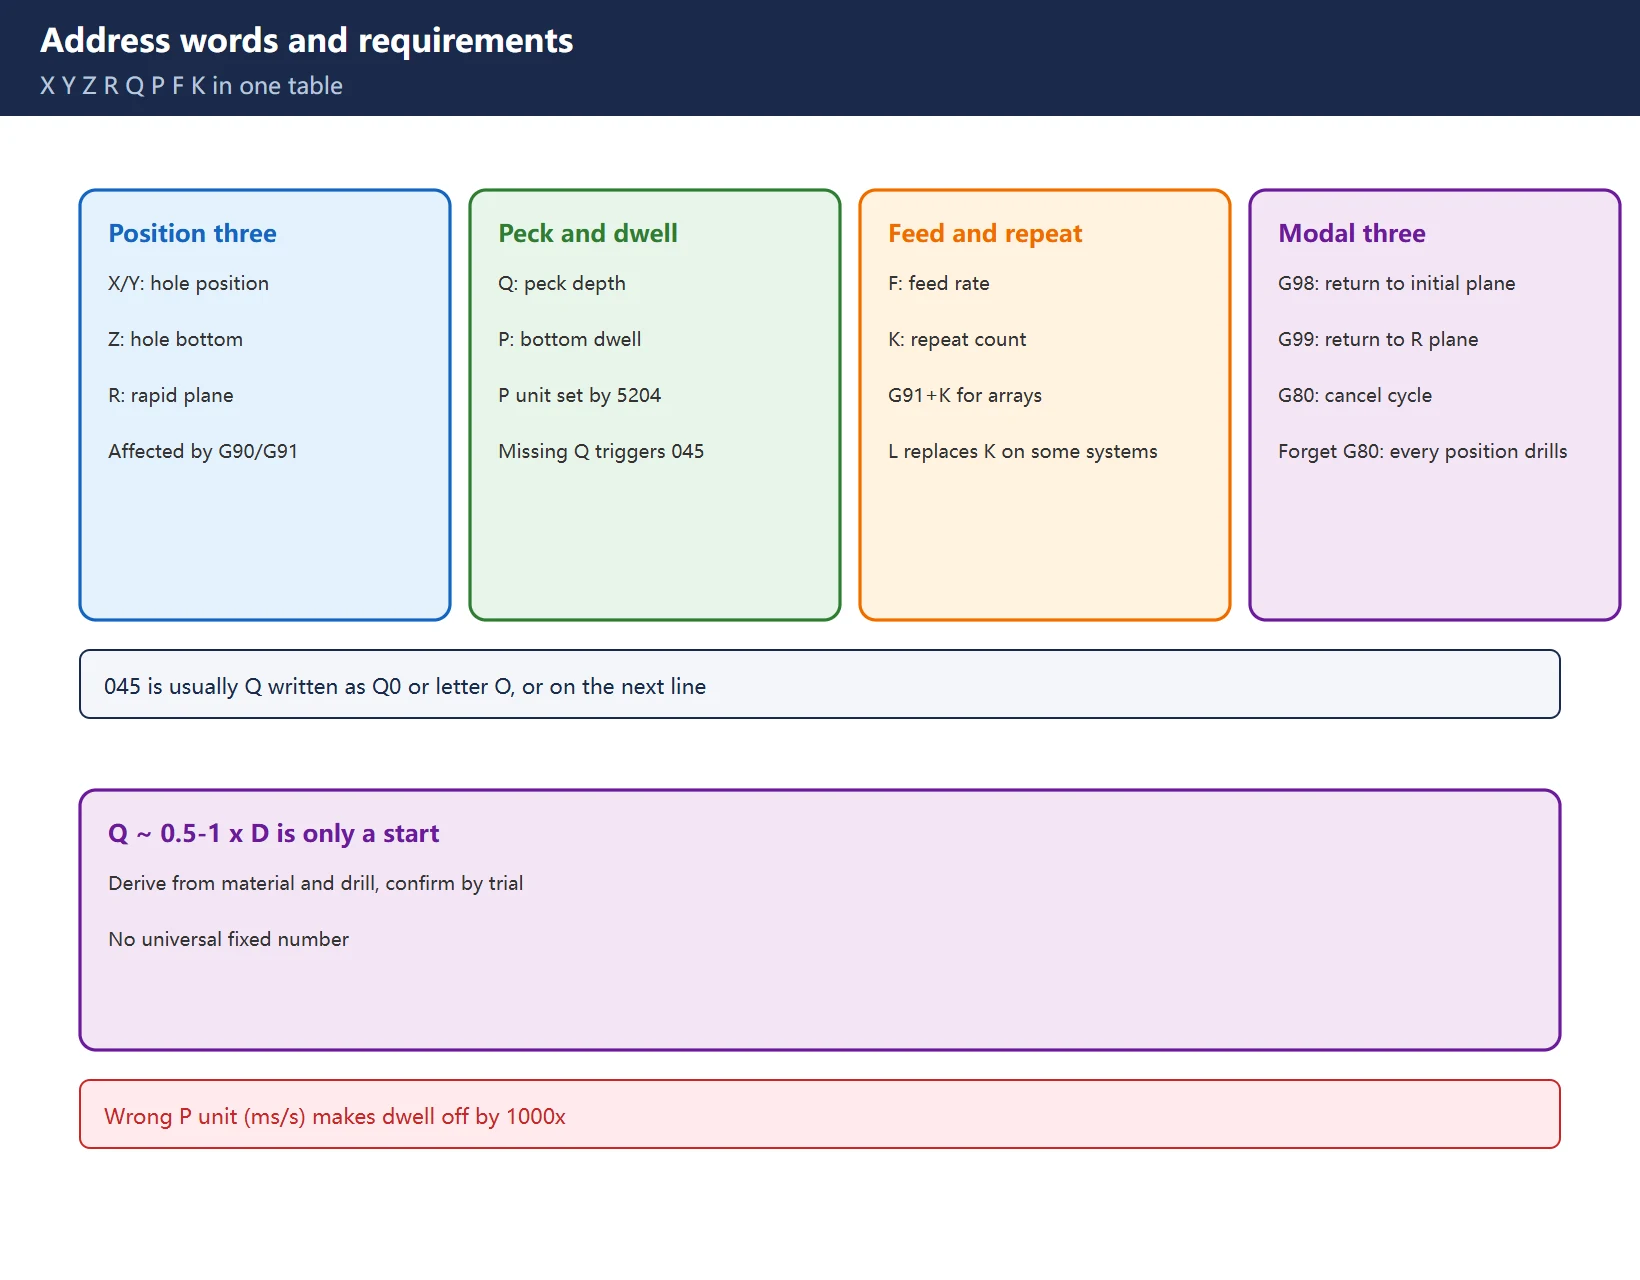
| Address | Meaning | Unit | Required | If missing |
|---|---|---|---|---|
| X / Y | Hole position | per G90/G91 | Required | No position, cycle does not run |
| Z | Hole bottom | mm/inch, per G90/G91 | Required | Wrong depth |
| R | Rapid plane | mm/inch | Required | Rapid/cut boundary unclear |
| Q | Peck depth | mm/inch | Required for G73/G83 | 045 (ADDRESS Q NOT FOUND) |
| P | Bottom dwell | ms or s (per 5204) | As needed for G82 | No dwell |
| F | Feed rate | mm/min | Required | Abnormal feed |
| K | Repeat count | count | Optional | Runs once |
| L | Some systems use it instead of K | count | system dependent | Error if mixed with K |
Table 2. Address word master table (units and requirements follow the manual for your control)
1.3 Parameter ranges
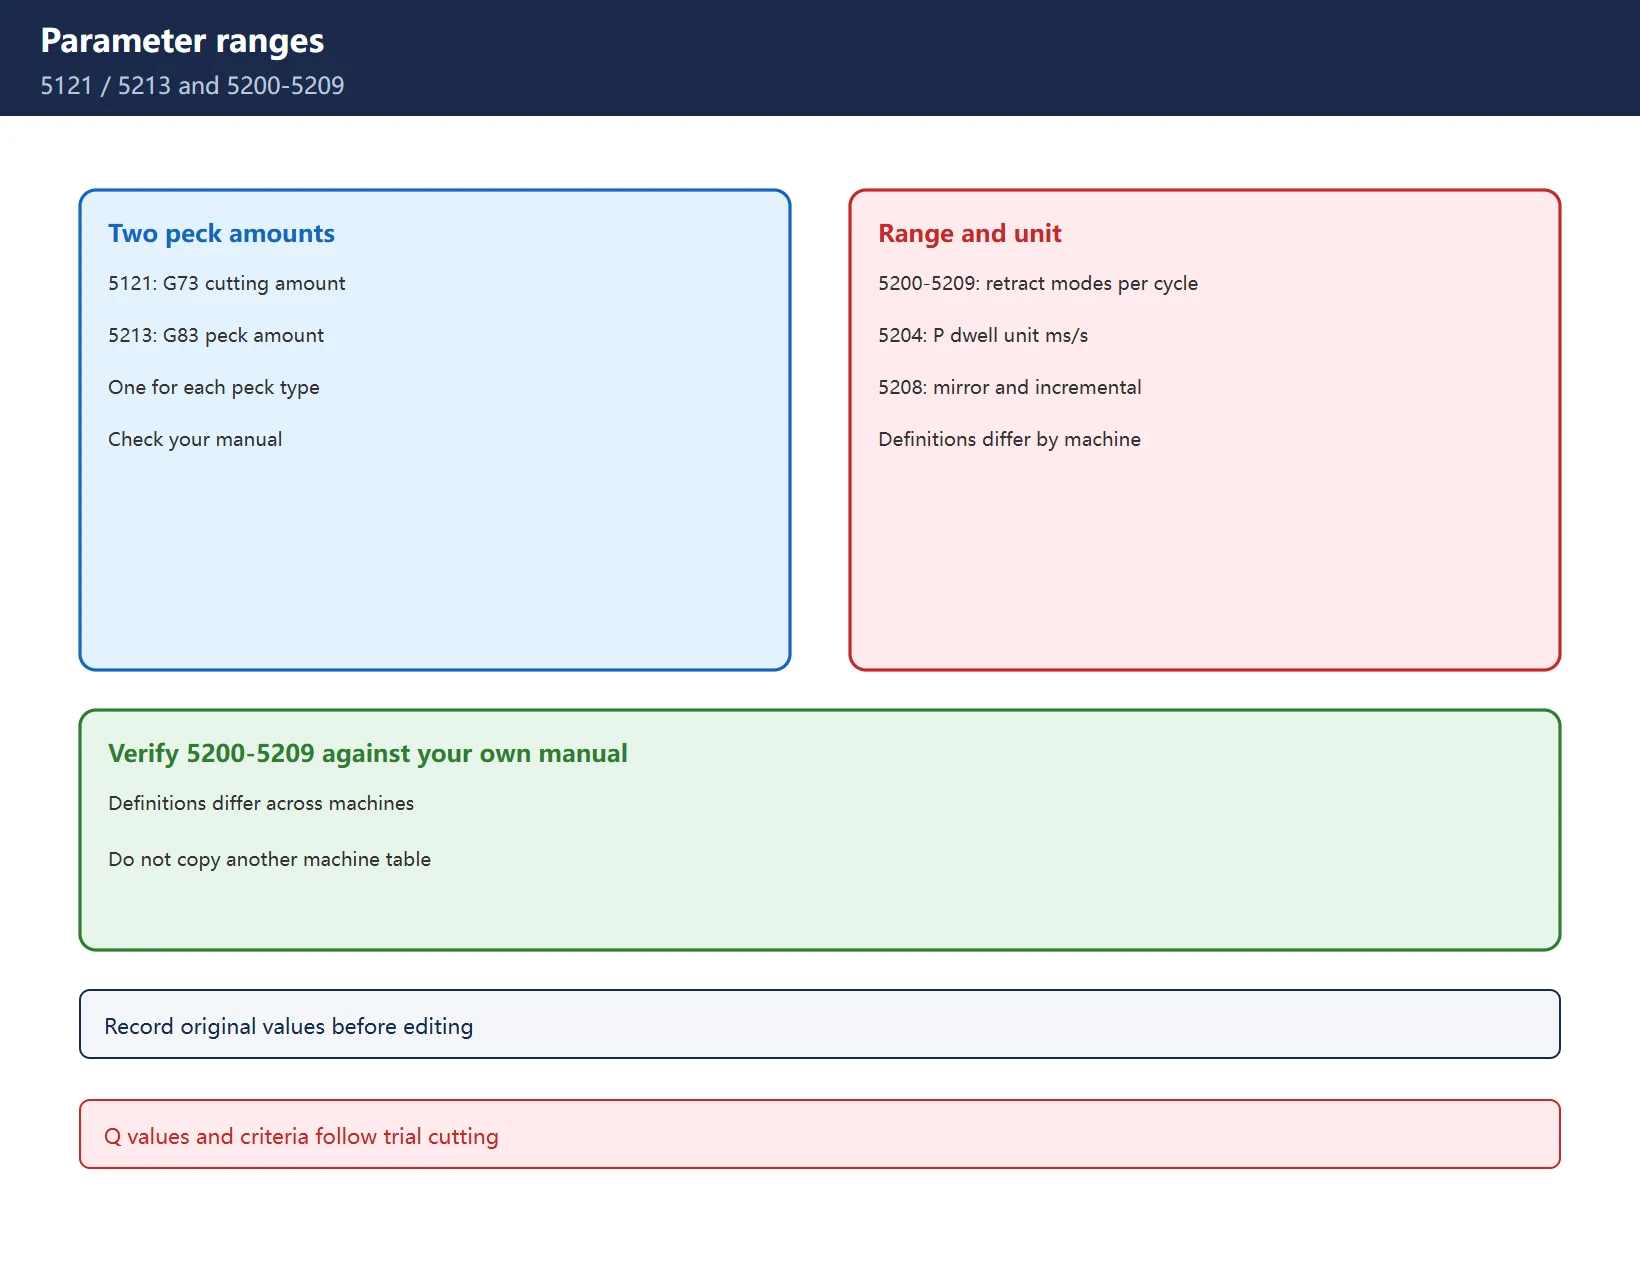
| Parameter | Function | Note |
|---|---|---|
| 5121 | G73 cutting amount | High-speed peck cutting |
| 5213 | G83 peck amount | Deep-hole peck Q baseline |
| 5200–5209 | Z/R/retract and incremental modes per cycle | Definitions differ by machine – check your manual |
| 5204 | P dwell unit (1 ms / 1 s) | Wrong unit = 1000x dwell |
| 5208 | Mirror and incremental | Varies by machine |
Table 3. Parameter ranges
1.4 Alarm reverse lookup
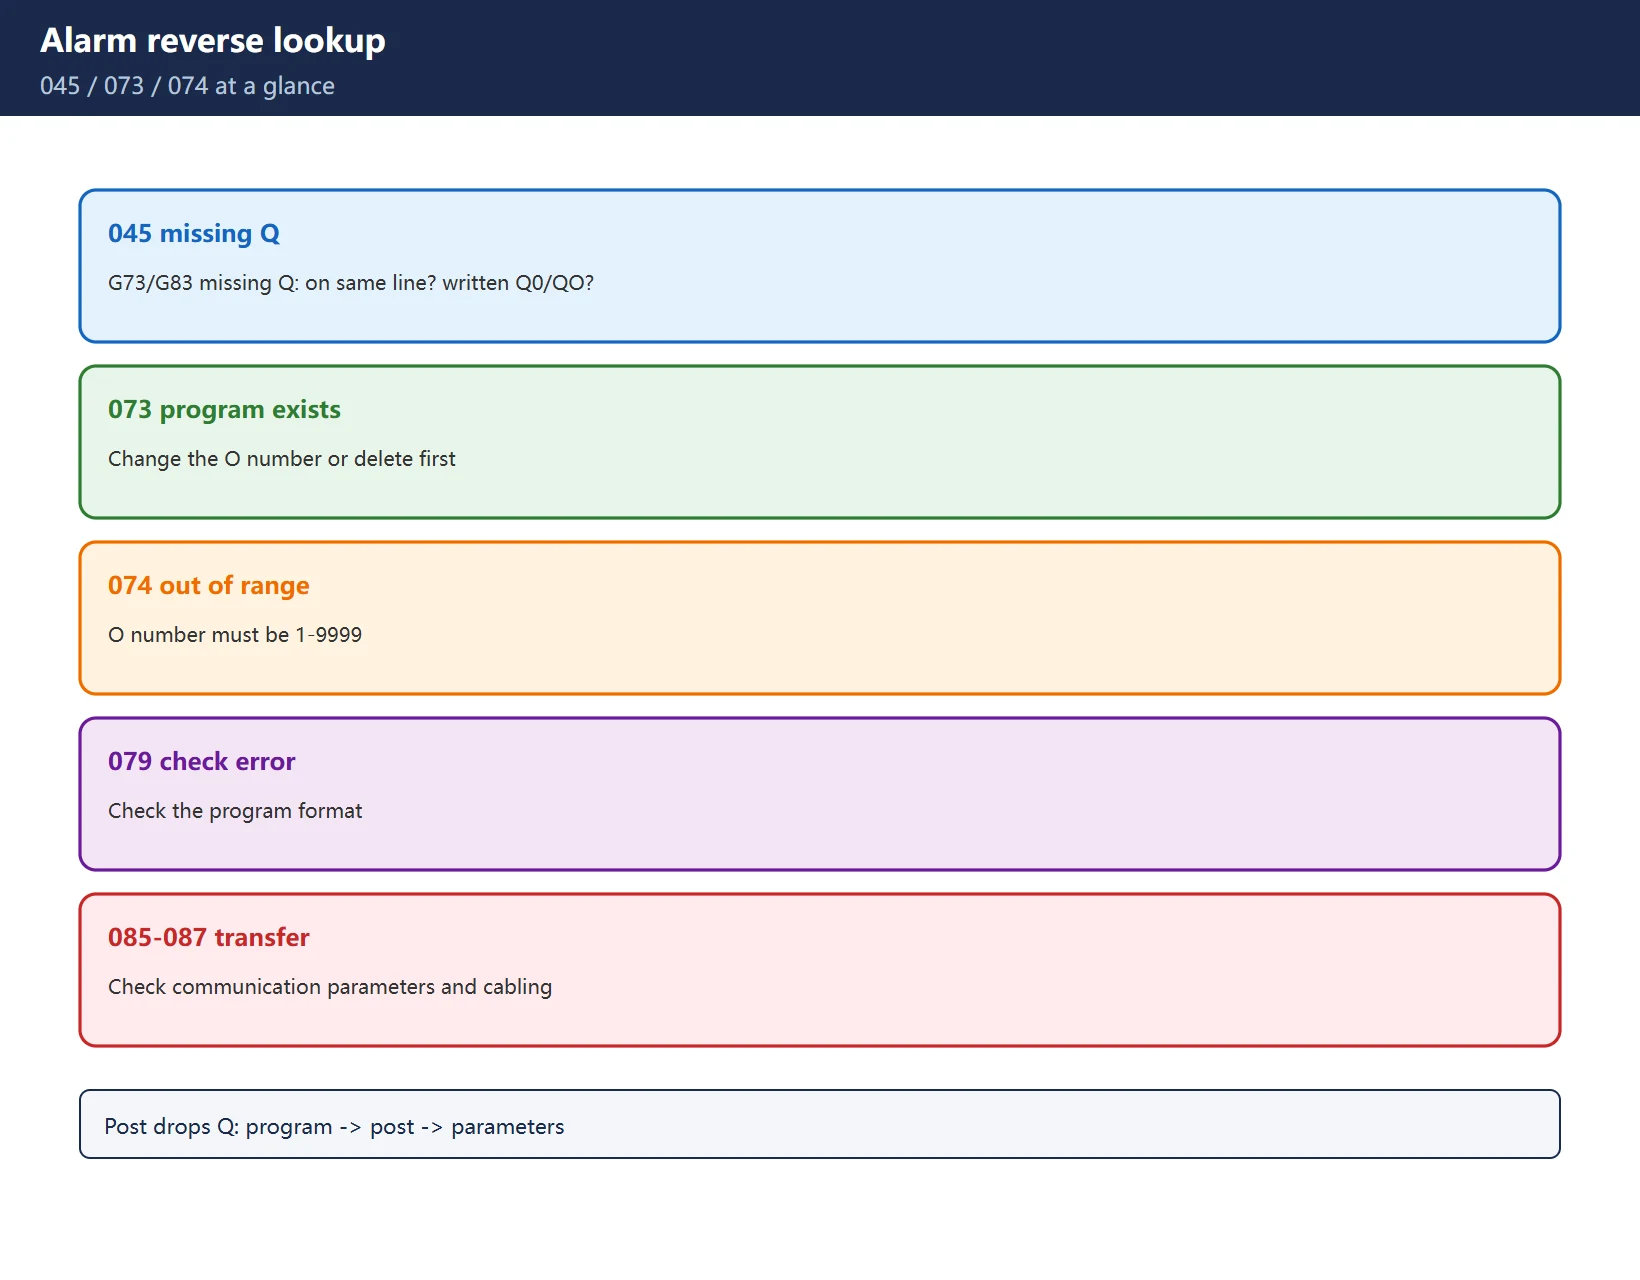
| Alarm | English text | Meaning | First check |
|---|---|---|---|
| 045 | ADDRESS Q NOT FOUND | G73/G83 missing Q | Is Q on the same line as G, or written Q0 / letter O? |
| 073 | PROGRAM NUMBER ALREADY EXISTS | Program number taken | Change O number or delete first |
| 074 | PROGRAM NUMBER OUT OF RANGE | Program number out of range | O number must be 1–9999 |
| 079 | PROGRAM CHECK ERROR | Program check error | Check program format |
| 085–087 | Transfer alarms | Data I/O abnormal | Check communication parameters and cabling |
Table 4. Alarm reverse lookup
1.5 G98 / G99 / G80 modal quick lines
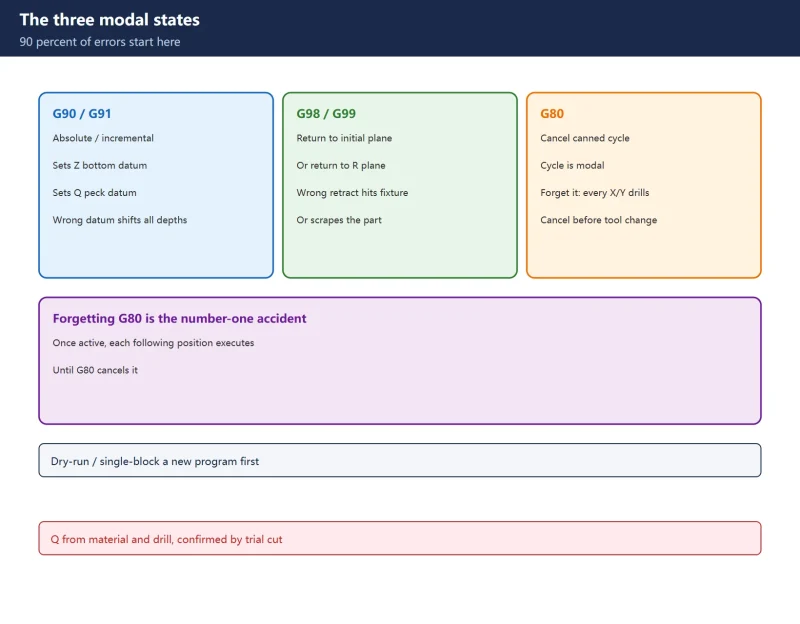
- G98 (single line): after the cycle, return to the initial plane.
- G99 (single line): after the cycle, return to the R-point plane.
- G80 (single line): cancel the canned cycle. The cycle is modal – forget it and every following position drills.
1.6 Q value rule
Q ≈ 0.5–1 x D (drill diameter) is a starting point: smaller for steel, larger for aluminium. Derive from material and tool and confirm by trial cutting – no universal fixed number. Deep holes (>5xD) and long chips use G83 with full retract; shallow holes and short chips can use G73 with slight retract.
1.7 Sources and version note
This page is a quick-reference table only and does not reproduce FANUC operation manual text. Codes, addresses and parameter ranges come from general FANUC canned-cycle conventions, compiled 2026-11-19. The 5200–5209 definitions differ by machine – verify against the manual supplied with your machine; Q values and criteria follow trial cutting. For the full walkthrough see Fanuc Canned Cycles Explained.
Frequently Asked Questions
Where do I look up FANUC canned-cycle parameters, and what do 5121 and 5213 control?
Parameter ranges follow the “canned cycle” chapter of the manual for your machine. In general conventions 5121 controls the G73 high-speed peck cutting amount and 5213 the G83 deep-hole peck amount; the 5200–5209 definitions differ by machine and must be verified against your own manual.
For alarm 045 on a canned cycle, do I check the program or the parameters first?
Check the program first: 045 is ADDRESS Q NOT FOUND, almost always because Q is not on the same line as G73/G83 or was written as Q0 / letter O. The order is program -> post-processor -> parameters.
Is the Q value algorithm the same for G73 and G83?
The rule is the same (Q ≈ 0.5–1 x D, derived from material and tool), but retract behaviour differs: G73 retracts slightly without full chip break for shallow holes and short chips; G83 retracts fully to clear chips for deep holes and long chips. Exact values follow trial cutting.
Last updated: 2026-11-19
Where to go next
- FANUC Troubleshooting — the full guide library: alarms, diagnosis numbers, servo, spindle, PMC and electrical faults, organised by symptom.
- CNC Repair Tools — which instrument measures what: multimeters, clamp meters, insulation testers and oscilloscopes, with the specification that actually matters.
- Remote Technical Support — have the readings reviewed with you: alarm reverse lookup, PMC ladder analysis and servo tuning advice by call. Repair companies and integrators welcome.
- Buying & Ownership Decisions — refurbished vs new, used-machine checks, software licensing and manuals: spend with the field facts in hand.
Read the guide, get the right instrument, or walk the diagnosis through with someone — pick whichever you need.
The original Chinese version — same procedure, with the full field notes.
































暂无评论内容