


Written for the FANUC 0i series. Parameter numbers follow the common 0i convention; always confirm initial values against your machine’s parameter manual.
1. First, decide which shift type the machine uses
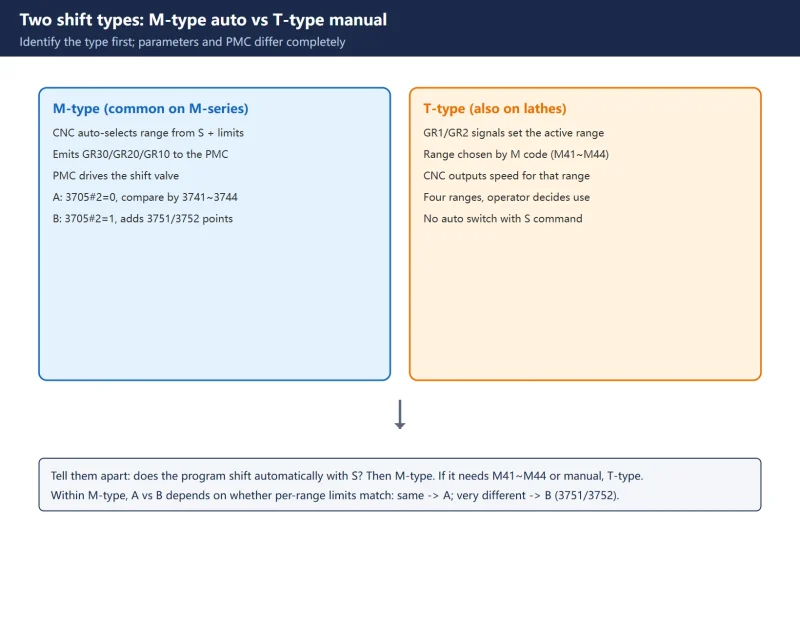
There are two families, with completely different parameters and PMC handling. Identify this first:
M-type shifting (most common on M-series, 0i-MF / 0i-Mate-M): the CNC auto-selects the range from the S command and the per-range speed limits, then announces it to the PMC through the GR30/GR20/GR10 signals. It splits further into:
- Type A:
3705#2 = 0. The CNC picks the range directly by comparing against3741~3744. - Type B:
3705#2 = 1. Adds3751/3752as the motor-speed switch points between ranges, which resolves the auto-detection trouble when each range has a different upper limit.
T-type shifting (also available on T-series lathes): the current range is set by the GR1/GR2 signals (four ranges), chosen by an M code in the program (e.g. M41~M44) or manually; the CNC simply outputs the speed for the active range.
2. The core parameter list
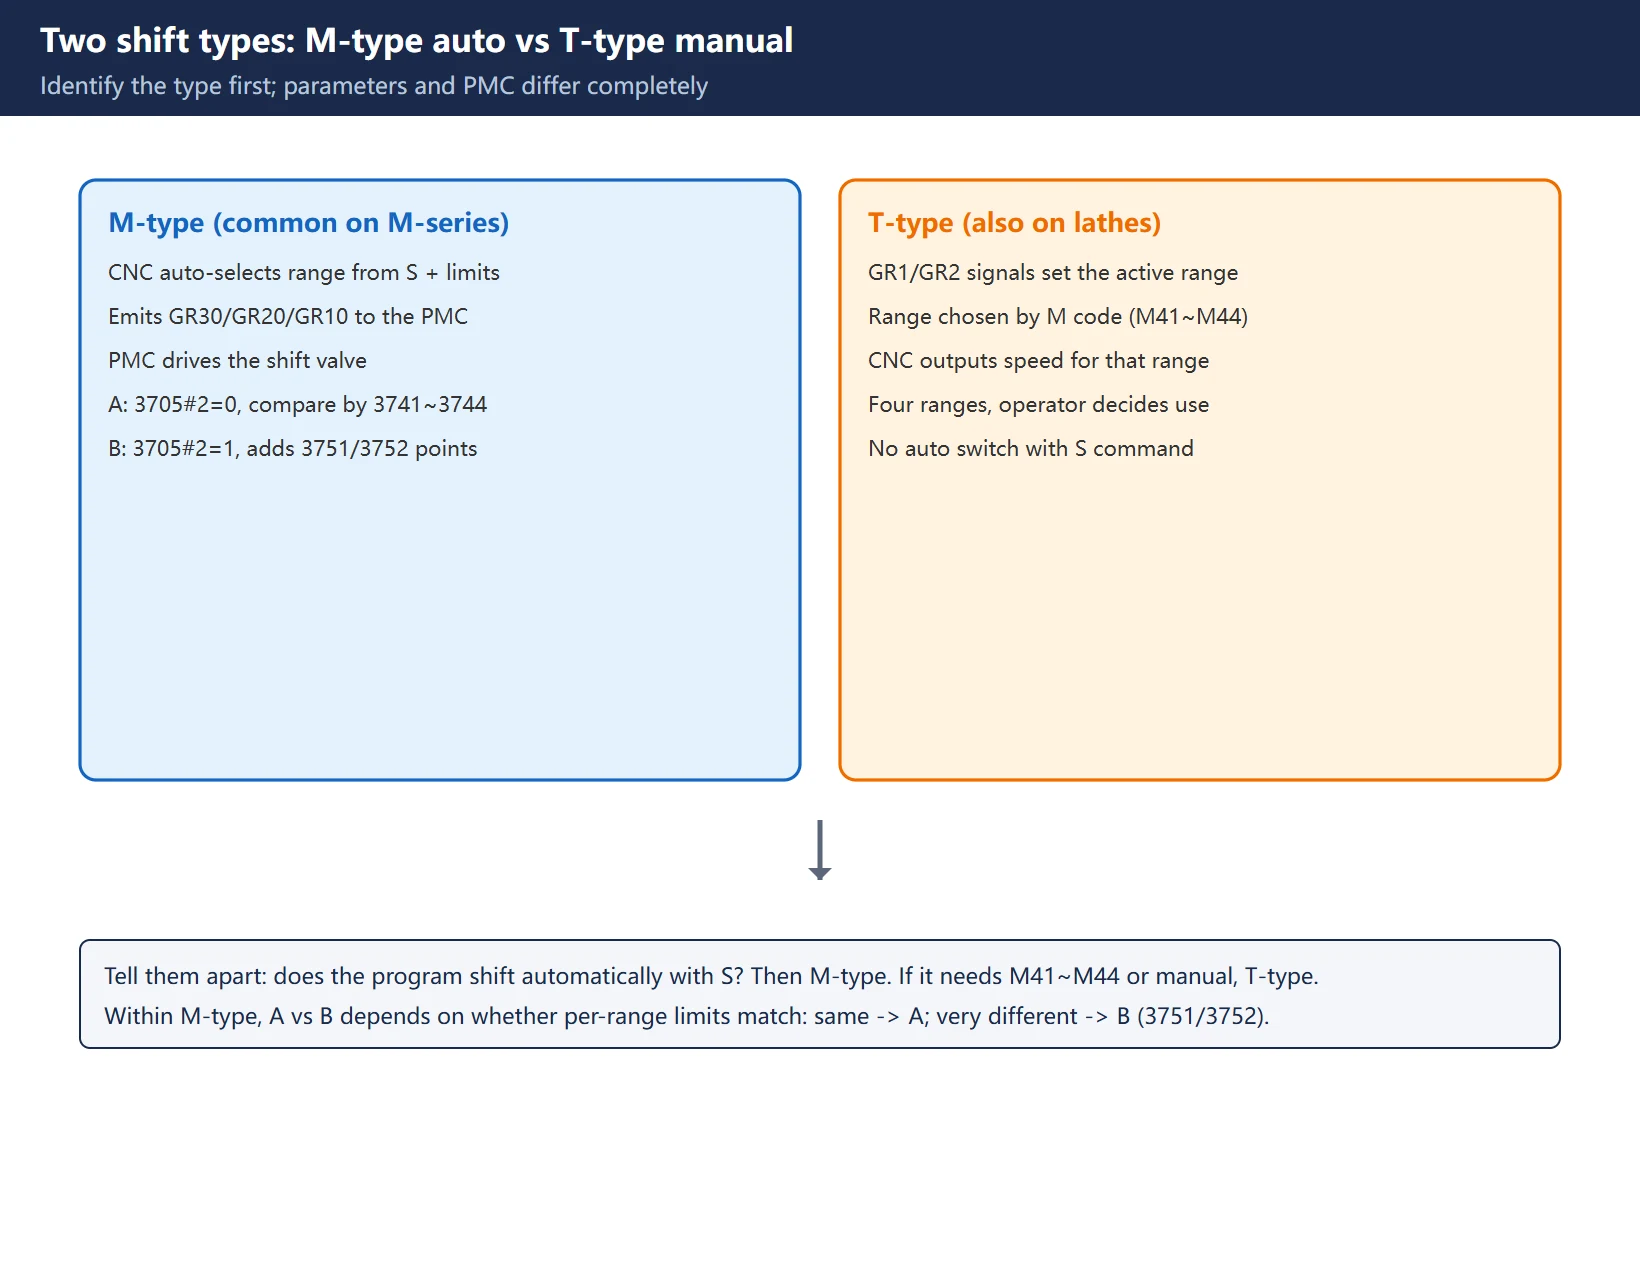
Whether M-type or T-type, set this group first:
| Parameter | Purpose | Note |
|---|---|---|
3705#2 | Gear switching method | 0 = Type A, 1 = Type B |
3705#1 | Use SOR for gear displacement | =1 lets the spindle oscillate at 3732 during shift |
3705#4 | Output S code / SF signal | Must =1 on M-series to use S/SF in PMC |
3732 | Spindle motor speed during gear shift | Oscillation speed for the fork to engage |
3735 | Spindle motor minimum clamp speed | Lower motor-speed limit (digital) |
3736 | Spindle motor maximum clamp speed | =4095 means unlimited |
3741~3744 | Spindle maximum speed per range | Range 1-4 upper limit, scaled by ratio |
3751 | Motor speed at the 1->2 switch point | Type B only, computed |
3752 | Motor speed at the 2->3 switch point | Type B only, computed |
3753 | Delay after the shift M code outputs | Wait for the mechanism before FIN |
4056~4059 | Spindle-to-motor gear ratio (by CTH1A/CTH2A) | One set per range, x1/1000 unit |
4171~4174 | Motor-sensor to spindle gear ratio | Same four ranges |
Correcting a common misprint: briefs often write the clamp speeds as
3734/3735, but there is no 3734 in the standard set. The minimum clamp is3735and the maximum clamp is3736(4095 = unlimited).3741~3744are the per-range spindle maximum speeds. Treat any “3734” as 3735/3736.
3. How the gear ratio is actually computed
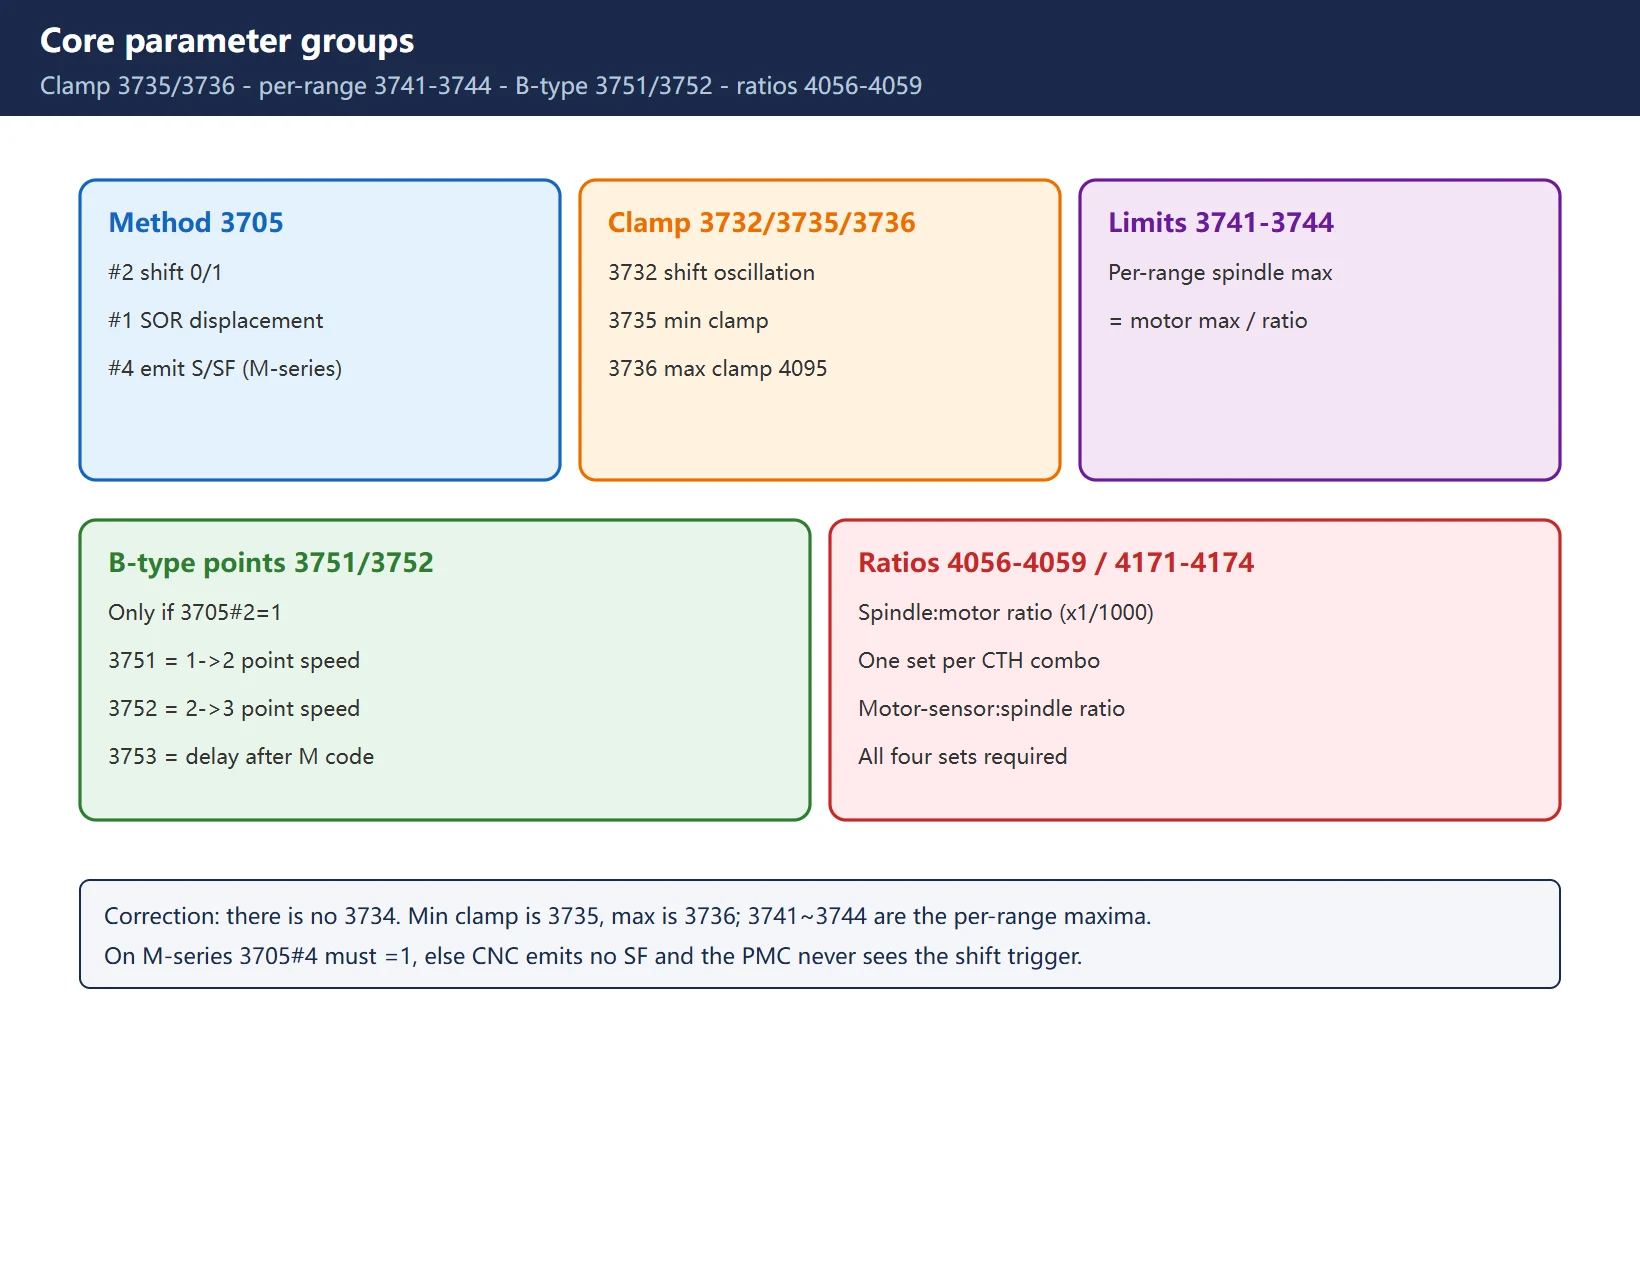
This is where people invert things. 4056~4059 hold the spindle-to-motor gear ratio (in 1/1000 units), one set per CTH1A/CTH2A combination. It is a different quantity from 3741/3742, but the two are coupled:
3741~3744set the highest spindle speed each range can reach (already ratio-scaled).4056~4059/4171~4174tell the CNC how to convert motor speed into spindle speed for display and control; after a shift, when CTH1A/CTH2A change, the CNC switches to the matching ratio set.
Complete example (ZF two-range, high 1:1, low 4:1, motor max 7000, shift speed 800):
3705#2 = 1(Type B)3735 = 5,3736 = 4095,3732 = 33741 = 7000/4 = 1750(low-range spindle limit)3742 = 7000(high-range spindle limit)3751 = 800 x 4095 / 1750 = 1872(1->2 switch-point motor speed)3752 = 40954056~4059 = 100, 100, 100, 400(ratio x1000 for the four CTH combinations)4171~4174 = 1, 1, 4, 1(motor-sensor to spindle ratio)
The hard check: at low range the actual spindle maximum = motor maximum / low-range ratio. Above, low = 7000 / 4 = 1750, matching 3741 – so it is not inverted.
4. PMC signals that must be handled
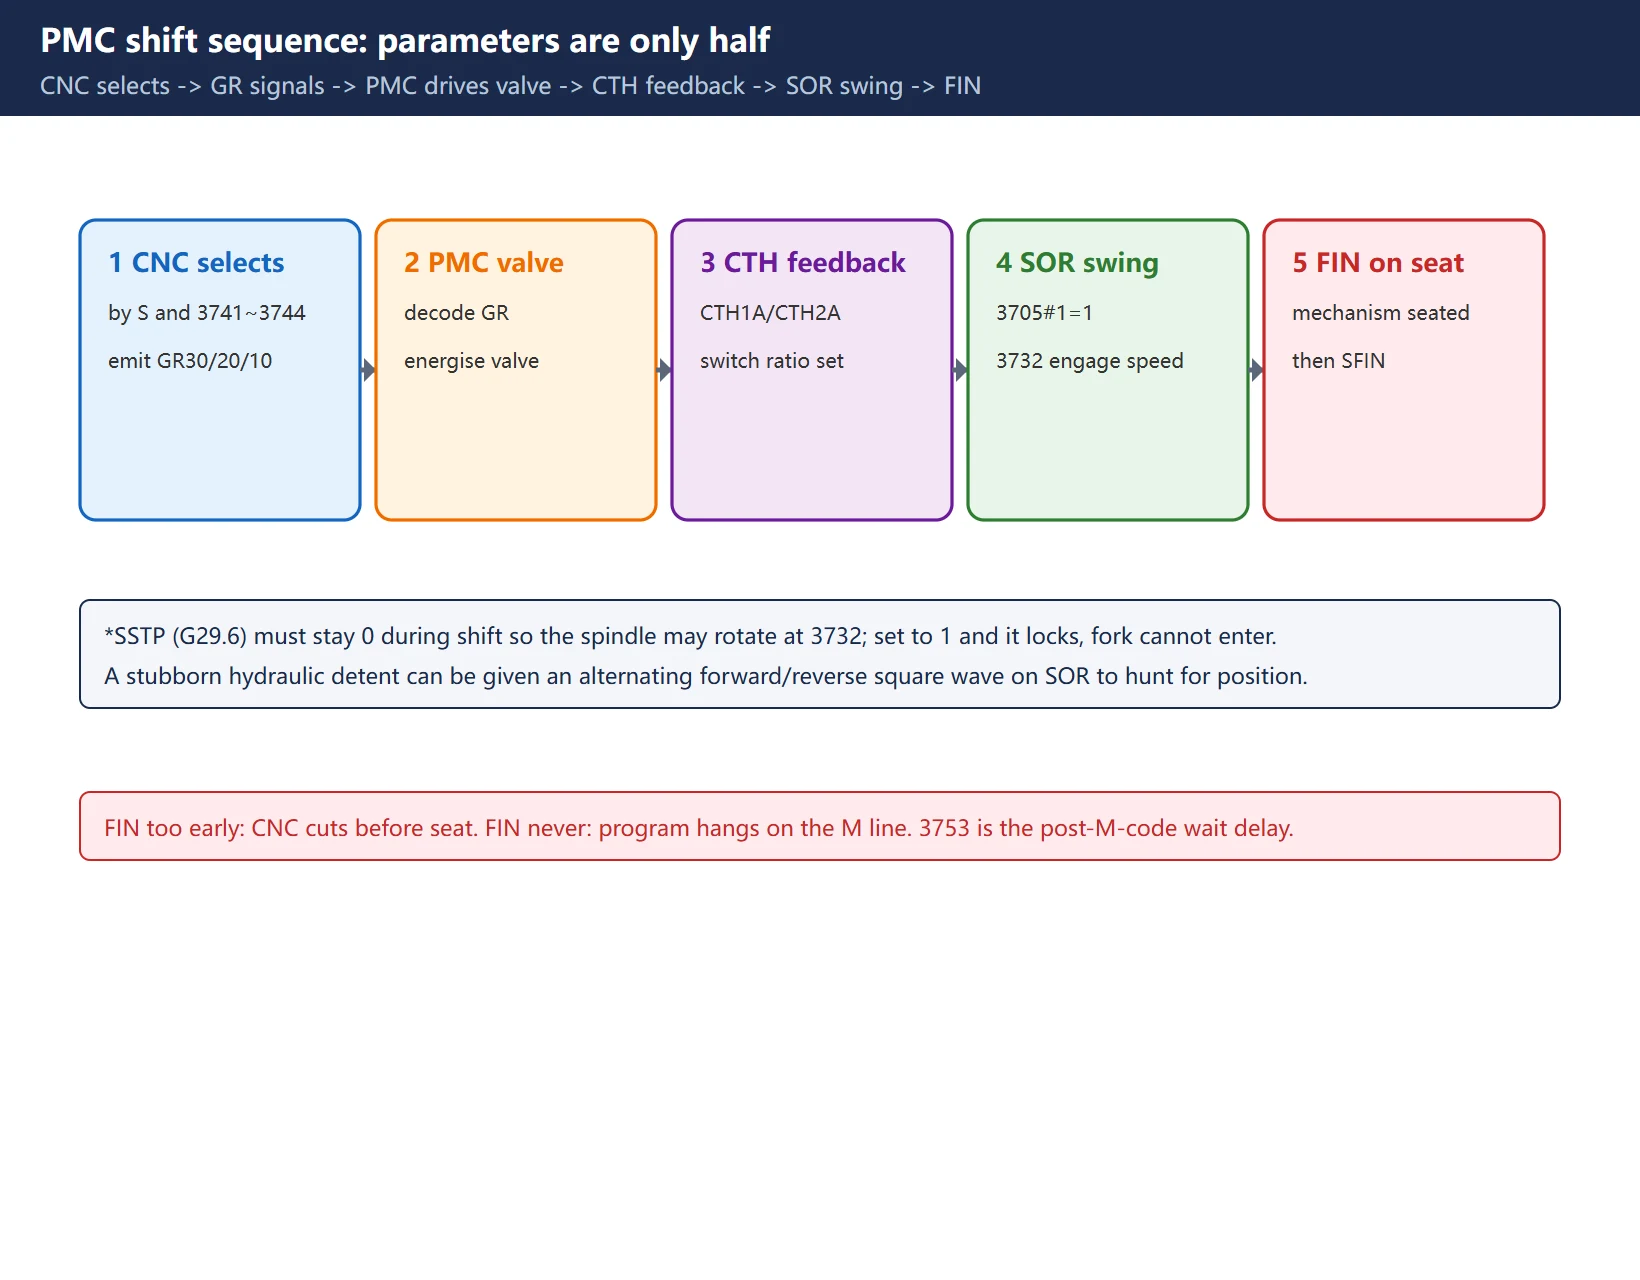
Filling parameters is only half the job; the shift action is driven by the PMC. Key signals:
- GR30/GR20/GR10 (G28.0/28.1/28.2): the gear-range select signals the CNC emits after choosing a range; the PMC uses them to energise the shift solenoid/valve.
- CTH1A (G70.3) / CTH2A (G70.2): the serial spindle actual gear stage feedback. The CNC uses this pair to pick which of
4056~4059to apply. The range and this pair must correspond, or the displayed speed diverges from reality by a large factor. - SOR (G29.5): spindle orientation / gear-displacement signal. With
3705#1=1, during a shift the spindle oscillates at the3732speed to help the fork engage; a stubborn hydraulic detent can be given an alternating forward/reverse square wave. - *SSTP (G29.6): spindle stop. Keep it 0 during the shift so the spindle is allowed to rotate at
3732; set it to 1 and the spindle locks, and the fork cannot enter. - SF (G70.5 class) / SFIN (G5.2): spindle function strobe and completion. On M-series
3705#4=1is required before SF is emitted; the PMC issues SFIN only after the mechanism is truly in place, otherwise the CNC hangs on the M line. - M code and the
3753delay: T-type or manual shifting uses M41~M44; after the CNC emits the M code it waits the3753delay before judging completion. In the ladder, issue FIN only after the mechanism is actually seated.
5. Five failure points
- Wrong clamp-speed name: 3734 does not exist; minimum is 3735, maximum is 3736. Leave 3736 wrong and the spindle speed gets clamped dead.
- 3741/3742 inverted against the ratio: the low range has the larger ratio, so its spindle limit is smaller;
3741must equal motor max / low ratio. Invert it and the low range overspeeds and alarms. - CTH1A/CTH2A not matched to the range: the PMC range signal and the CNC ratio set are misaligned, so the screen speed and real speed differ by several times.
- *SSTP not held at 0: the spindle will not oscillate during the shift, the fork jams, and gears grind or lock.
- FIN too early or never: issuing FIN before the mechanism seats makes the CNC cut too soon; never issuing it hangs the program on the M line.
6. Acceptance checklist
- [ ]
3705#2matches the actual shift method (A/B); on M-series3705#4=1is set - [ ]
3735/3736clamp speeds are sane;3732oscillation can drive the fork - [ ]
3741~3744per-range limits = motor max / range ratio, none inverted - [ ]
4056~4059/4171~4174four ratio sets filled per CTH combination - [ ] PMC chain GR signal -> valve -> CTH1A/CTH2A feedback all live
- [ ] Measured per-range top speed matches the screen (low clearly below high)
- [ ] No gear grinding, no lock-up, no hang on the M line
Further reading: the shift PMC signals share the same discrete-logic handling as FANUC PMC Force output, and the spindle-motor parameters are covered in FANUC analog spindle commissioning.
Frequently Asked Questions
Why are there four sets in 4056~4059 when I only use two ranges?
The four sets are reserved for the four combinations of CTH1A/CTH2A (00/01/10/11); the CNC uses this pair to pick the active ratio set. Even with only two physical ranges, fill all four correctly and set the unused two equal to an in-use range – otherwise after a shift the CNC applies the wrong ratio and the screen speed diverges from the real speed by a large factor.
Do I use 3751/3752, and how do they relate to 3741/3742?
Only Type-B shifting (3705#2=1) uses 3751/3752. 3741/3742 are the per-range spindle maximum speeds; 3751/3752 are the switch-point motor speeds (digital), computed as 3751 = 4095 x switch-point spindle speed / 10V-motor-speed. Type-A (3705#2=0) does not need them – the CNC selects directly by 3741~3744.
The spindle will not oscillate during shift and the fork will not enter – what now?
First check 3705#1 = 1 (enable SOR displacement) and that *SSTP (G29.6) is held at 0 during the shift; then check 3732 oscillation speed is enough to move the fork. For a stubborn hydraulic detent, change the SOR-period spindle into an alternating forward/reverse square wave so the detent hunts for position.
Last updated: 2026-10-31
FANUC Serial Spindle Alarms 749/750/751
Where to go next
- FANUC Troubleshooting — the full guide library: alarms, diagnosis numbers, servo, spindle, PMC and electrical faults, organised by symptom.
- CNC Repair Tools — which instrument measures what: multimeters, clamp meters, insulation testers and oscilloscopes, with the specification that actually matters.
- Remote Technical Support — have the readings reviewed with you: alarm reverse lookup, PMC ladder analysis and servo tuning advice by call. Repair companies and integrators welcome.
Read the guide, get the right instrument, or walk the diagnosis through with someone — pick whichever you need.
The original Chinese version — same procedure, with the full field notes.




























暂无评论内容