最新发布第3页
排序
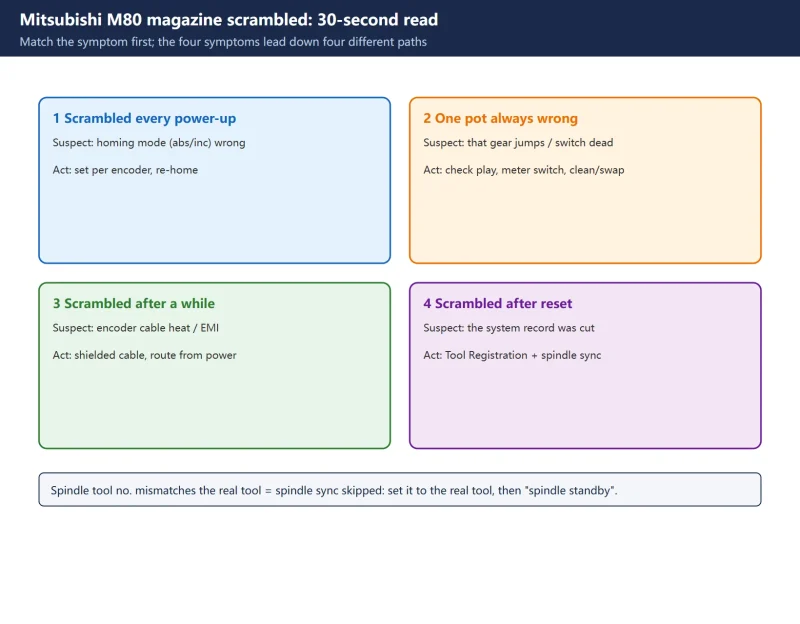
Mitsubishi M80 Magazine Scrambled Quick Chart: Symptom, Tool Registration Fields and R Registers
One page for a scrambled Mitsubishi M80 magazine: match the symptom, then act. Spindle sync, the four Tool Registration targets, and the magazine / tool-life R-register addresses a...

 18小时前
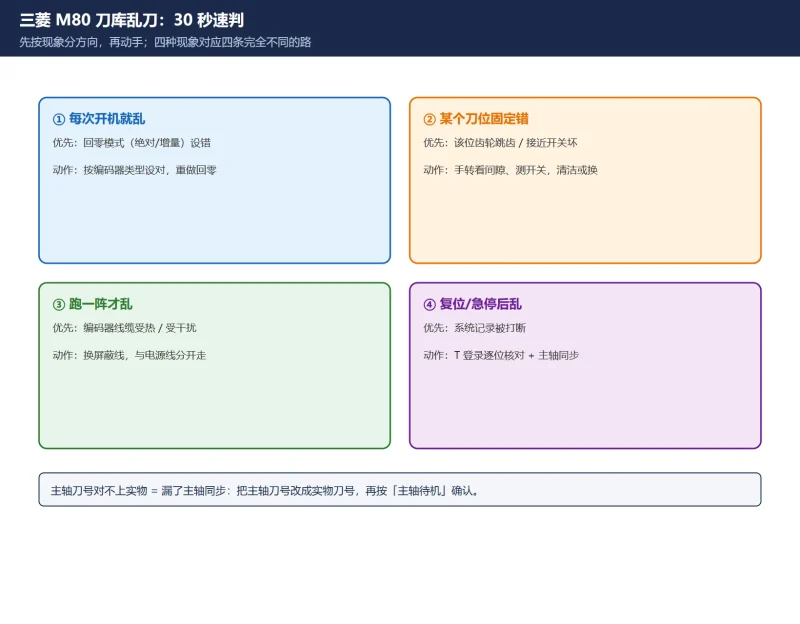
三菱 M80 刀库乱刀速查表:现象·原因·先查 + T 登录四个位置 + R 寄存器
一页看完三菱 M80 刀库乱刀:按现象对号入座,主轴同步、T 登录四个位置、刀库刀具数据与刀具寿命的 R 寄存器地址一次列清。适合现场贴着机台用。
18小时前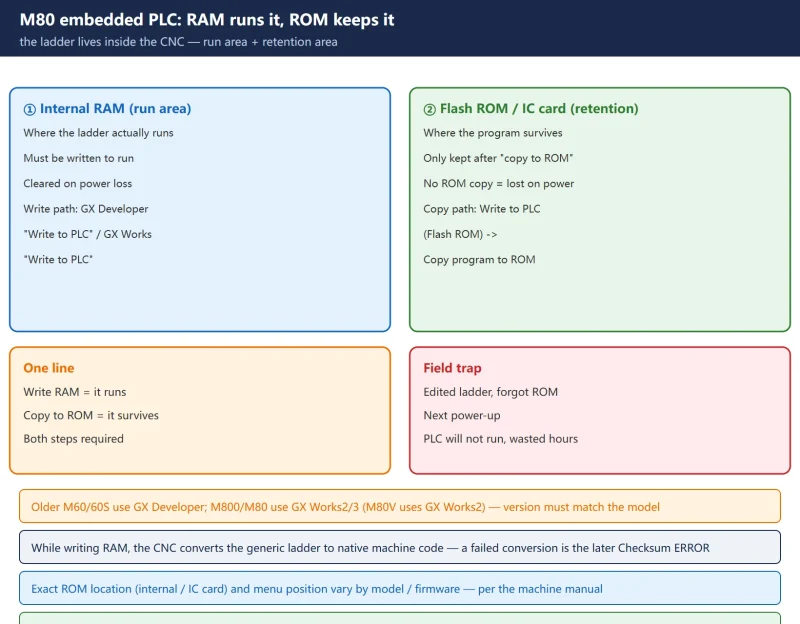
How to Write Mitsubishi M80 Ladder Logic into the CNC — RAM Write, ROM Copy and Checksum ERROR
How to write the Mitsubishi M80 / M800 ladder logic (the embedded PLC sequence program) into the CNC — the GX Developer / GX Works2·3 RAM write flow, why you must 'copy to ROM', ...
18小时前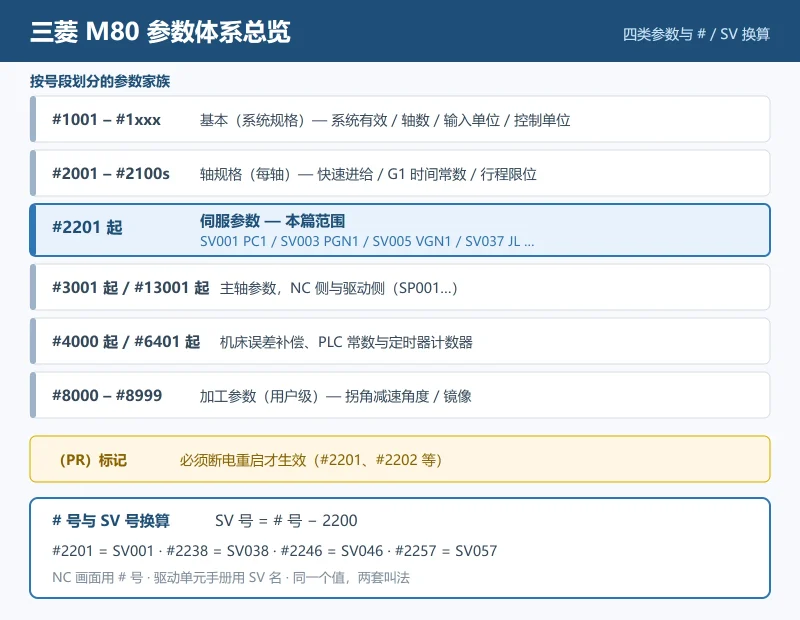
三菱 M80/M70 伺服参数速查:#2201–#2210 全表、#2233/#2238/#2246 共振抑制、#2235/#2237 惯量辨识完整对照
三菱 M80/M70 伺服参数速查:#2201–#2210 全表(PC1/PC2 齿轮比、PGN1 位置环、VGN1 速度环)、#2233/#2238/#2246 共振抑制三件套、#2235→#2237 惯量辨识实测步骤、SHG 与 OMR-FF 互斥、伺服...
18小时前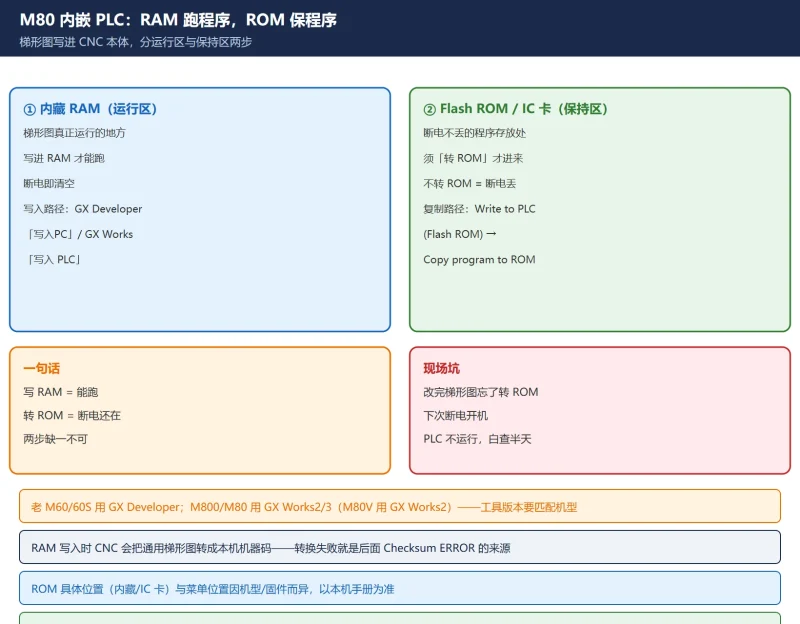
三菱 M80 梯形图怎么写进 CNC?GX Developer 写 RAM、转 ROM 与 Checksum ERROR 排查
三菱 M80 / M800 的梯形图(内嵌 PLC 序列程序)怎么写进 CNC:GX Developer / GX Works2·3 写入内藏 RAM 的流程、为什么必须'转 ROM'固化、以及 Checksum ERROR 的根因(转换错误把出错步变 N...
18小时前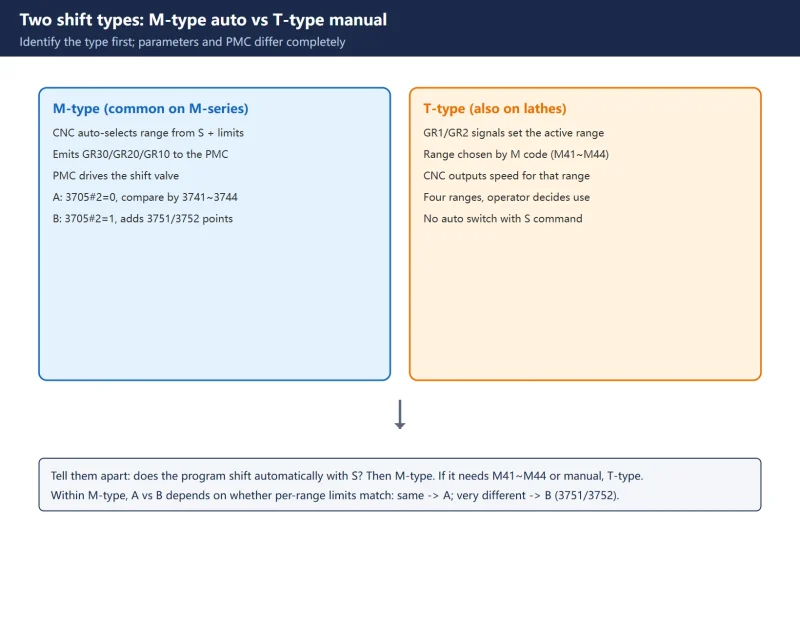
FANUC Spindle Gear Shifting: 3705/3732/3735/3741-3744/3751-3753/4056-4059 and PMC Signals
Gear-shift setup breaks most often because the clamp-speed parameter names are confused (there is no 3734; minimum is 3735, maximum 3736), 3741-3744 is inverted against the gear ra...
18小时前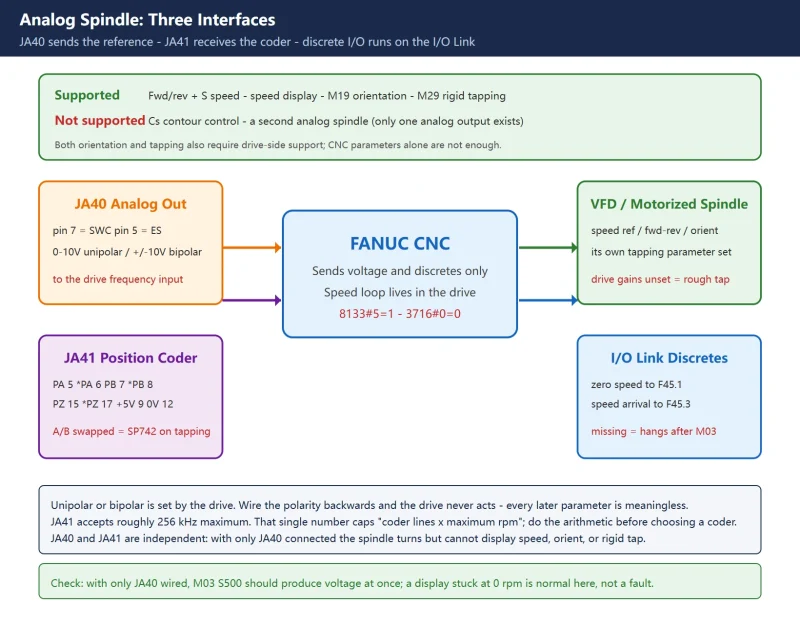
Fanuc Analog Spindle Commissioning: Enable Chain 8133#5/3716#0/3717, 3730/3731 Voltage Calibration, and JA40/JA41 Wiring
An analog spindle is rarely beaten by the number of parameters. It is beaten by a wrong enable order, 3730 and 3731 swapped, or an inverted coder phase on JA41. Four stages in orde...
18小时前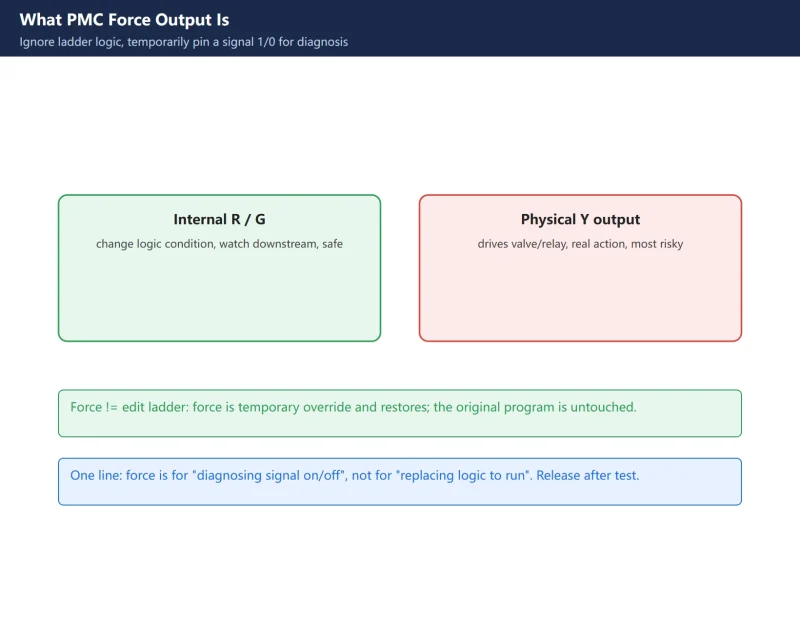
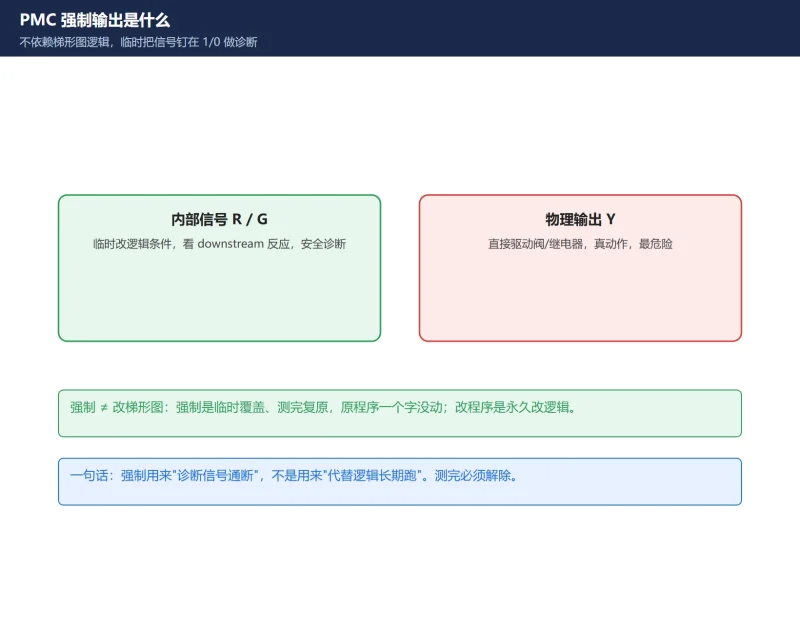
How to Use FANUC PMC Force Output (FORCE): Path (PMCDGN/STATUS/FORCE) + Forceable Addresses (G/R/Y) + Stop PMC / Release / Safety Rules
FANUC PMC force output (FORCE) pins a signal to 1 or 0 regardless of ladder logic, telling whether 'the valve is bad, the wire is broken, or the logic never arrived'. This guide co...
18小时前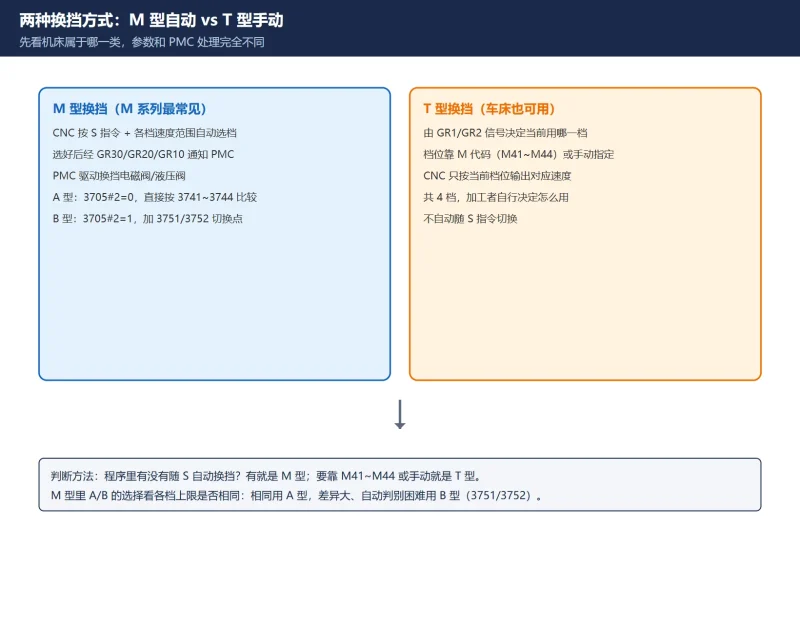
FANUC 主轴齿轮换挡参数全解:3705/3732/3735/3741-3744/3751-3753/4056-4059 + PMC 信号
主轴齿轮换挡(高低档)错得最多的是钳速参数名搞混(标准里没有 3734,最低钳速 3735、最高 3736)、3741-3744 与各档传动比算反、以及 PMC 侧 CTH1A/CTH2A 与 GR 信号没对应。本文按换挡方式...
18小时前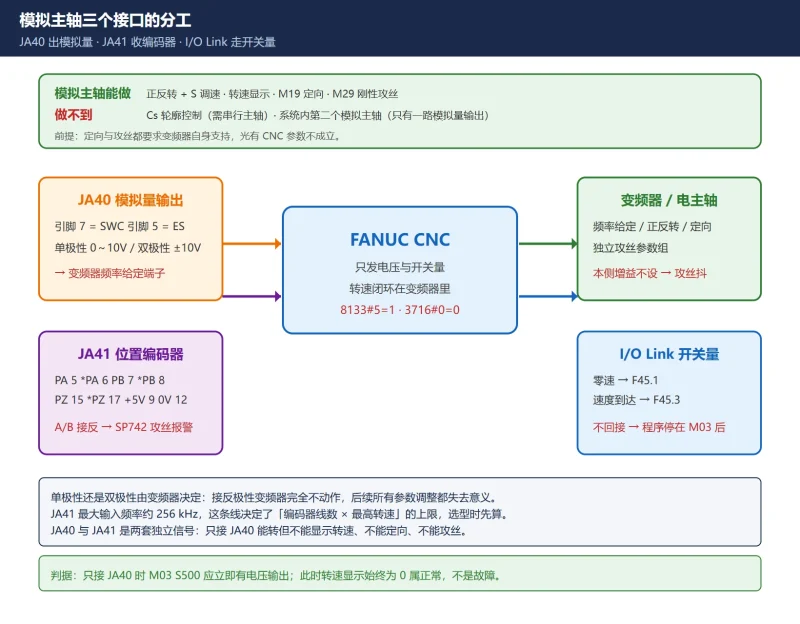
FANUC 模拟主轴调试全流程:8133#5/3716#0/3717 启用链 + 3730/3731 电压标定 + JA40/JA41 接线
模拟主轴的坑不在参数多,而在启用链顺序错、3730 与 3731 填反、JA41 编码器 A/B 接错。本文按接线→启用链→电压标定→功能验证四步走:给出 3717 填 0 时无报警却不转的原因、3731 先 3730 ...
18小时前




扫一扫,添加我的微信