最新发布第28页
排序
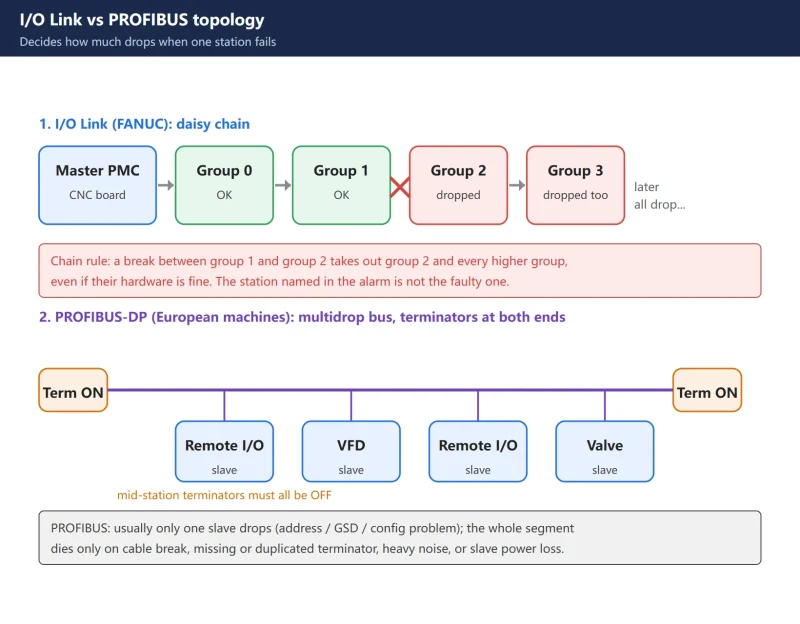
How to Troubleshoot I/O Link & PROFIBUS Station Dropout: Reading ER97 + the I/O Link Chain Rule + PROFIBUS BF LED Diagnosis + Terminator/Address/Shielding Checklist
Do not swap modules the moment a station drops. FANUC I/O Link is a daisy chain: one break takes out everything downstream, so the station named in the alarm is usually not the fau...

 昨天
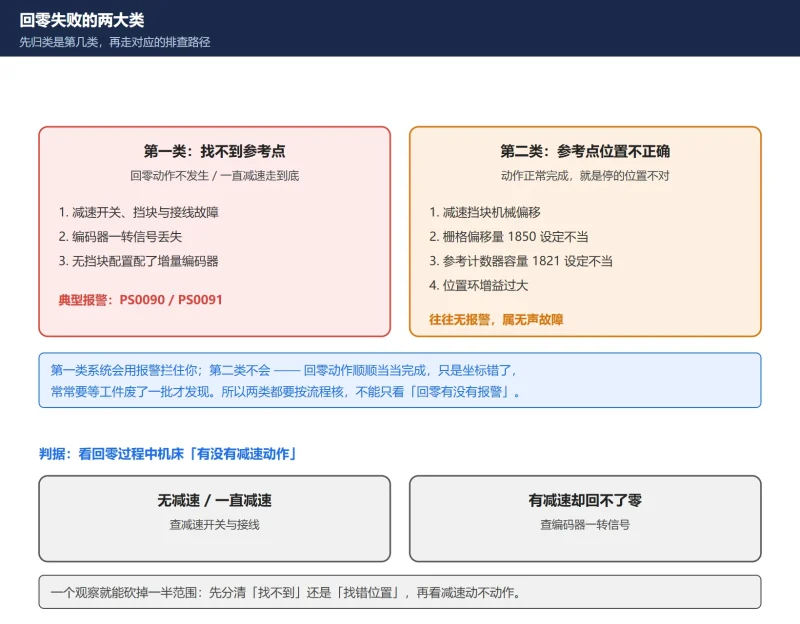
数控机床回零失败怎么分类排查?”找不到参考点”与”参考点位置不对”两大类 + 减速开关/一转信号 + 1850 栅格偏移 / 1821 参考计数器 + 绝对值编码器电池
回零失败别再靠换件试:先分成'找不到参考点'和'参考点位置不正确'两大类。前者再看回零时有没有减速动作——无减速查减速开关与接线,有减速仍失败查编码器一转信号;后者按偏差形态区分 1850 ...
19小时前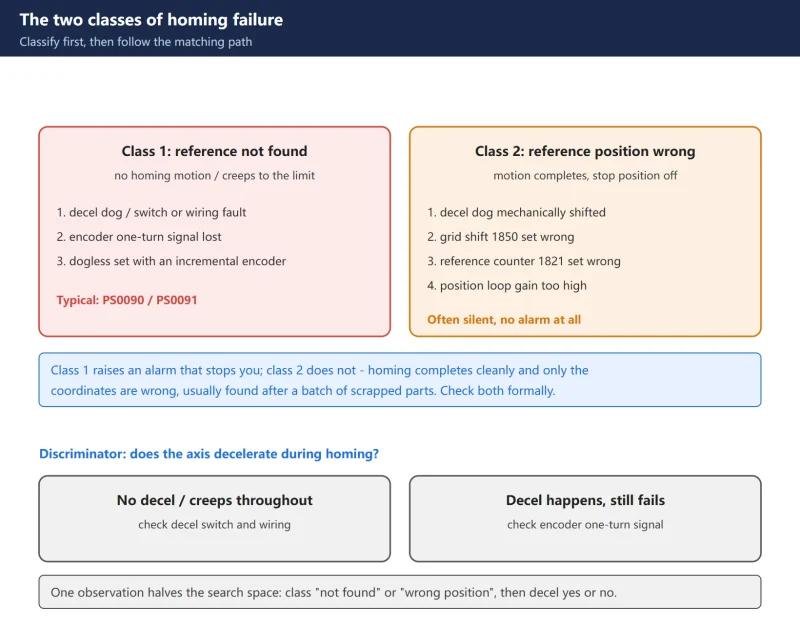
How to Classify and Troubleshoot CNC Homing Failures: Reference Not Found vs Wrong Reference Position + Decel Dog / One-Turn Signal + Grid Shift 1850 / Reference Counter 1821 + Absolute Encoder Battery
Stop swapping parts to see what sticks. Split homing failures into two classes: reference not found, and reference position wrong. In the first class, watch whether the axis decele...
19小时前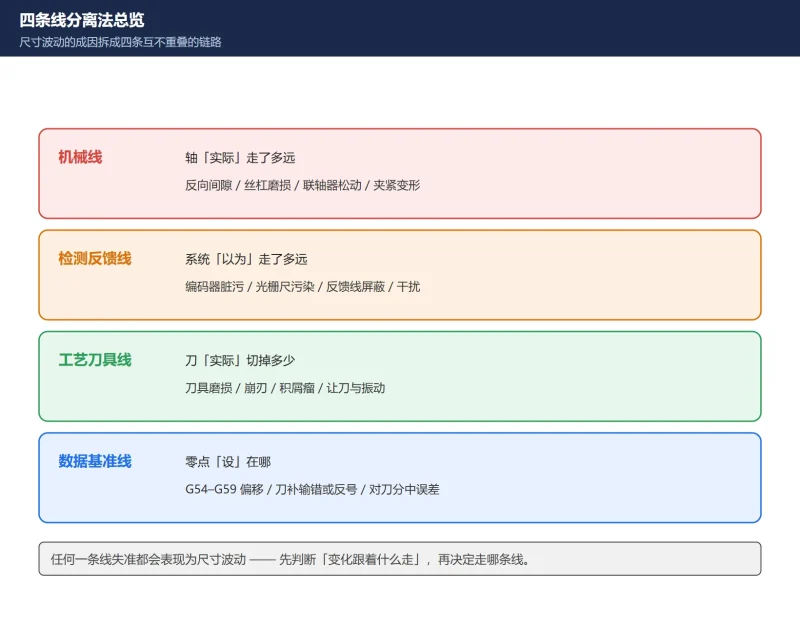
加工尺寸忽大忽小怎么查?四条线分离法:机械线 / 检测反馈线 / 工艺刀具线 / 数据基准线,一次把波动源分开
尺寸忽大忽小别再靠反复调刀补硬压 —— 刀补只修稳定的系统偏差,修不了随机漂移。用四条线分离法先判断「变化跟着什么走」:随件数走是刀具磨损,随时间走是热变形,随位置走是丝杠/螺距,随...
昨天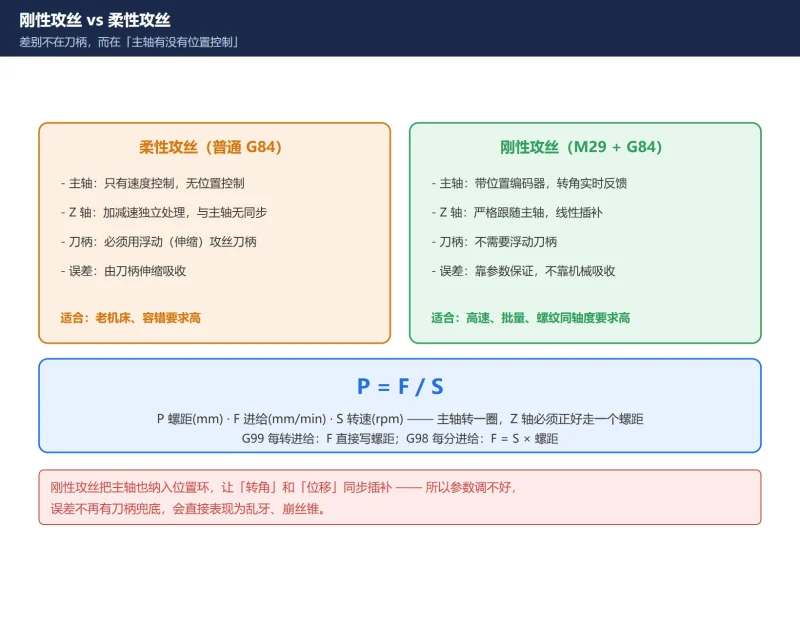
FANUC 刚性攻丝参数全解:M29/G84 同步原理 + 5200–5294 参数链 + SP0741 报警怎么排(附诊断号 452/453 读法)
刚性攻丝调不好的根子,多半不是编程而是参数。本文把 5200–5294 按五类拆开讲:开关位决定走不走刚性攻丝、齿轮比 5221–5224/5231–5234 决定比例、转速上限是 5241–5244(不是 5200)、增...
昨天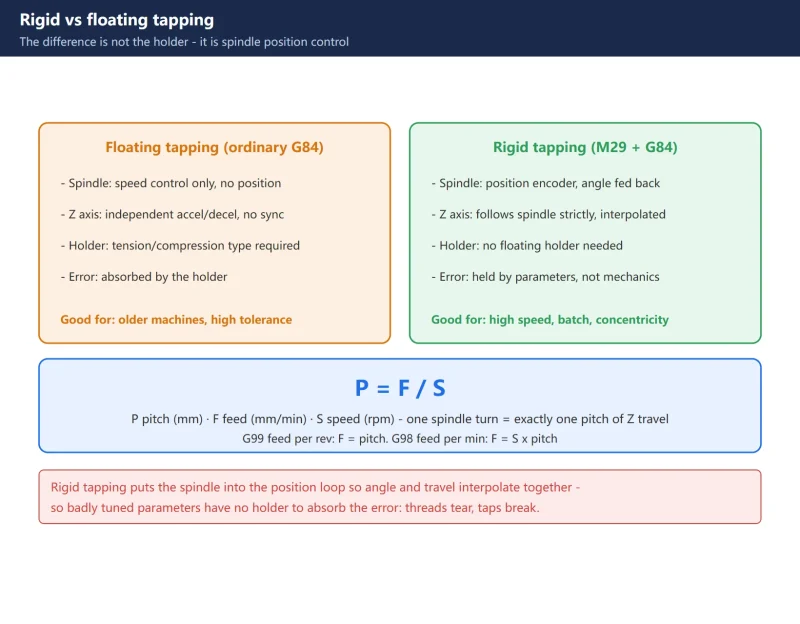
Fanuc Rigid Tapping Parameters Explained: M29/G84 Sync, the 5200–5294 Chain and SP0741 Alarm Troubleshooting (with DGN 452/453)
Bad rigid tapping is usually not the program - it is the parameters nobody explained. This guide splits the 5200-5294 group into five blocks: enable bits that decide whether you ta...
昨天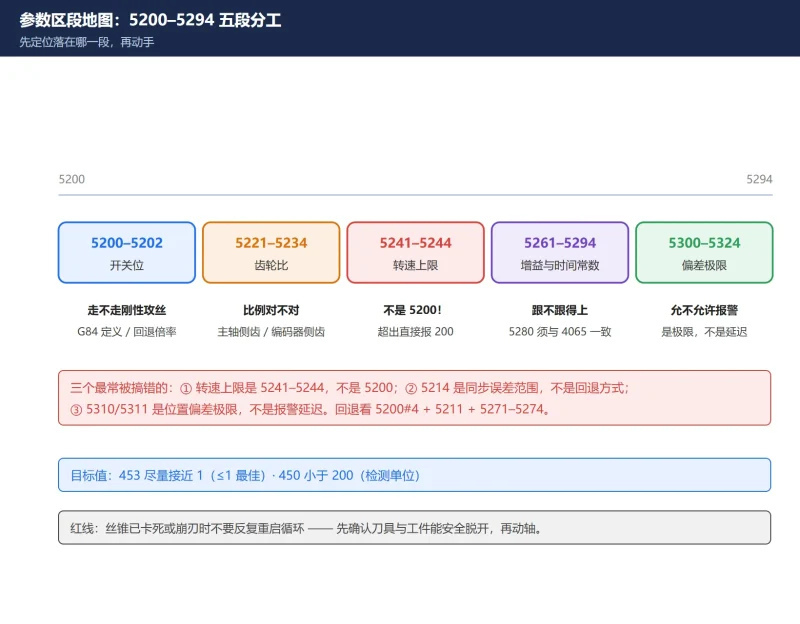
FANUC 刚性攻丝参数速查表:5200–5294 区段逐条说明 + SP0741 报警码 + 诊断号 452/453 含义
可直接对着机床抄的 FANUC 刚性攻丝参数速查表:5200–5294 按五段归类(开关位 / 齿轮比 / 转速上限 5241–5244 / 增益与时间常数 / 偏差极限),逐条给出含义与常用设定;附诊断号 452/453/45...
昨天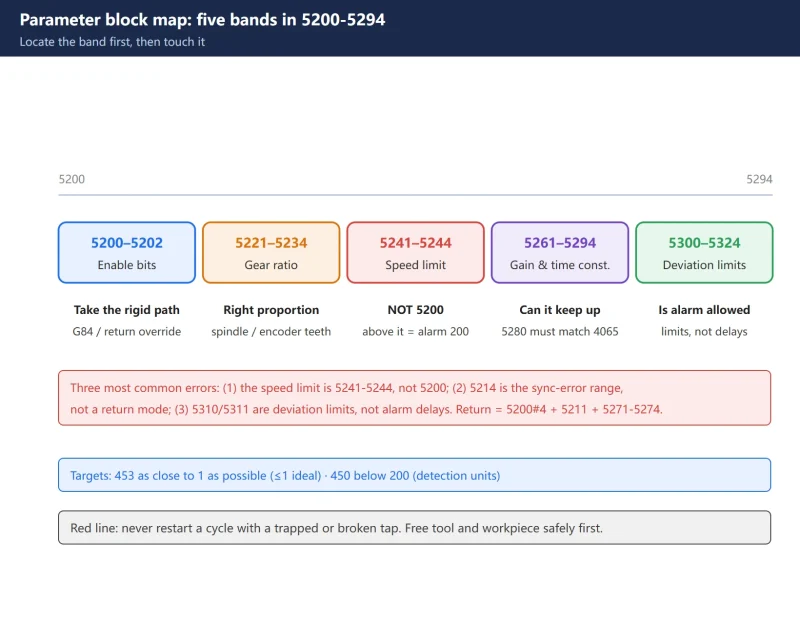
Fanuc Rigid Tapping Parameter Quick Reference: 5200–5294, SP0741 and DGN 452/453
A copy-straight-to-the-machine Fanuc rigid tapping reference: 5200-5294 grouped into five blocks (enable bits, gear ratio, speed limit 5241-5244, gains and time constants, deviatio...
昨天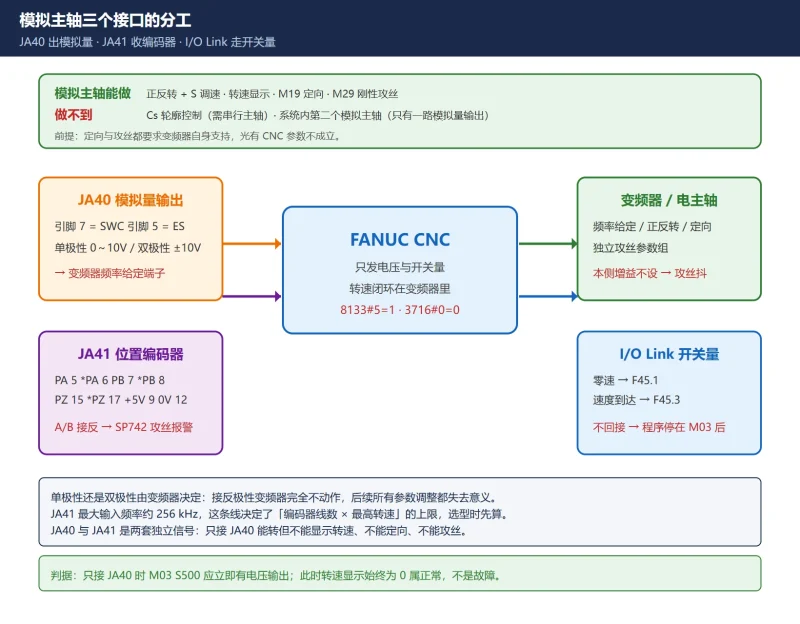
FANUC 模拟主轴调试全流程:8133#5/3716#0/3717 启用链 + 3730/3731 电压标定 + JA40/JA41 接线
模拟主轴的坑不在参数多,而在启用链顺序错、3730 与 3731 填反、JA41 编码器 A/B 接错。本文按接线→启用链→电压标定→功能验证四步走:给出 3717 填 0 时无报警却不转的原因、3731 先 3730 ...
19小时前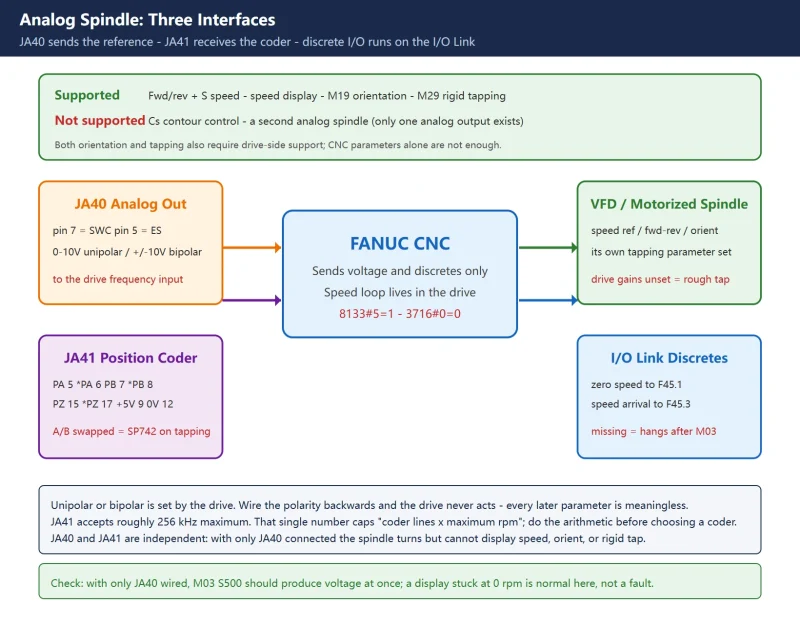
Fanuc Analog Spindle Commissioning: Enable Chain 8133#5/3716#0/3717, 3730/3731 Voltage Calibration, and JA40/JA41 Wiring
An analog spindle is rarely beaten by the number of parameters. It is beaten by a wrong enable order, 3730 and 3731 swapped, or an inverted coder phase on JA41. Four stages in orde...
19小时前




扫一扫,添加我的微信