最新发布第29页
排序
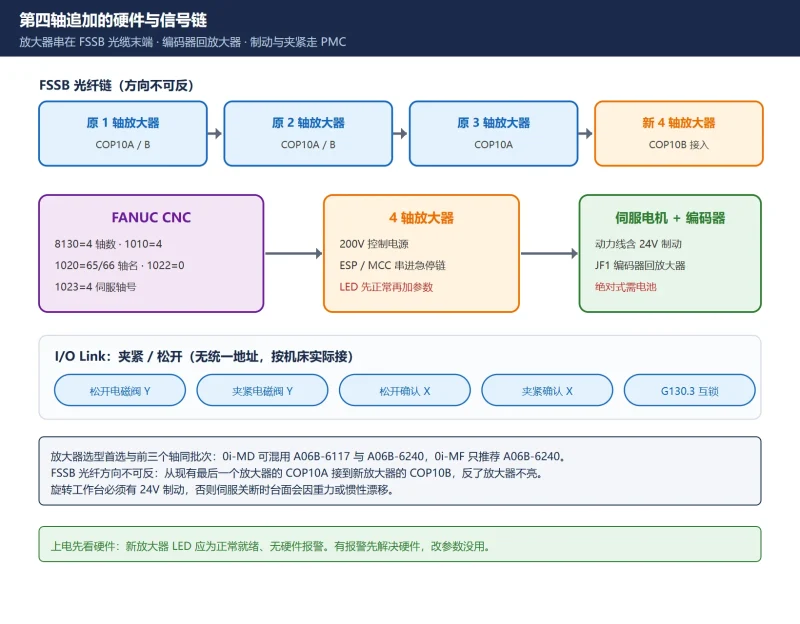
FANUC 第四轴/旋转轴追加配置:FSSB + 轴定义参数 + 伺服初始化 + 回零设定全流程
第四轴加不上的本质不是参数多,而是 FSSB 轴数没告诉系统、轴名 ASCII 填错、1006#0 忘了置 1、柔性齿轮比算错。本文按硬件→FSSB→轴定义→伺服初始化→回零→PMC 六步走:给出 8130/1010/102...

 19小时前
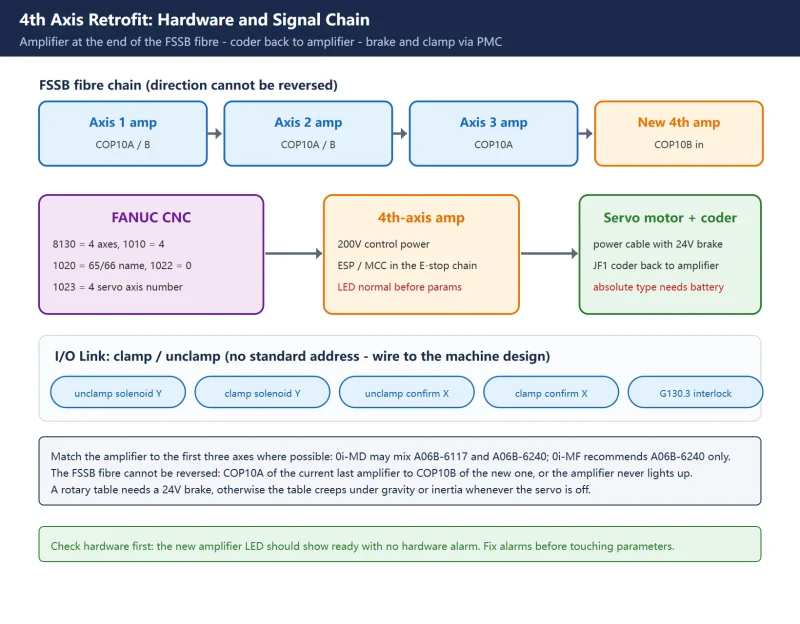
FANUC 4th Axis / Rotary Axis Add-on Config: FSSB, Axis Parameters, Servo Init, Homing
Adding a fourth axis is rarely about having too many parameters - it usually fails because the FSSB axis count was never told to the control, the axis name ASCII is wrong, 1006#0 w...
19小时前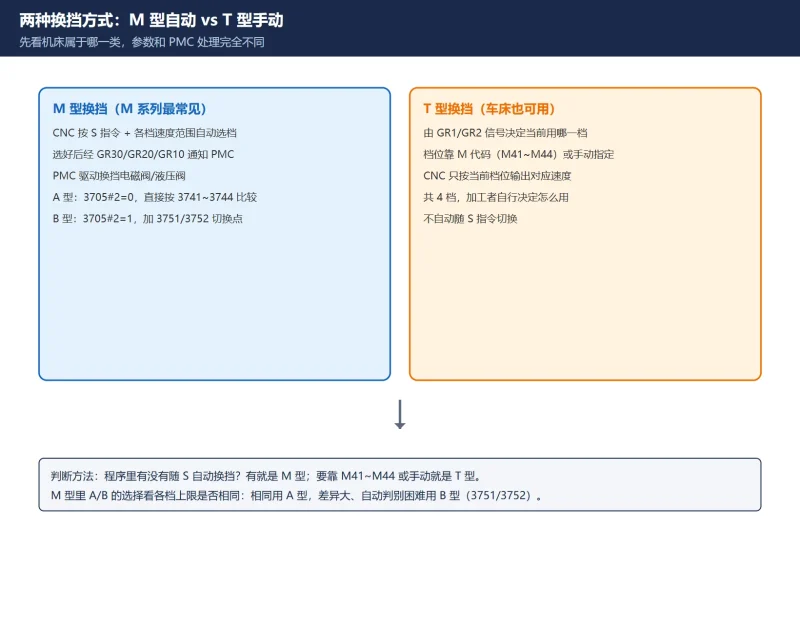
FANUC 主轴齿轮换挡参数全解:3705/3732/3735/3741-3744/3751-3753/4056-4059 + PMC 信号
主轴齿轮换挡(高低档)错得最多的是钳速参数名搞混(标准里没有 3734,最低钳速 3735、最高 3736)、3741-3744 与各档传动比算反、以及 PMC 侧 CTH1A/CTH2A 与 GR 信号没对应。本文按换挡方式...
19小时前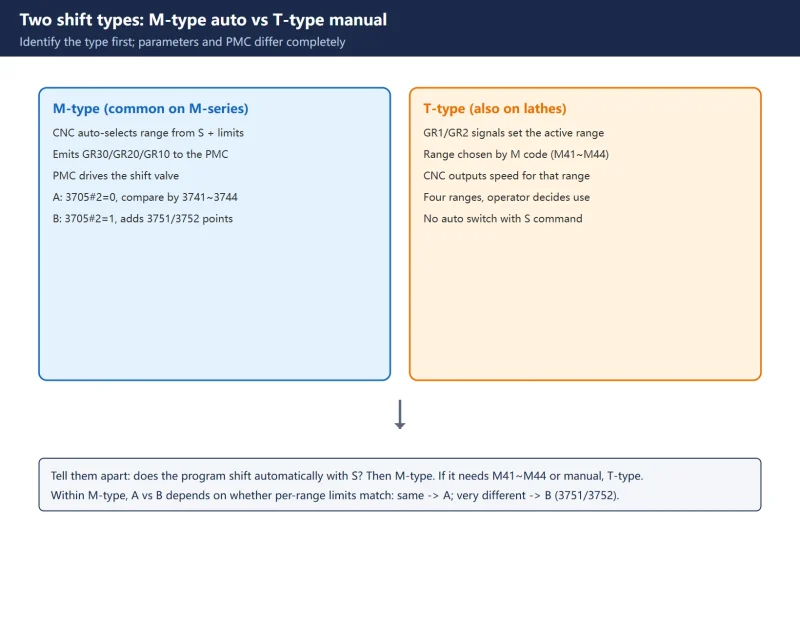
FANUC Spindle Gear Shifting: 3705/3732/3735/3741-3744/3751-3753/4056-4059 and PMC Signals
Gear-shift setup breaks most often because the clamp-speed parameter names are confused (there is no 3734; minimum is 3735, maximum 3736), 3741-3744 is inverted against the gear ra...
19小时前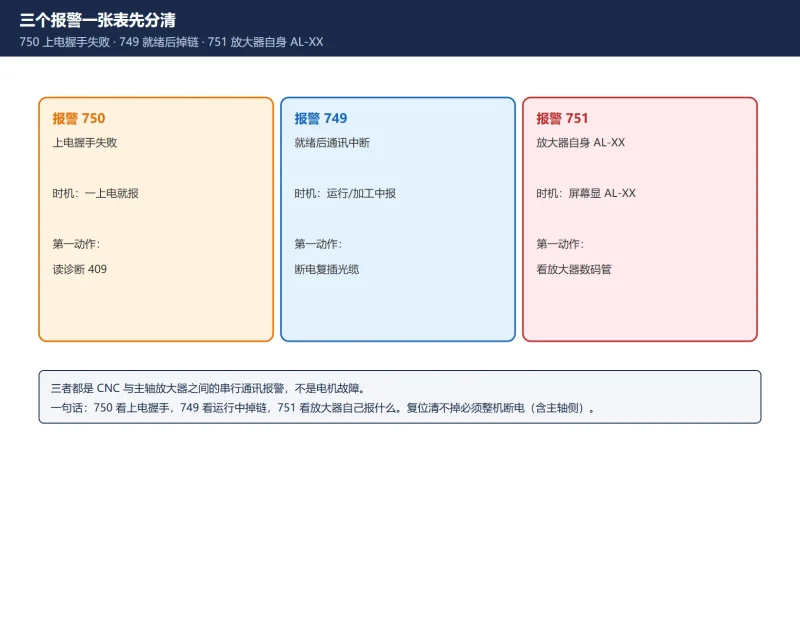
FANUC 串行主轴报警 749/750/751 排查:先分时机,再看诊断 409 与放大器数码管
749/750/751 都是 CNC 与主轴放大器之间的串行通讯报警,不是电机故障。750 是上电握手失败、749 是就绪后掉链、751 是放大器自身 AL-XX,三者排查起点完全不同。本文给时机区分、诊断 409 四位...
19小时前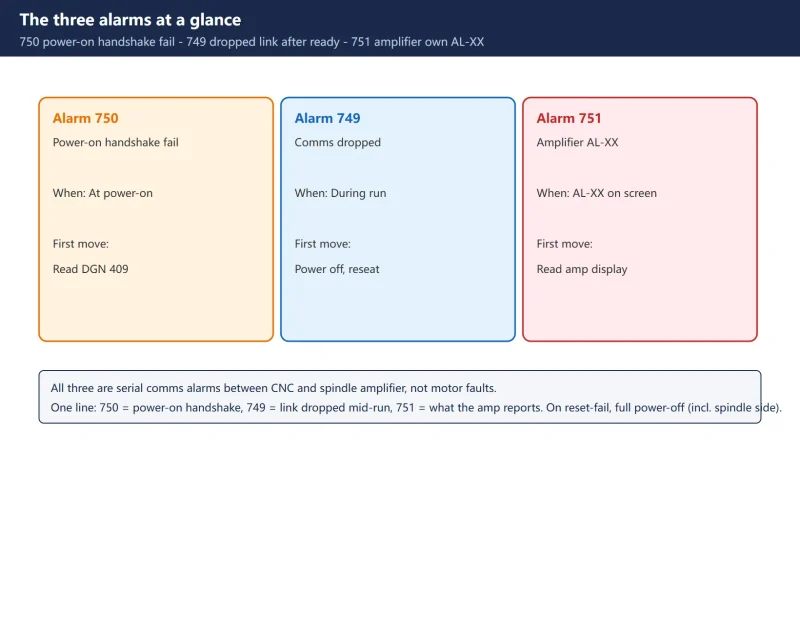
FANUC Serial Spindle Alarms 749/750/751: Split by Timing, then DGN 409 and Amp Display
749, 750 and 751 are all serial communication alarms between the CNC and the spindle amplifier - not motor faults. 750 is a failed power-on handshake, 749 a dropped link after read...
19小时前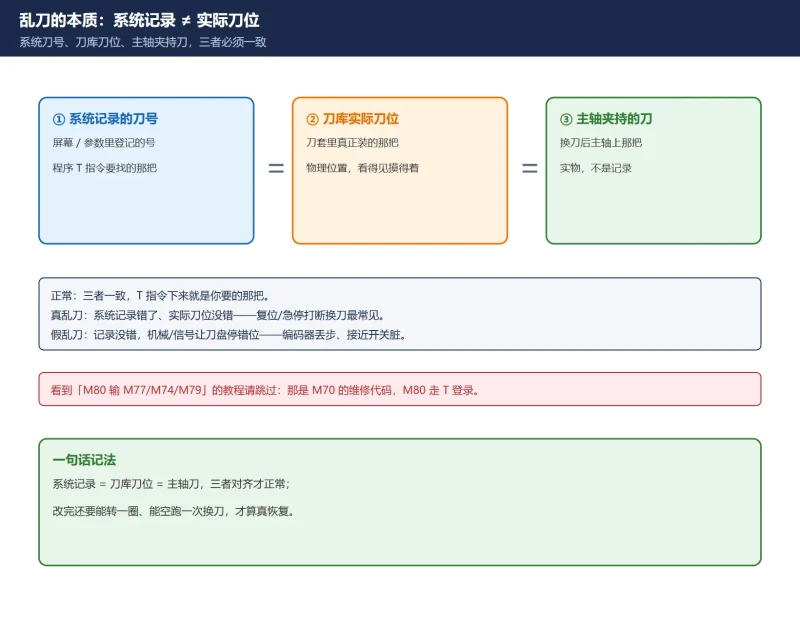
三菱 M80 刀库乱刀怎么修:先分真假,再用 T 登录逐位修正
三菱 M80 刀库乱刀的本质是系统记录的刀号与实际刀位对不上。不要照搬 M70 的 M77/M74/M79 维修代码,M80 的正确手段是 Setup 下的刀具登录逐位核对 + 主轴同步,再按信号/参数/机械三分法定位...
19小时前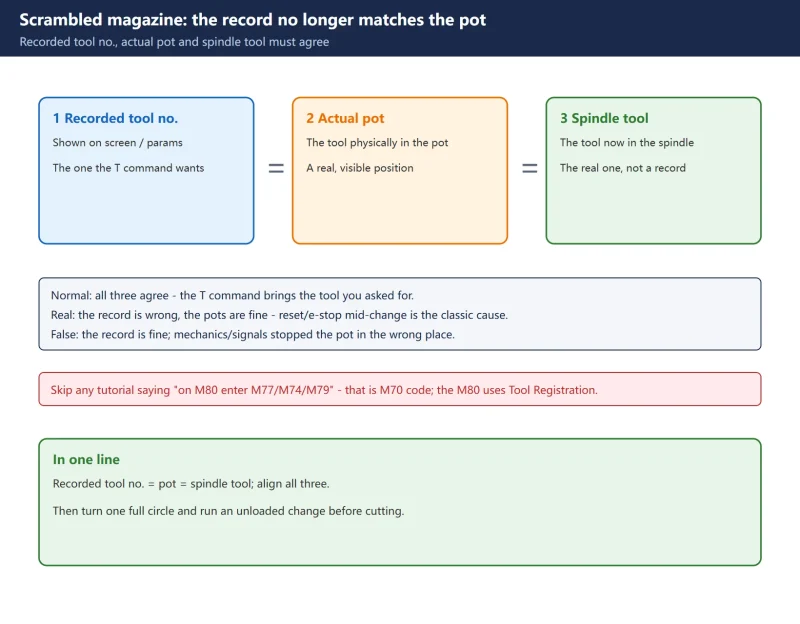
Mitsubishi M80 Tool Magazine Out-of-Order: Fix It with Tool Registration
A scrambled tool magazine on a Mitsubishi M80 is not 'a tool loaded wrong': the recorded tool number no longer matches the physical pot. Do not copy the M70 M77/M74/M79 codes - the...
19小时前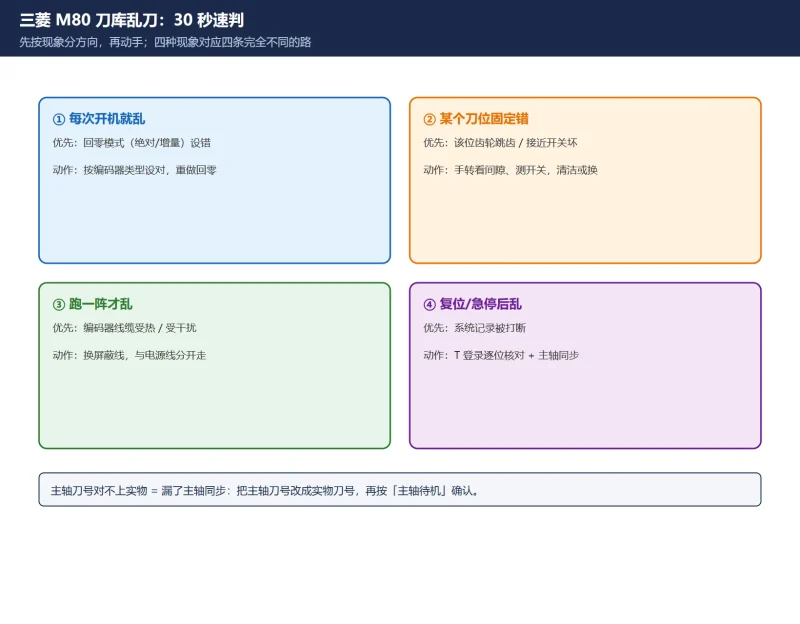
三菱 M80 刀库乱刀速查表:现象·原因·先查 + T 登录四个位置 + R 寄存器
一页看完三菱 M80 刀库乱刀:按现象对号入座,主轴同步、T 登录四个位置、刀库刀具数据与刀具寿命的 R 寄存器地址一次列清。适合现场贴着机台用。
19小时前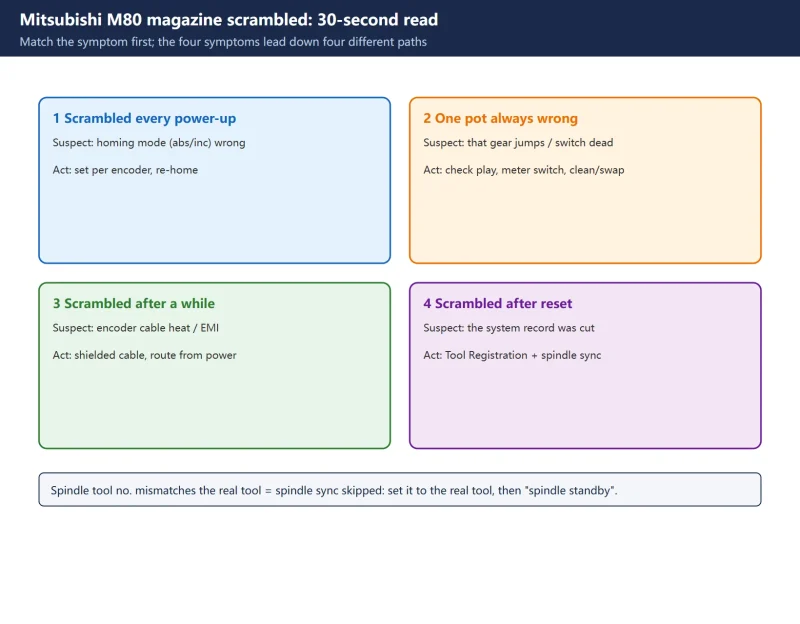
Mitsubishi M80 Magazine Scrambled Quick Chart: Symptom, Tool Registration Fields and R Registers
One page for a scrambled Mitsubishi M80 magazine: match the symptom, then act. Spindle sync, the four Tool Registration targets, and the magazine / tool-life R-register addresses a...
19小时前




扫一扫,添加我的微信