最新发布第28页
排序
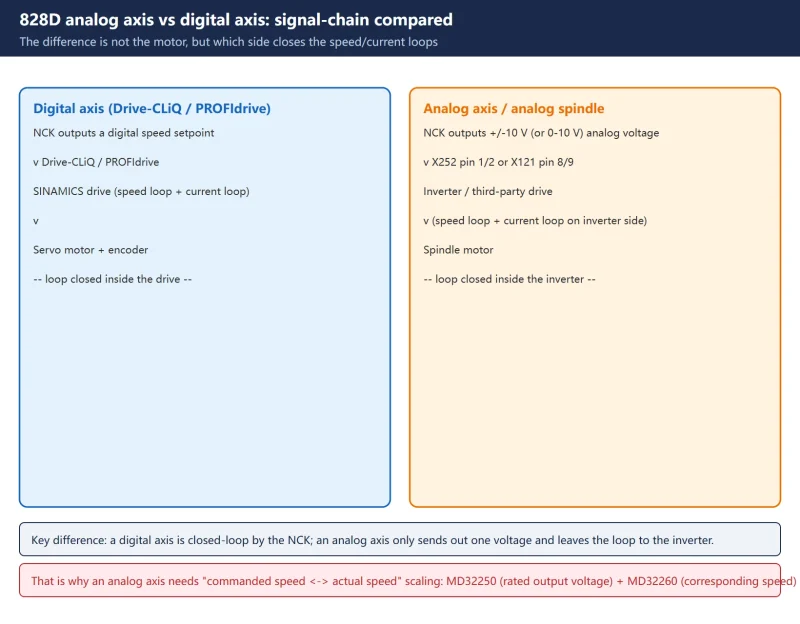
How to Configure an Analog Spindle / Analog Axis on SINUMERIK 828D: MD30100–31050, X252 Wiring, MD32250/32260 Scaling
When an 828D drives an inverter or analog drive, the axis must be configured as an analog (analog setpoint output) axis rather than a digital one. This guide gives the values for M...

 20小时前
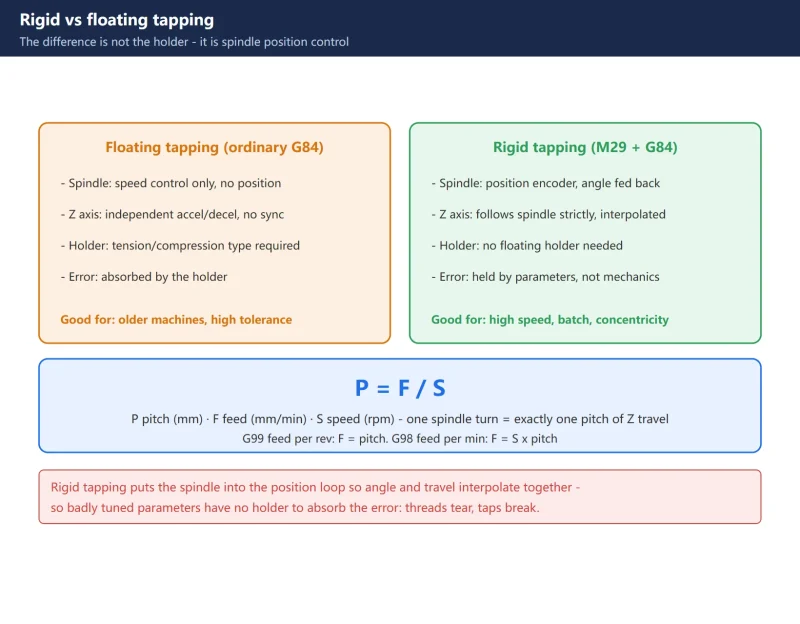
Fanuc Rigid Tapping Parameters Explained: M29/G84 Sync, the 5200–5294 Chain and SP0741 Alarm Troubleshooting (with DGN 452/453)
Bad rigid tapping is usually not the program - it is the parameters nobody explained. This guide splits the 5200-5294 group into five blocks: enable bits that decide whether you ta...
20小时前
技术人的“躺赚”系统:零基础复制粘贴也能月入过万
懂技术却赚不到钱?专为不擅长人际沟通的技术人员打造的零基础“复制粘贴”赚钱系统。本文深度拆解如何利用AI工具、视频下载软件及剪映,通过搬运爆款素材、自动化内容生产实现被动收益。从软件...
昨天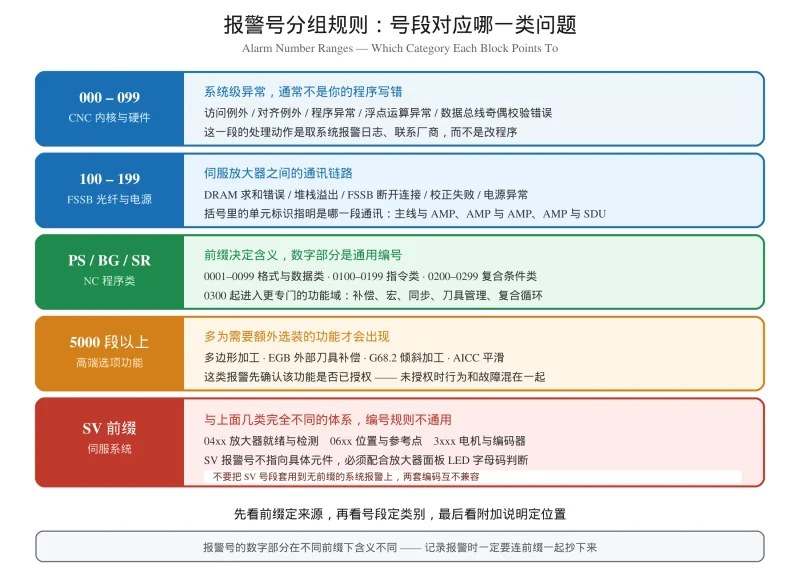
FANUC 报警代码一览表:分组速查与首选检查动作
FANUC 报警代码速查:讲清无前缀系统报警、PS BG SR 程序报警、SV 伺服报警与 PMC 自定义报警四套体系,附常用程序报警三列对照表与复位前必做的三件事。
昨天
FANUC Alarm Code List: P/S Alarms 5130–5559 Explained (Part 6)
English reference for FANUC P/S alarm numbers 5130 to 5559: PMC axis overlap, flexible synchronous control, tool management and interference, Cs contour control, tilted surface mac...
昨天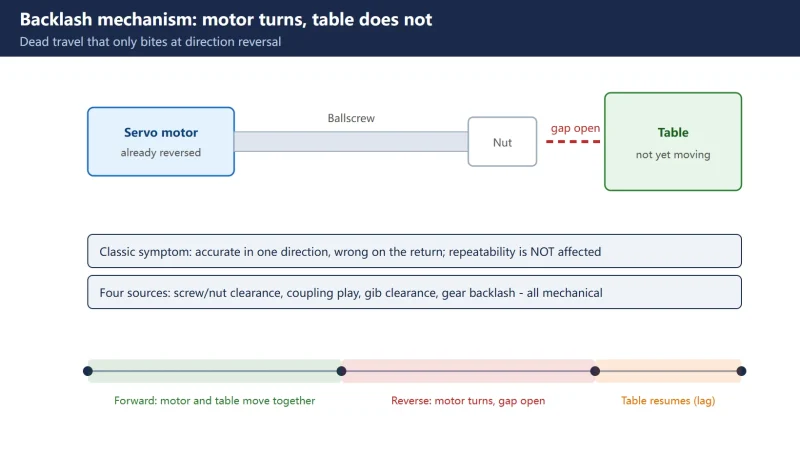
Fanuc Backlash Compensation 1851: Measure, Convert to Detection Units, Write and Verify
The complete FANUC backlash compensation procedure: measure with a dial indicator at cutting feed and rapid, convert to detection units (0.020 mm becomes 20; lathe X axis times 2),...
昨天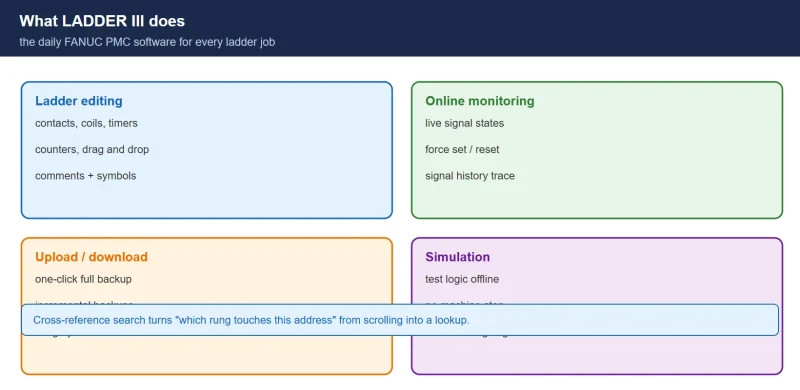
FANUC LADDER III: Version Selection, Installation and Common Pitfalls
A practical guide to FANUC LADDER III: which version matches which control, how to install it without the classic beginner failures, and how to get connected for online PMC monitor...
昨天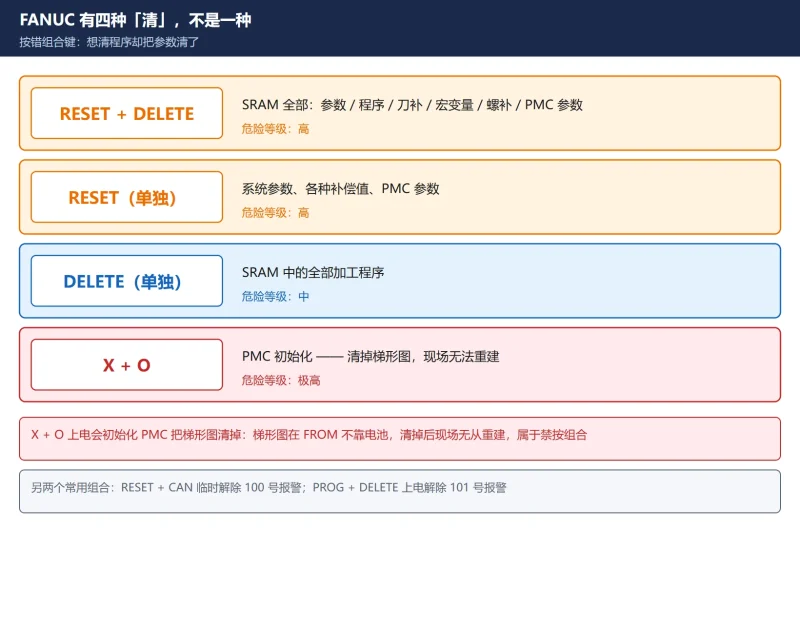
FANUC 参数怎么全部清零?RESET + DELETE 上电全清 + IPL 菜单逐项实操(顺带纠正一个流传很广的错误)
网上流传的「FANUC 恢复出厂设置」教程至少有一半是错的:0i-MD / 0i-MF 根本没有这个菜单项,真正的入口是断电后按住 RESET + DELETE 上电。本文区分四种「清」(RESET+DELETE / RESET / DELET...
昨天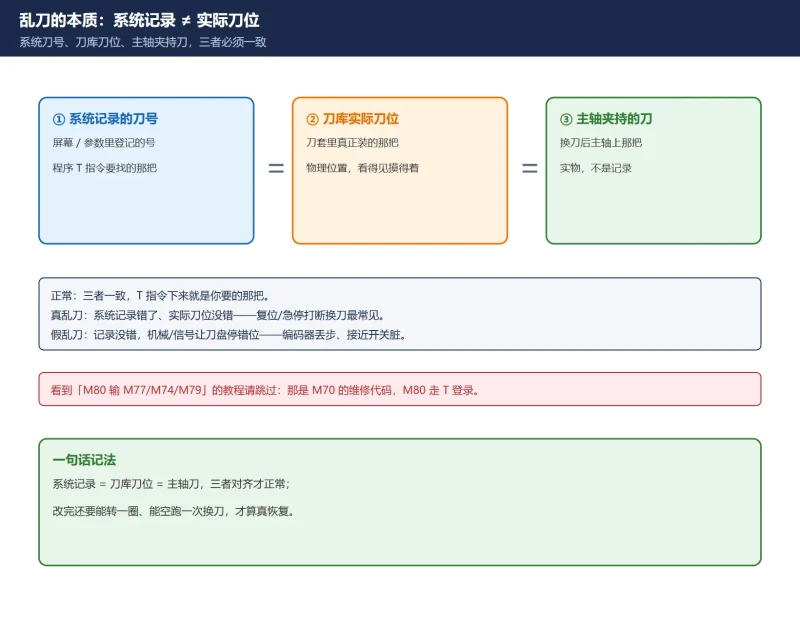
三菱 M80 刀库乱刀怎么修:先分真假,再用 T 登录逐位修正
三菱 M80 刀库乱刀的本质是系统记录的刀号与实际刀位对不上。不要照搬 M70 的 M77/M74/M79 维修代码,M80 的正确手段是 Setup 下的刀具登录逐位核对 + 主轴同步,再按信号/参数/机械三分法定位...
11小时前




扫一扫,添加我的微信