最新发布第28页
排序
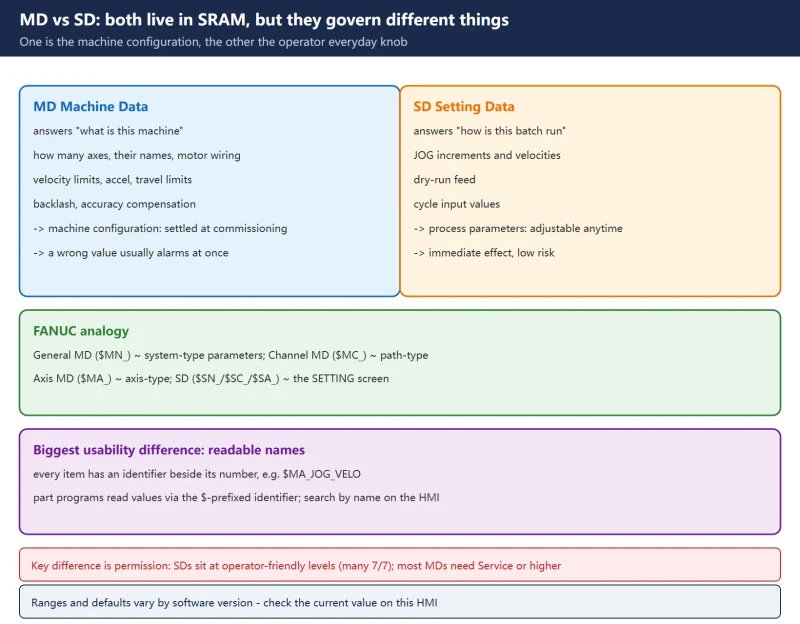
Setting Data (SD) vs Machine Data (MD) on SINUMERIK 828D: Number Ranges, Activation Types and Access Levels
On the 828D both MD and SD live in SRAM but do completely different jobs: MD defines what this machine physically is, and getting it wrong means alarms or even a crash; SD is the o...

 18小时前
伺服放大器坏了修还是换?一张决策表和四个成本项,别只看报价单
伺服放大器故障后只对比维修费和换新价是错的。本文给出可修性判断、维修三个层次、更换三种选择,以及含停机成本的完整决策表,帮你算出真正的成本边界。
昨天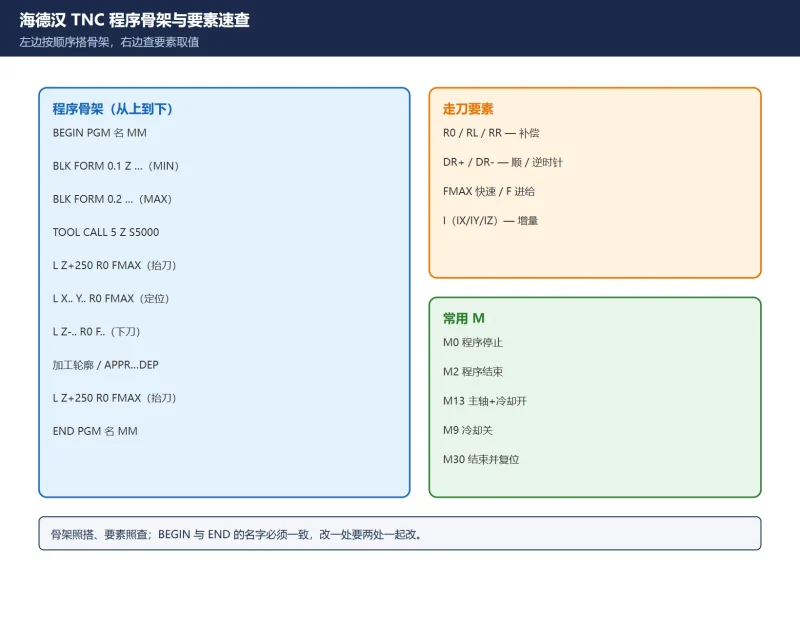
海德汉 TNC 基本程序段速查表:BEGIN/BLK FORM/TOOL CALL/L/C/CR/APPR/CYCL DEF 一页对照
把海德汉 TNC 最常用的对话式程序段压成一页:程序结构 8 步、常用段全表、走刀要素(R0/RL/RR、DR、I)、常用 M 代码。现场写程序或读别人程序时对着查。
18小时前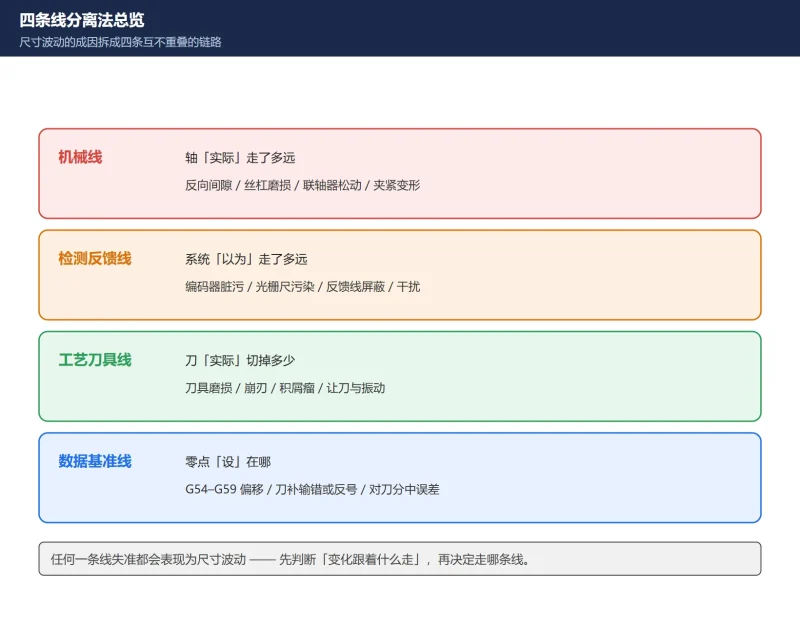
加工尺寸忽大忽小怎么查?四条线分离法:机械线 / 检测反馈线 / 工艺刀具线 / 数据基准线,一次把波动源分开
尺寸忽大忽小别再靠反复调刀补硬压 —— 刀补只修稳定的系统偏差,修不了随机漂移。用四条线分离法先判断「变化跟着什么走」:随件数走是刀具磨损,随时间走是热变形,随位置走是丝杠/螺距,随...
昨天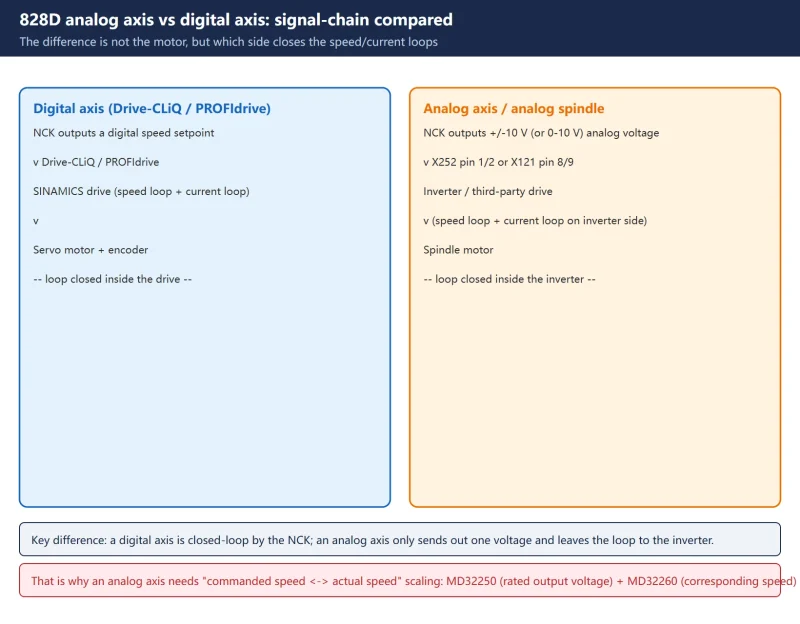
How to Configure an Analog Spindle / Analog Axis on SINUMERIK 828D: MD30100–31050, X252 Wiring, MD32250/32260 Scaling
When an 828D drives an inverter or analog drive, the axis must be configured as an analog (analog setpoint output) axis rather than a digital one. This guide gives the values for M...
昨天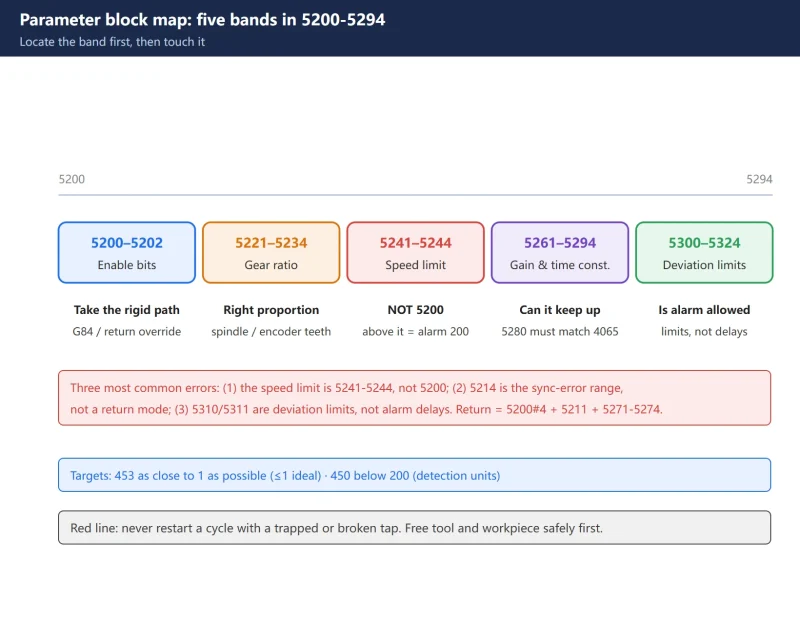
Fanuc Rigid Tapping Parameter Quick Reference: 5200–5294, SP0741 and DGN 452/453
A copy-straight-to-the-machine Fanuc rigid tapping reference: 5200-5294 grouped into five blocks (enable bits, gear ratio, speed limit 5241-5244, gains and time constants, deviatio...
昨天
Used CNC Machine Electrical Inspection Checklist — 30 Checks Before You Pay the Balance
The most expensive mistake in a used CNC purchase is in the electrical cabinet. This 30-point field checklist covers history verification, power-off checks, live testing, and how t...
昨天
CNC Servo Vibration, Overshoot and Noise: A Phenomenon-Based Troubleshooting Table
Classify servo vibration into 4 types (high-frequency squeal, low-frequency flutter, start/stop overshoot, machining ripple) and follow the right branch. Covers HRV filters, inerti...
昨天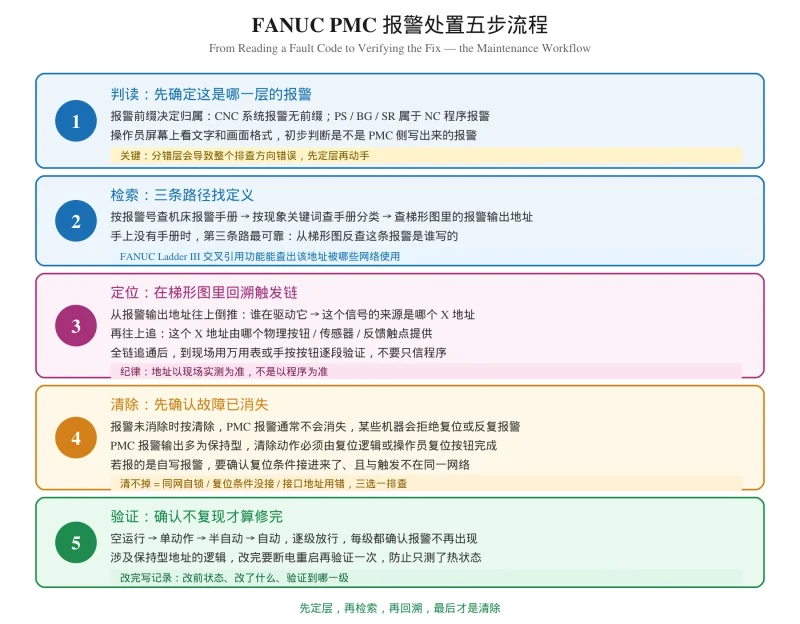
Fanuc PMC Alarm Codes Explained: How to Read, Search and Clear a PMC Fault
How to read, search and clear Fanuc PMC alarm codes without losing your ladder.
昨天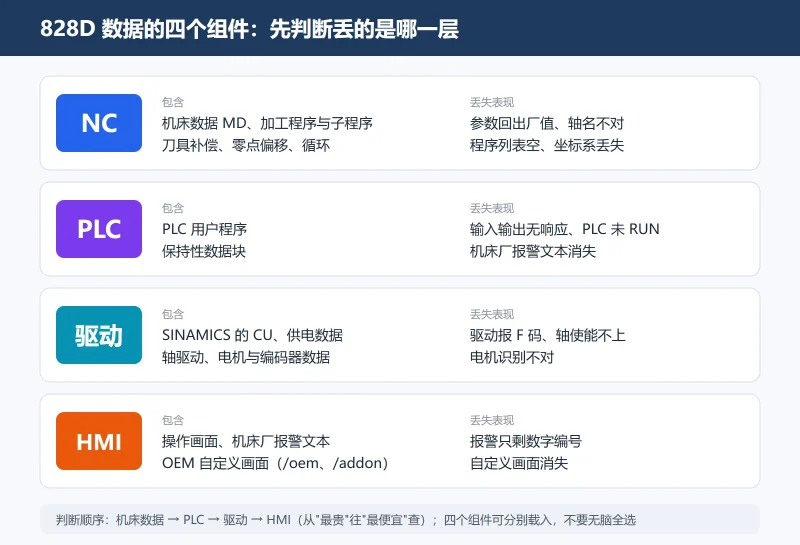
SINUMERIK 828D/802D 数据丢了还能救吗?程序/参数/PLC 三层恢复顺序与缺省模式启动操作详解
828D/802D 数据丢了怎么救:先判断丢的是 NC/PLC/驱动/HMI 哪一层,读懂 4062 与 4060 相反的含义,再按内部备份、.ard 存档、缺省模式启动三条路径恢复。含 SUNRISE 口令与轴名错位提醒。
昨天




扫一扫,添加我的微信