


一句话答案:"It powers on and runs" only proves a used CNC is not dead, not that it works—latent faults in the servo, spindle, tool changer, lubrication or safety circuits turn into repair bills after you pay. This guide splits a field inspection into 5 stages and 30 checks, with the common concealment tactics sellers use and how to turn findings into price.
The most expensive sentence in a used equipment deal is: “It powers on and it runs, so it’s fine.”
Powering on only proves it isn’t dead. It does not prove it will work. Especially on the electrical side — servo drives, spindle, tool changer, lubrication, safety circuits. Any one of them carrying a latent fault turns into a repair invoice plus months of downtime once it reaches your floor.
This guide breaks a field inspection into 5 stages and 30 checks. Print it out and tick them off one by one.
Note: this article covers inspection method and decision logic only, not machine-specific parameters. Wherever a specific value is needed, refer to the manual that came with the machine. Items marked verify against the manual should not be settled from experience alone.
1. Check the history before you check the machine (5 checks)
A machine can be cosmetically restored. Its history cannot be faked.
1. Nameplate, system model and drive nameplate must agree
Compare the nameplate model and serial number with what the control reports. Check three places in particular: the nameplate, the machine model setting inside the parameters, and the drive nameplate. If they disagree, the control or the drives have been swapped.
2. Read running time and part count
Most controls can report cumulative powered hours, cumulative parts cut, and spindle hours. “Old machine, very few running hours” is either genuinely idle time or a cleared counter.
3. Go through the alarm history
Look at the alarm log for historical alarms. What you want: repeated occurrences of the same alarm, servo overload, spindle alarms, battery alarms.
Alarm logs can be cleared. This item is evidence, never a conclusion.
4. Look for evidence the parameters were touched
Check parameter backup dates and modification traces. If the timestamp is obviously later than the machine’s last known operating period, someone has been in there recently — which may be maintenance, or may be concealment.
5. Ask why it is being sold
Stopped because of a fault, product line change, or equipment renewal — those are normal reasons. A vague “the owner got out of the business” deserves extra caution.
2. Checks with the power OFF (8 checks)
Do not switch it on yet. What you can see with the power off becomes invisible once it is running.
6. Open the electrical cabinet — smell it first
A burnt or acrid smell is a hard signal. Then look at: dust thickness, oil contamination, scorch marks, water traces, and whether the cabinet seal has hardened.
7. Cables and harnesses
Inspect each one: hardened or cracked insulation, damaged sheath, rodent damage, loose cable ties, and chafed wires inside the drag chains. The drag-chain sections are the worst offenders — wires break at bends.
8. Contactors and relays
Look for pitted, eroded, or welded contacts. Pull the armature by hand: the action should be crisp, never sluggish.
9. Drive cooling fans and filters
A dead fan is the most common latent fault. Fan stops → drive overheats → intermittent alarms, which are almost impossible to reproduce on site but will follow you home.
10. Absolute position encoder battery
The battery holder sits in the cabinet or on the motor side, depending on the machine. Measure the voltage; treat anything below its rated value as “replace” (verify the rated value against the manual).
The classic consequence of a low battery: absolute position is lost on every power-down, requiring re-homing or reference-point re-establishment on the next start-up. This is not a minor fault.
11. Grounding and insulation
Check that the ground wire is actually landed on the cabinet and has not been removed. With a megger, measure insulation resistance — use the acceptance value from the manual, not “looks about right”.
12. Look for swapped components or modifications
Empty slots, jumpered wires, unrecognised retrofit boards. A jumper is the classic “make the alarm go away” shortcut.
13. Transformers and power modules
Look for discoloration from heat and smell. Measure module output voltages after power-up.
3. Power on, but do not run it (6 checks)
Energise, but don’t move anything yet. This stage tells you what the machine thinks about its own health.
14. Power-up self-test and current alarms
Do not hit reset first. Record every alarm number and message, then decide which are “sat for a long time” and which are real.
15. Battery alarms
If absolute-position or battery alarms appear, the battery or the stored position is suspect. Do not clear them on site — ask whether the reference point has already been lost.
16. Servo and spindle enable
Release the E-stop and check whether the servos energise, whether there is abnormal noise, and whether the drive panel shows alarms. Noise at the moment of energising deserves particular attention.
17. E-stop circuit and guard interlocks
Test each one: panel E-stop, pendant E-stop (if fitted), guard door switch, light curtain (if fitted). A bypassed E-stop circuit is the most dangerous and the most common corner cut.
18. Lubrication, hydraulics, pneumatics
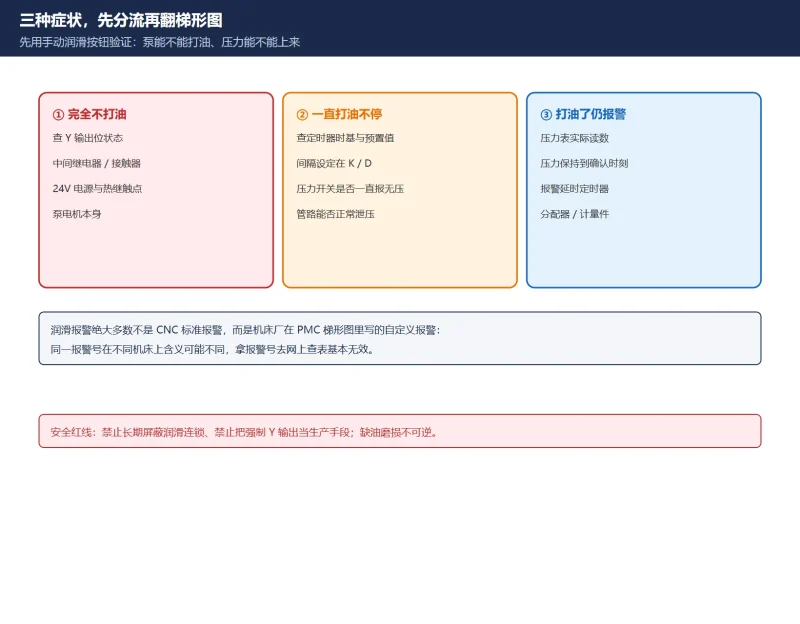
Check oil level, pressure and air pressure, and confirm the lubrication pump actually delivers on schedule (observe it in manual mode). Poor lubrication is the slow killer of ways and ballscrews — invisible in a short visit.
19. Coolant and chip conveyor
Run the coolant pump and the chip conveyor under power. These auxiliaries do not affect “it runs”, but they absolutely affect whether you can start production.
4. What only shows up when it moves (7 checks)
20. Jog each axis through its full safe travel
Listen for noise, watch for smooth running. Look specifically for: abnormal noise, stiction, juddering, and backlash.
21. Backlash
Do a reversal test using a limit switch or a dial indicator. Excess backlash is not necessarily mechanical wear — it may be a parameter temporarily adjusted (see section 6).
22. Spindle ramp-up and orientation
Step up from low to medium speed, listening for noise and feeling for vibration. Test spindle orientation (required before tool change). The location of the noise matters — bearing noise, belt noise and motor noise must be distinguished.
23. Tool changer full cycle
Do not just watch one tool change. Run 10 or more consecutive changes and look for jammed tools, dropped tools, and positioning error. The tool magazine is one of the most common problem areas on a used machine.
24. Coolant, chip conveyor and pneumatic interlocks
Run a short program in automatic mode and confirm the auxiliaries follow correctly.
25. Accuracy spot-check
A ballbar or laser interferometer is ideal; without them, at minimum cut a test part (circle, square, step) and check roundness, squareness and size consistency.
26. Run it long
Idle for at least 30 minutes. Many overheat and intermittent-alarm faults only appear under continuous running. Do not skip this stage.
5. Software and files (4 checks) — the most overlooked
27. Is the parameter backup complete?
Confirm you can export parameters, PMC ladder, pitch error compensation, macro programs and tool data. Miss one and every future problem gets harder.
28. Can the backup actually be restored? (critical)
Having a backup file is not enough — you must confirm this backup is restorable. A corrupt file, a version mismatch, or a missing PMC means there is no rescue when you need one.
Run this as a rehearsal. Half an hour before purchase beats three days of downtime later.
29. System media, CF card, and locks
Confirm the system program media is intact, whether it is encrypted, and whether a factory password lock is present. A locked machine with an unknown password is a half-usable machine.
30. Documentation
The random manual, electrical drawings, parameter tables and PLC program listing. Electrical drawings matter most — without them, every future line fault takes twice as long to trace.
6. Common concealment tactics (the most valuable section)
| Tactic | What it looks like | How to defeat it |
|---|---|---|
| Clearing the alarm log | An implausibly clean history for the machine's age | Cross-check against running hours and test-cut results |
| Temporarily adjusting parameters to hide backlash | Backlash “just barely passes” | Check parameter modification timestamps; measure at several positions |
| Removing or bypassing alarm devices | A sensor “isn't there” or its wire is jumpered | Count components against the electrical drawings (checks 12 and 17) |
| Board swapping or borrowing power | Drive or power module looks “new” | Match drive nameplate against the factory serial number |
| Removing filters or fans | An oddly clean cabinet that still runs hot | Touch-test every fan by hand (check 9) |
| Running empty but refusing a test cut | Deflection with “no material available” | Insist on a test cut, even a small part |
7. Turning findings into price
Finding problems does not mean you cannot buy the machine. It means turning them into price or remediation terms.
- List the findings first: which are “must fix before production”, which are “can run with”.
- Cost them: convert the must-fix items into money, including lost production time, and use that as your negotiating basis.
- Put it in writing: remediation scope, delivery condition, balance payment terms, warranty coverage.
- Hold back a balance: leave part of the payment until the machine has been powered, test-cut and accepted at your site.
Frequently Asked Questions
Q: What if there are no electrical drawings?
A: You can still buy it, but price the risk in. Without drawings, any future circuit fault can take twice as long to trace. At minimum require a parameter backup and the PLC program.
Q: Can I just clear a battery alarm?
A: Not recommended. When an absolute position encoder battery is low, clearing the alarm only hides the problem — the position is still lost on the next power-down. The correct fix is to replace the battery and re-establish the reference point.
Q: Can I sign off if it only ran empty, with no test cut?
A: Very risky. Empty running cannot expose load, accuracy or thermal deformation. At minimum require a small test part and keep the sample.
Q: How important is a parameter backup on a used machine?
A: Extremely. Parameters, PMC, pitch compensation and macro programs are all required, and you must verify that the backup is restorable. That is your only way back when something goes wrong.
Further reading
- FANUC Battery Alarm 306/307: Field Replacement Procedure
- FANUC Diagnosis Numbers (DGN) Quick Reference
- FANUC No-Alarm Fault Diagnosis: Using DGN Numbers
- CNC Servo Vibration, Overshoot and Noise: Phenomenon-Based Troubleshooting
- FANUC 0i-Mate / 0i-D Alarm Quick Reference
Verify against the manual: the rated battery voltage (check 10), insulation acceptance criteria (check 11), allowable backlash (check 21) and accuracy tolerances (check 25).
No specific values are given here because they vary widely by machine model and accuracy class — applying someone else’s numbers is the real mistake.
Where to go next
- FANUC Troubleshooting — the full guide library: alarms, diagnosis numbers, servo, spindle, PMC and electrical faults, organised by symptom.
- CNC Repair Tools — which instrument measures what: multimeters, clamp meters, insulation testers and oscilloscopes, with the specification that actually matters.
- Remote Technical Support — have the readings reviewed with you: alarm reverse lookup, PMC ladder analysis and servo tuning advice by call. Repair companies and integrators welcome.
Read the guide, get the right instrument, or walk the diagnosis through with someone — pick whichever you need.
The original Chinese version — same procedure, with the full field notes.






























暂无评论内容